

What is a Mobile Powder Pneumatic Conveying System? What are the Design Principles?
Welcome to the world of efficient material handling solutions, where the mobile powder pneumatic conveying system stands out as a versatile and reliable choice for transporting bulk powders. This article delves into the essence of such systems, exploring their design principles and the technology behind them. As a leading provider in the industry, Shandong HeadPowder Engineering Co., Ltd. specializes in crafting innovative solutions tailored to meet diverse operational needs.
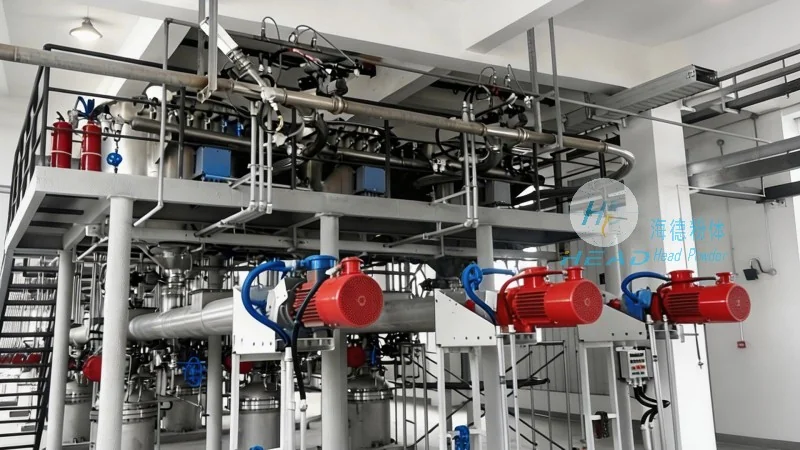
Understanding the Mobile Powder Pneumatic Conveying System
A mobile powder pneumatic conveying system is a sophisticated setup designed to transport dry bulk materials, such as powders and granules, from one location to another using compressed air or other gas as the driving force. Unlike fixed systems, these systems are portable and can be easily reconfigured to adapt to changing production requirements. The core components include a hopper for material storage, a conveying line, a compressor to generate the necessary air pressure, and a control unit to regulate the entire process. This flexibility makes them ideal for industries like pharmaceuticals, food processing, and chemical manufacturing, where precise and hygienic material handling is paramount.
Key Components of the System
The effectiveness of a mobile powder pneumatic conveying system hinges on its well-designed components. Each part plays a crucial role in ensuring smooth and efficient operation. The material hopper serves as the initial storage point, allowing for easy loading of the powder. The conveying line, typically made of stainless steel or other corrosion-resistant materials, transports the material under pressure. The compressor generates the air pressure required to move the powder, while the control unit monitors and adjusts the system parameters to maintain optimal performance. Additionally, features like filter systems and dust collection units are often integrated to ensure environmental compliance and operational safety.
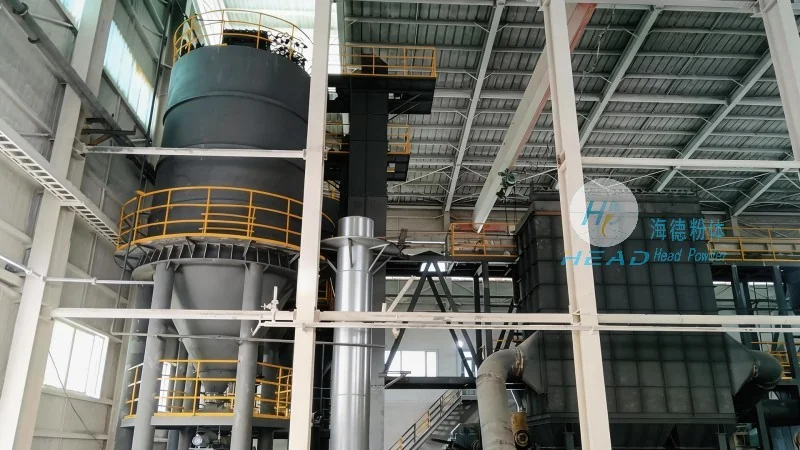
Design Principles Behind the System
The design principles of a mobile powder pneumatic conveying system are centered on efficiency, reliability, and adaptability. Engineers at Shandong HeadPowder Engineering Co., Ltd. focus on optimizing the system's flow characteristics, ensuring that the powder moves with minimal pressure drop and maximum throughput. The selection of appropriate air velocities and pipe diameters is critical to prevent material degradation and system blockages. Moreover, the system's modular design allows for easy installation and maintenance, reducing downtime and operational costs. The integration of advanced control technologies, such as variable frequency drives and real-time monitoring, further enhances the system's performance and longevity.
Advantages of Mobile Pneumatic Conveying Systems
Compared to traditional bulk material handling methods, mobile powder pneumatic conveying systems offer several advantages. Their portability allows for quick repositioning, enabling manufacturers to adapt to changing production layouts or temporary needs. The system's ability to handle a wide range of materials, from fine powders to coarse granules, makes it a versatile solution. Additionally, the enclosed design minimizes dust emissions, enhancing workplace safety and environmental compliance. The reduced need for extensive infrastructure, such as fixed pipelines and large storage silos, also contributes to lower capital and operational expenses. These benefits make mobile pneumatic conveying systems a preferred choice for industries seeking efficient, flexible, and cost-effective material handling solutions.
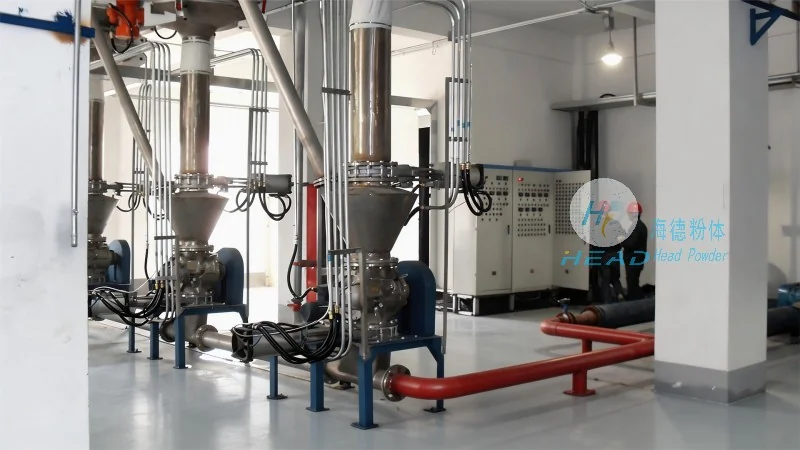
Applications and Industries
The mobile powder pneumatic conveying system finds applications across various industries, thanks to its adaptability and efficiency. In the pharmaceutical industry, it is used for transporting active pharmaceutical ingredients (APIs) and excipients, ensuring sterile and hygienic handling. The food processing sector employs these systems for conveying ingredients like flour, sugar, and spices, maintaining product quality and safety. In the chemical industry, the system handles a variety of powders, including chemicals and catalysts, with precision and control. Other industries, such as mining and construction, also benefit from the system's ability to transport bulk materials in remote or temporary locations. The versatility of the mobile system makes it a valuable asset for any operation requiring reliable and efficient powder handling.
Conclusion
In conclusion, the mobile powder pneumatic conveying system is a sophisticated and efficient solution for transporting bulk powders. Its design principles, centered on flexibility, reliability, and performance, make it an ideal choice for modern industries. With a focus on innovation and customer-centric solutions, Shandong HeadPowder Engineering Co., Ltd. continues to lead the way in providing high-quality mobile pneumatic conveying systems that meet the evolving needs of the market. Whether for pharmaceutical, food, or chemical applications, these systems offer a reliable and efficient means of material handling, ensuring productivity and compliance with industry standards.