Pharmaceutical powder handling systems are critical components in the manufacturing and processing of medicinal products. These systems are designed to safely and efficiently transport, store, and handle powders used in pharmaceutical applications. Understanding the components and design principles of such systems is essential for ensuring product quality, maintaining regulatory compliance, and optimizing production processes.
Introduction to Pharmaceutical Powder Handling Systems
Pharmaceutical powder handling systems are specialized equipment used in the pharmaceutical industry to manage powders, which are often the active ingredients or excipients in drug formulations. These systems are engineered to handle powders in a controlled environment, minimizing the risk of contamination, dust generation, and product degradation. The design of these systems is tailored to meet the stringent requirements of pharmaceutical manufacturing, including adherence to Good Manufacturing Practices (GMP) and other regulatory standards.
Key Components of a Pharmaceutical Powder Handling System
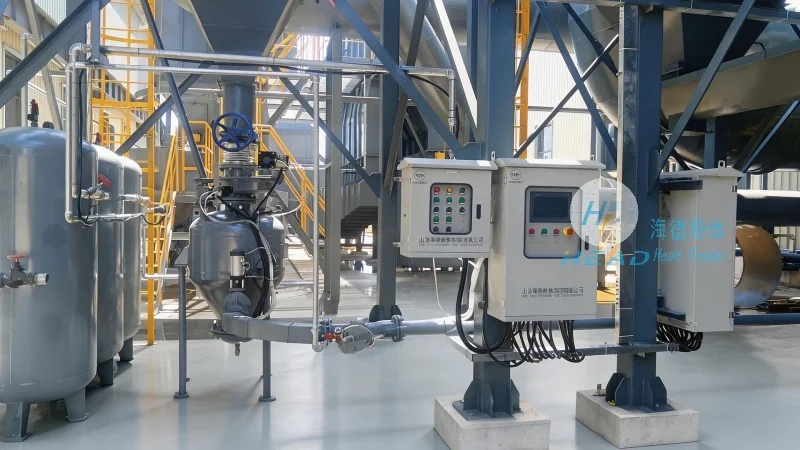
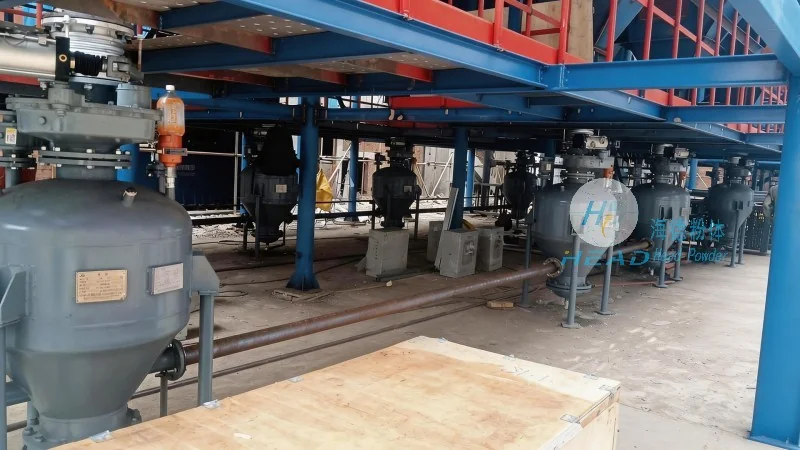
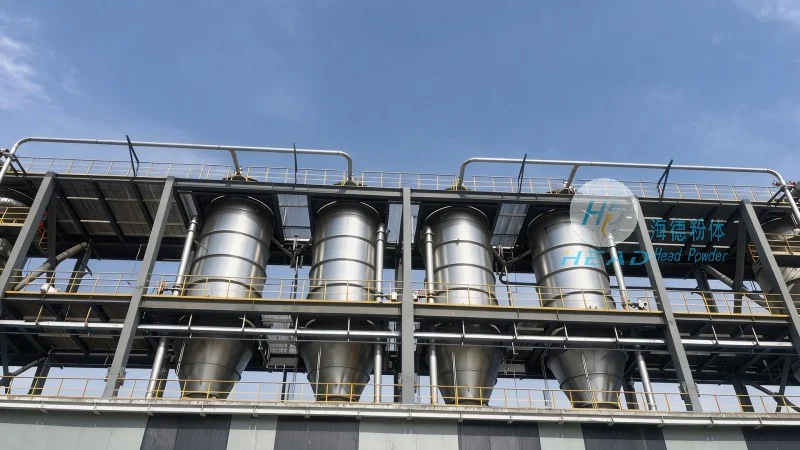
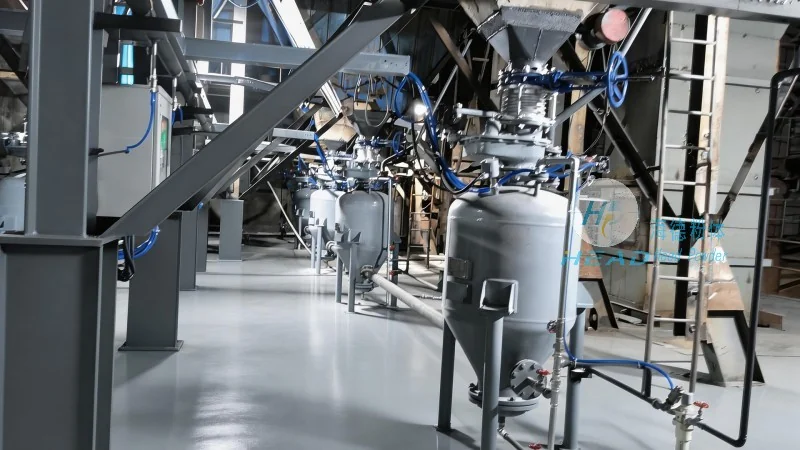
The core components of a pharmaceutical powder handling system typically include feeders, conveyors, storage vessels, and control systems. Feeders, such as rotary or vibratory feeders, are used to regulate the flow of powder from storage containers to processing equipment. Conveyors, including pneumatic or mechanical systems, transport the powder through the production line. Storage vessels, often equipped with agitators or mixers, ensure uniform powder distribution and prevent caking or segregation. Control systems, integrated with sensors and automation, monitor and adjust the flow rates and operational parameters to maintain consistent product quality.
Design Principles for Pharmaceutical Powder Handling Systems
The design of pharmaceutical powder handling systems follows several key principles to ensure safety, efficiency, and compliance. First, the system must be designed to minimize dust generation and prevent cross-contamination. This is achieved through the use of enclosed systems, air filtration, and proper sealing of components. Second, the system must be easy to clean and maintain, with components that can be disassembled and sanitized. This is crucial for maintaining GMP standards and ensuring product purity. Third, the system must be scalable and adaptable to different powder types and production volumes. The design allows for flexibility in processing various formulations without compromising performance or safety.
Role of Material Handling in Pharmaceutical Manufacturing
Material handling plays a vital role in pharmaceutical manufacturing, and powder handling systems are a key part of this process. These systems ensure that powders are transported from raw material storage to the final product packaging without any loss or contamination. The efficiency of the material handling process directly impacts the overall productivity and cost-effectiveness of the pharmaceutical production line. By optimizing the design and operation of powder handling systems, manufacturers can reduce downtime, minimize waste, and improve the quality of the final drug products.
Regulatory Considerations in Powder Handling System Design
Pharmaceutical powder handling systems must comply with various regulatory requirements, such as those outlined by the FDA and other international health authorities. The design of these systems must consider factors like contamination control, equipment validation, and documentation. Manufacturers must ensure that all components are made from materials that are compatible with pharmaceutical powders and do not introduce any harmful substances. Additionally, the system must be designed for easy inspection and maintenance, with clear documentation of all operational parameters and cleaning procedures.
Case Study: HeadPowder's Pharmaceutical Powder Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of pharmaceutical equipment, specializes in designing and manufacturing high-quality powder handling systems. The company's products are engineered to meet the specific needs of pharmaceutical manufacturers, with a focus on safety, efficiency, and compliance. HeadPowder's systems are designed using advanced materials and technologies to ensure durability and reliability in demanding pharmaceutical environments. The company's commitment to quality and customer satisfaction has made it a trusted partner for pharmaceutical companies worldwide.




