High-calcium powder conveying systems are essential equipment in industries that handle calcium-rich powders, such as food processing, pharmaceuticals, and chemical manufacturing. These systems are designed to efficiently transport high-calcium powders from storage to processing units, ensuring consistent flow and minimizing material loss. Understanding the components and design principles of such systems is crucial for optimizing operational efficiency and maintaining product quality.
HeadPowder: A Leading Provider of Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a renowned manufacturer specializing in advanced powder handling equipment. With a strong presence in China, particularly in Shandong, the company has established itself as a trusted partner for businesses seeking reliable and efficient high-calcium powder conveying systems. HeadPowder’s commitment to innovation and quality has positioned it as a key player in the industry, delivering solutions tailored to the unique needs of each client.
Key Components of High-Calcium Powder Conveying Systems
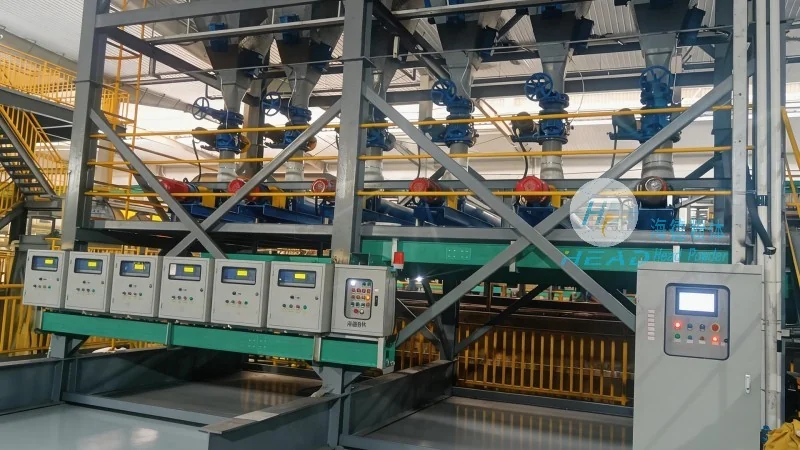
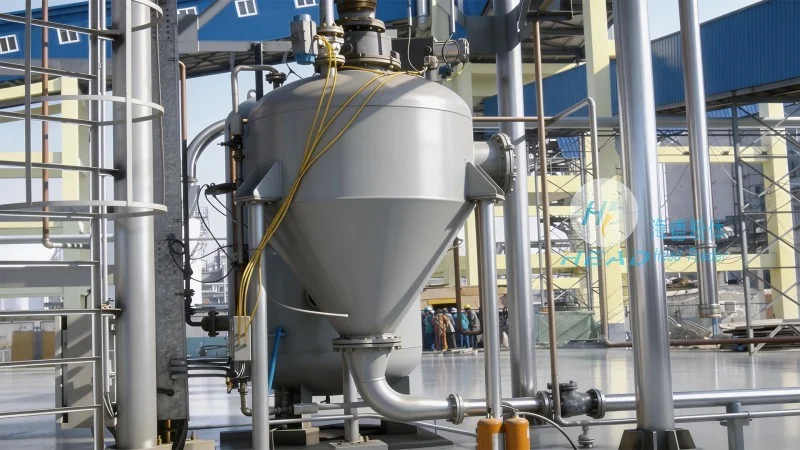
The design of a high-calcium powder conveying system typically involves several critical components that work in tandem to ensure smooth operation. These include feeders, conveyors, and control systems, each playing a vital role in the overall functionality. Feeders are responsible for accurately metering the powder, preventing overfilling or underfilling, which can affect downstream processes. Conveyors, such as pneumatic or mechanical systems, transport the powder through pipelines or ducts, while control systems monitor and adjust the flow rate based on real-time operational conditions.
Design Principles for Efficient High-Calcium Powder Handling
The design principles of high-calcium powder conveying systems focus on maximizing efficiency, minimizing material degradation, and ensuring safety. One key principle is the use of appropriate materials for construction, such as stainless steel or corrosion-resistant alloys, to prevent contamination and ensure durability. Another principle is the incorporation of anti-static features, as high-calcium powders can be prone to static buildup, which may lead to dust explosions or material agglomeration. Additionally, the system design considers the specific properties of the powder, including its density, flowability, and moisture content, to optimize conveying speed and reduce energy consumption.
Applications and Benefits of High-Calcium Powder Conveying Systems
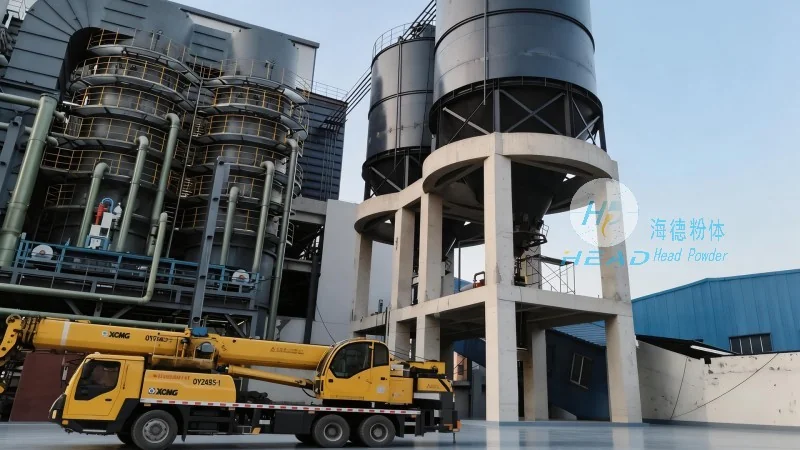
High-calcium powder conveying systems find widespread applications across various industries. In the food industry, they are used to transport calcium-rich ingredients like calcium carbonate or calcium phosphate in food production lines. In pharmaceuticals, these systems ensure the safe and hygienic handling of calcium-based drugs, maintaining compliance with regulatory standards. The benefits of using such systems include improved process control, reduced labor costs, and enhanced product consistency. By automating the powder conveying process, businesses can achieve higher throughput and lower operational costs, leading to increased profitability.
Conclusion and Contact Information
High-calcium powder conveying systems are indispensable in modern industrial operations, and choosing the right equipment is essential for success. Shandong HeadPowder Engineering Co., Ltd. offers a range of high-quality solutions designed to meet the specific requirements of high-calcium powder handling. With its expertise and commitment to quality, HeadPowder provides reliable and efficient systems that enhance operational performance and ensure product integrity. For more information or to explore how a high-calcium powder conveying system can benefit your business, please contact HeadPowder at its Shandong location.




