For industries dealing with bulk powders, maintaining a clean and efficient material handling process is paramount. A tote bag dust-free feeding station, often integrated with a powder conveying line, represents a sophisticated solution designed to address these challenges. This article explores the functionality, key design principles, and practical applications of such systems, highlighting how they enhance operational efficiency and product integrity.
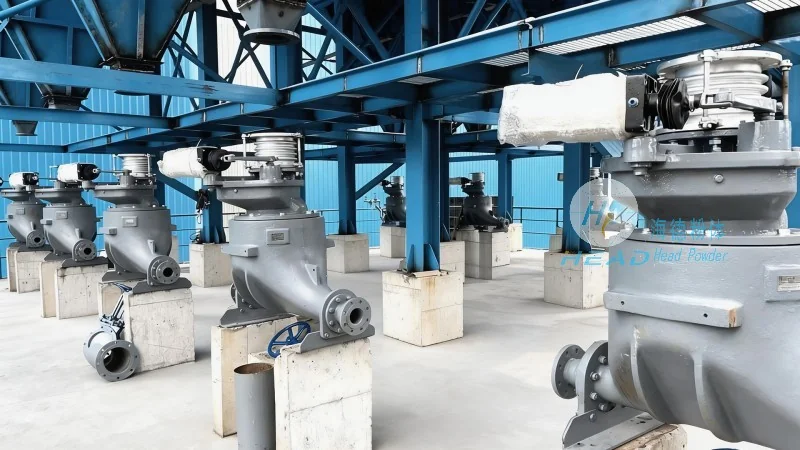
Introduction to Tote Bag Dust-Free Feeding Station and Powder Conveying Line
A tote bag dust-free feeding station is a specialized system used to transfer bulk powders from large tote bags into processing equipment or storage tanks while minimizing dust generation and contamination. The system typically includes a tote bag unloading mechanism, dust collection and filtration units, and a conveying component that transports the powder to its destination. This integrated approach ensures that the entire process remains enclosed, protecting both personnel and the environment from airborne particles.
Key Components and Design Principles
The design of a tote bag dust-free feeding station adheres to several core principles to ensure optimal performance. First, the system is built with a fully enclosed structure to contain dust and prevent cross-contamination. This includes airtight seals and negative pressure zones that capture any airborne particles. Second, the feeding mechanism is engineered to handle various powder types, from fine powders to bulkier materials, using adjustable flow control to maintain consistent feed rates. Third, the conveying line, often equipped with flexible or rigid hoses, is designed to minimize material degradation and ensure smooth transfer. The integration of these components is critical for achieving a seamless and efficient powder handling process.
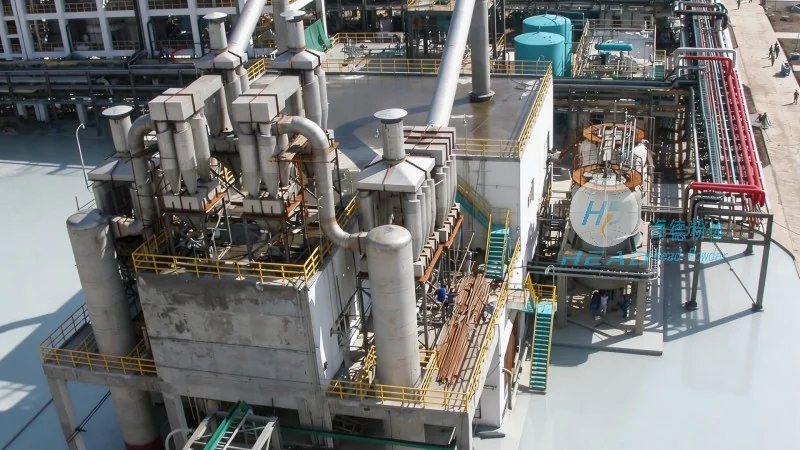
The Role of Dust-Free Feeding in Powder Handling
Dust-free feeding is essential in industries where powder quality and worker safety are top priorities. Traditional open feeding methods can lead to dust accumulation, equipment clogging, and health hazards. A tote bag dust-free feeding station addresses these issues by using a combination of vacuum or pressure systems to draw powder from the tote bag into the conveying line. The enclosed design ensures that all dust is captured and filtered, preventing it from escaping into the workspace. This not only improves air quality but also maintains the purity of the powder, which is crucial for applications in pharmaceuticals, food processing, and chemical manufacturing.
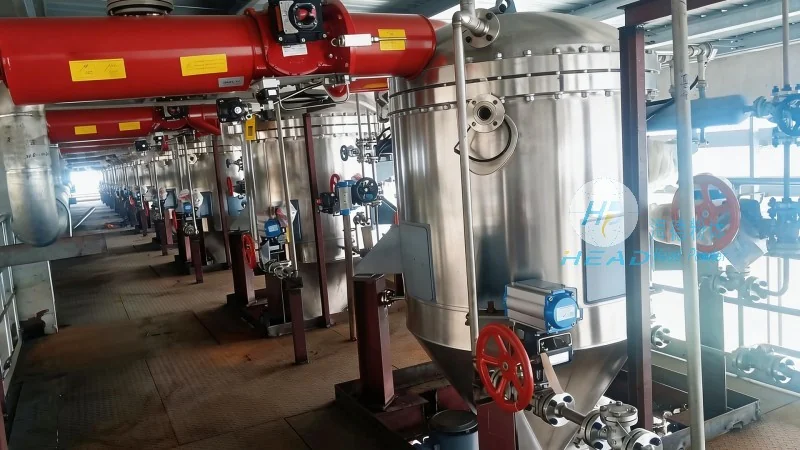
Practical Applications and Industry Benefits
The tote bag dust-free feeding station with a powder conveying line is widely used across various industries. In the pharmaceutical sector, it ensures that active ingredients are handled in a sterile environment, reducing the risk of contamination. In the food industry, it maintains product safety and compliance with hygiene standards. For chemical manufacturers, it enhances process efficiency and reduces downtime caused by equipment maintenance. The benefits extend beyond operational efficiency; these systems also contribute to cost savings by minimizing material waste and reducing the need for frequent cleaning and maintenance.
Company Overview and Commitment to Quality
Shandong HeadPowder Engineering Co., Ltd., based in China, specializes in the design and manufacturing of advanced powder handling systems. With a focus on innovation and customer-centric solutions, the company has established itself as a leader in the industry. HeadPowder's products are engineered to meet the highest standards of quality and reliability, ensuring that clients receive systems that are tailored to their specific needs. The company's commitment to research and development ensures that its solutions remain at the forefront of technology, providing sustainable and efficient solutions for bulk powder handling challenges.




