HeadPowder, a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and implementation of pneumatic conveying systems tailored for magnesium oxide powder. This article provides a comprehensive classification and application analysis of such systems, highlighting the technical aspects, operational advantages, and practical implementations in industrial settings.
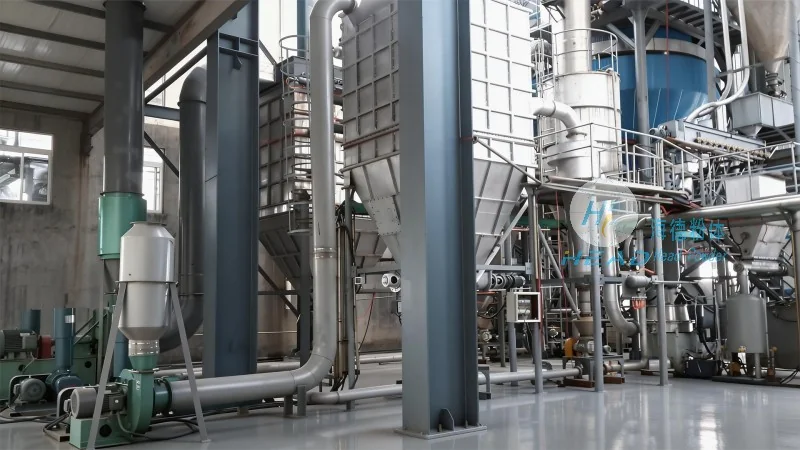
Overview of Pneumatic Conveying Systems for Magnesium Oxide Powder
Pneumatic conveying systems are widely used in the powder handling industry to transport materials like magnesium oxide powder efficiently and safely. These systems utilize air or gas to move powder through pipelines, offering advantages such as reduced contamination, improved process control, and enhanced safety compared to traditional mechanical conveying methods. The classification of these systems is primarily based on the pressure used during operation, which can be categorized into two main types: pressure and vacuum systems.
Classification of Magnesium Oxide Powder Pneumatic Conveying Systems
1. Pressure Pneumatic Conveying Systems: These systems operate under positive pressure, where air is forced through the pipeline to push the powder forward. They are suitable for long-distance and high-capacity transport of magnesium oxide powder. Key components include a positive displacement blower, a hopper for material storage, and a pipeline network. The pressure system is effective for applications requiring consistent flow rates and minimal particle degradation.
2. Vacuum Pneumatic Conveying Systems: In contrast, vacuum systems operate under negative pressure, drawing the powder into the pipeline using a vacuum pump. This method is ideal for short-distance transport or when the material needs to be conveyed from multiple sources. Vacuum systems are particularly useful for handling magnesium oxide powder in environments where dust control is critical, as they can capture and contain particles effectively.
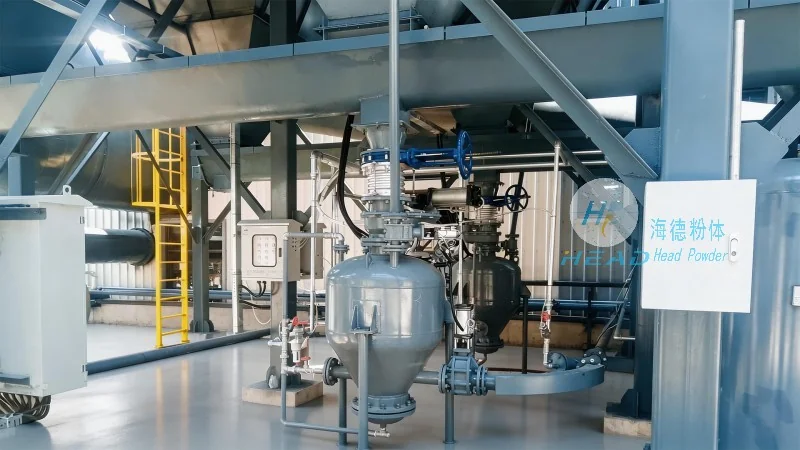
Key Features and Advantages of Magnesium Oxide Powder Pneumatic Conveying Systems
Both pressure and vacuum systems offer several benefits when handling magnesium oxide powder. The primary advantages include:
- Hygienic and Clean Operation: Pneumatic conveying minimizes direct contact between the powder and equipment, reducing the risk of contamination and ensuring product purity, which is crucial for magnesium oxide used in pharmaceutical or food industries.
- Energy Efficiency: Modern systems utilize high-efficiency blowers and optimized pipeline designs to reduce energy consumption while maintaining high transport efficiency.
- Flexibility in Layout: The modular design of pneumatic conveying systems allows for easy integration into existing production lines or new facility setups, accommodating changes in production scale or process requirements.
- Reduced Maintenance: Compared to mechanical conveyors, pneumatic systems have fewer moving parts, leading to lower maintenance costs and longer equipment lifespan.
Application Analysis of Magnesium Oxide Powder Pneumatic Conveying Systems
The application of magnesium oxide powder pneumatic conveying systems varies across different industries. Here are some key sectors where these systems are widely utilized:
1. Pharmaceutical Industry: In pharmaceutical manufacturing, magnesium oxide is used as an antacid and in drug formulations. The pneumatic conveying system ensures that the powder is transported under sterile conditions, maintaining compliance with GMP (Good Manufacturing Practice) standards. The system's ability to handle fine powders without agglomeration is critical for maintaining product quality.
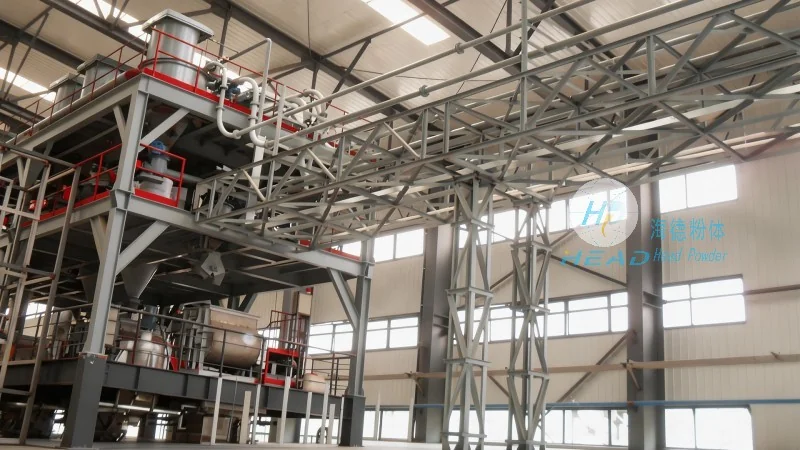
2. Food and Beverage Industry: Magnesium oxide is used as a food additive and in the production of certain beverages. The clean and hygienic nature of pneumatic conveying systems makes them suitable for food processing environments, where contamination control is paramount.
3. Chemical Manufacturing: In chemical plants, magnesium oxide is used as a catalyst or in the production of other chemical compounds. The high-capacity and long-distance transport capabilities of pressure pneumatic systems are beneficial for moving large quantities of powder between different processing stages.
4. Construction Materials Industry: Magnesium oxide is used in the production of fire-resistant materials and building products. The robust design of pneumatic conveying systems can handle the abrasive nature of some magnesium oxide powders, ensuring reliable operation over extended periods.
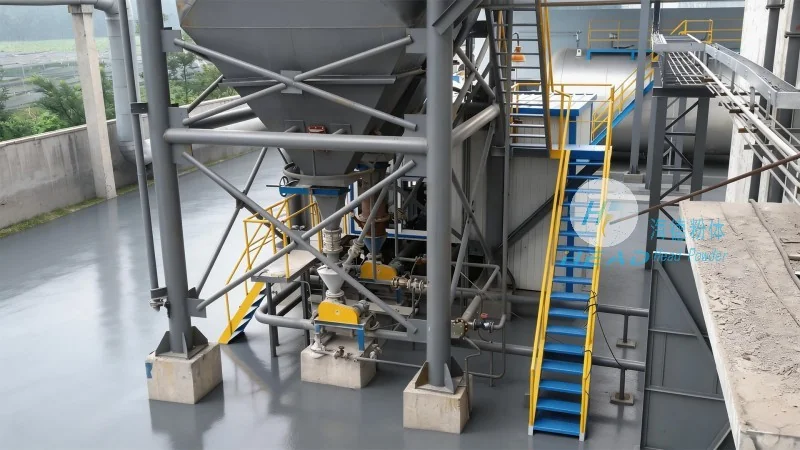
Implementation and Customization by HeadPowder
Shandong HeadPowder Engineering Co., Ltd. (HeadPowder) specializes in providing customized pneumatic conveying solutions for magnesium oxide powder. The company's expertise lies in designing systems that meet specific customer requirements, including material flow rates, pipeline lengths, and environmental regulations. HeadPowder's engineers work closely with clients to assess their operational needs and recommend the most suitable system configuration.
For example, a client in the pharmaceutical industry may require a vacuum system with advanced filtration to ensure particle size control and compliance with regulatory standards. HeadPowder's team can design a system with integrated dust collection and particle size monitoring to meet these specific needs. Similarly, a chemical manufacturer might need a pressure system with high-pressure blower capabilities to transport large volumes of magnesium oxide over long distances.
Conclusion
Pneumatic conveying systems for magnesium oxide powder offer significant advantages in terms of efficiency, safety, and product quality. The classification into pressure and vacuum systems allows for tailored solutions based on specific application requirements. As a leading provider in the industry, HeadPowder continues to innovate and deliver reliable pneumatic conveying systems that enhance operational performance and support the growth of industries relying on magnesium oxide powder.




