Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier specializing in pneumatic conveying systems tailored for the transportation of sodium bicarbonate. With a focus on efficiency, safety, and reliability, our company has established itself as a leading provider in the industry, serving clients with customized solutions that meet their specific operational needs.
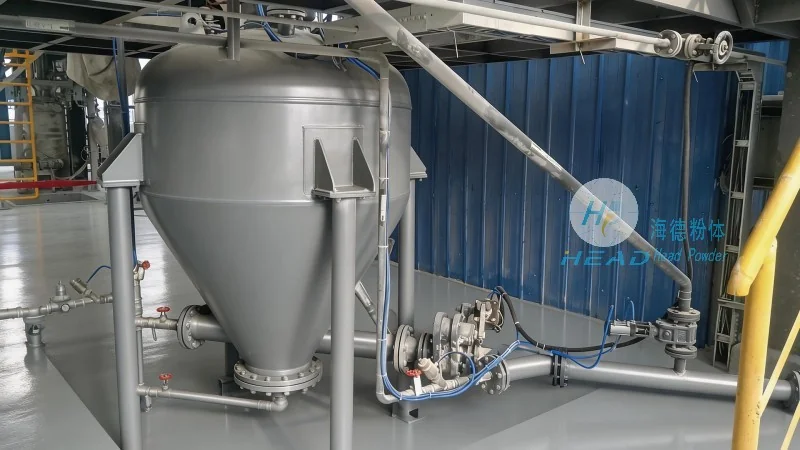
Pneumatic Conveying Systems for Sodium Bicarbonate: An Overview
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials like sodium bicarbonate through a pipeline using compressed air. This technology offers several advantages over traditional mechanical conveying methods, including reduced risk of product contamination, lower maintenance requirements, and the ability to handle materials in a dust-free environment. For sodium bicarbonate, which is often used in pharmaceuticals, food processing, and chemical industries, maintaining product purity is paramount. Pneumatic conveying systems effectively prevent cross-contamination and preserve the quality of the material during transport.
Key Benefits of Pneumatic Conveying for Sodium Bicarbonate
One of the primary benefits of using pneumatic conveying for sodium bicarbonate is its ability to handle fine powders without clogging or degradation. The system uses a combination of positive and negative pressure to move the material through the pipeline, ensuring a consistent flow rate and preventing material buildup. This is particularly important for sodium bicarbonate, which can be sensitive to moisture and temperature changes. Our systems are designed with materials that are resistant to corrosion and wear, ensuring long-term durability and minimal downtime.
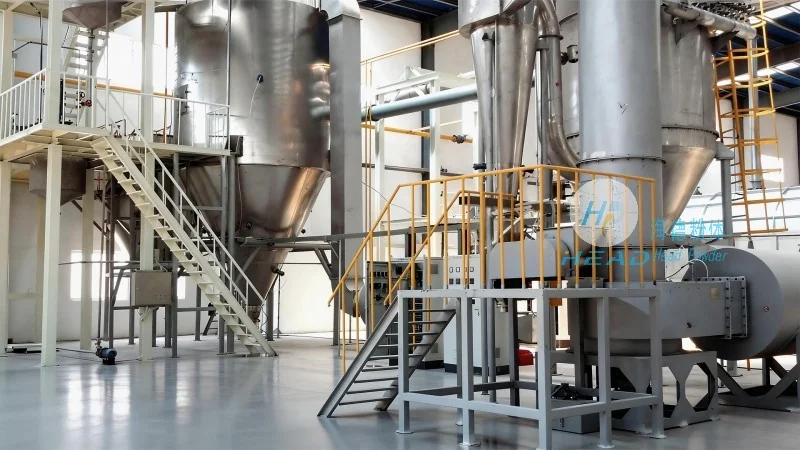
Another significant advantage is the improved safety and hygiene standards. Pneumatic conveying eliminates the need for manual handling of bulk materials, reducing the risk of accidents and exposure to dust. This is crucial in industries where sodium bicarbonate is used in food or pharmaceutical applications, where strict regulatory compliance is required. Our systems are equipped with advanced filtration and dust collection mechanisms to maintain a clean working environment.
Customized Solutions for Diverse Applications
Shandong HeadPowder Engineering Co., Ltd. understands that each client has unique requirements when it comes to transporting sodium bicarbonate. Whether the application involves short-distance or long-distance transport, high or low flow rates, our team of experts works closely with clients to design and implement tailored pneumatic conveying solutions. We consider factors such as the material's characteristics, the desired transport speed, and the existing infrastructure to ensure the system is optimized for performance and cost-effectiveness.
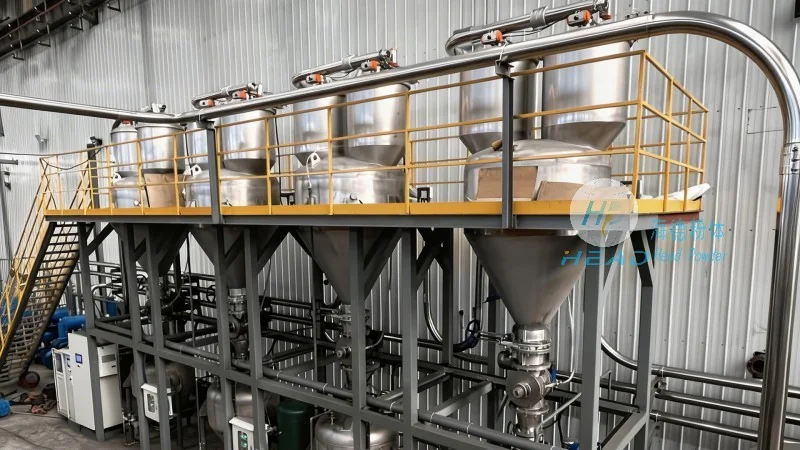
Our customized systems can be integrated with existing production lines or serve as standalone units, depending on the client's needs. We also provide maintenance and support services to ensure the continuous operation of the conveying system. By leveraging our expertise in pneumatic technology, we help clients enhance their operational efficiency and reduce overall costs associated with material handling.
Quality Assurance and Compliance
At Shandong HeadPowder Engineering Co., Ltd., we adhere to strict quality control standards to ensure that our pneumatic conveying systems meet the highest industry benchmarks. Our manufacturing processes are ISO-certified, and we use only premium materials to construct our equipment. This commitment to quality ensures that our systems are reliable, durable, and safe for use in various industrial applications.
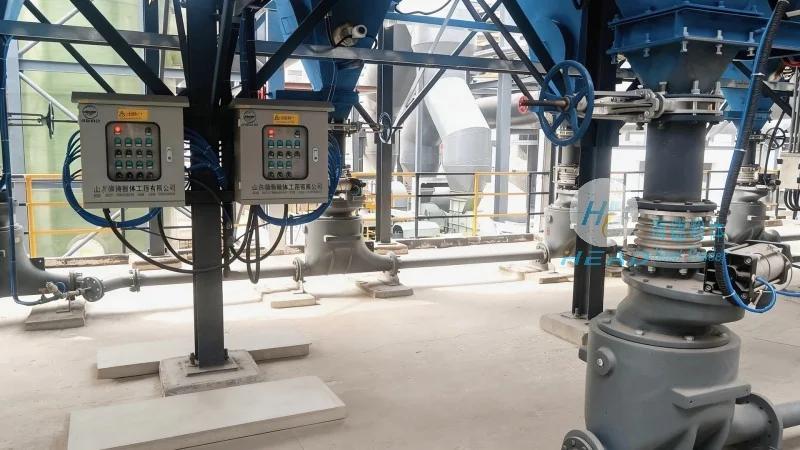
Moreover, we comply with all relevant industry regulations and standards, including those related to food safety and pharmaceutical manufacturing. This ensures that our clients can operate with confidence, knowing that their sodium bicarbonate is handled in a manner that meets or exceeds regulatory requirements.
Conclusion
Pneumatic conveying plays a vital role in the efficient and safe transportation of sodium bicarbonate. By leveraging advanced technology and customized solutions, Shandong HeadPowder Engineering Co., Ltd. provides reliable systems that enhance productivity and maintain product quality. Our commitment to quality, safety, and customer satisfaction has made us a trusted partner for businesses in the pharmaceutical, food, and chemical industries. Whether you are looking to upgrade your existing conveying system or implement a new one, our team is ready to assist you in achieving your operational goals.




