HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored for the coal and coke industries. This article explores the critical functions and advantages of pneumatic conveying in the efficient transport of these essential raw materials.
Understanding Pneumatic Conveying Systems
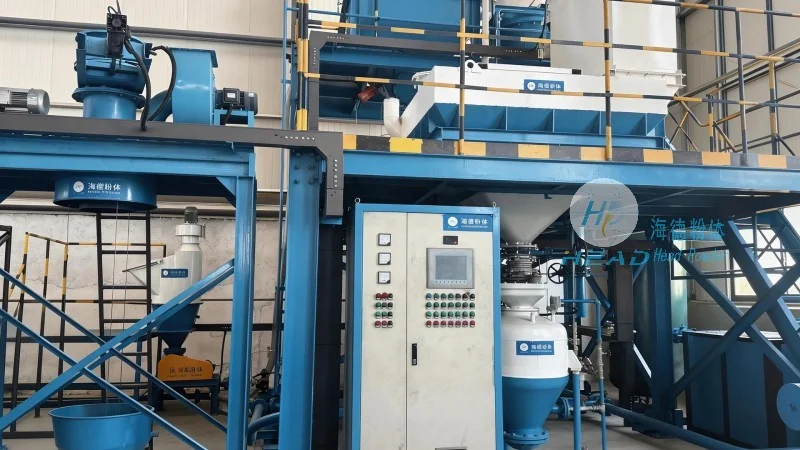
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials like coal and coke through a pipeline using pressurized or vacuum air. The process involves feeding the material into a hopper, where it is mixed with air and then propelled through the pipeline to the destination. This technology offers a non-contact, dust-free, and flexible solution for material handling, which is particularly valuable in industries where traditional belt or bucket elevators may be impractical or inefficient.
Key Applications in Coal and Coke Handling
For coal and coke transportation, pneumatic conveying systems are employed in various stages of the production and processing workflow. From raw material storage and transfer to the blending and loading of finished products, these systems enhance operational efficiency and safety. In coal mines, pneumatic conveyors can be used to move coal from extraction points to processing facilities, reducing the need for manual handling and minimizing the risk of dust exposure. Similarly, in coke plants, the transport of coke from the coking process to storage or shipping areas is streamlined through pneumatic systems, ensuring consistent flow and reducing downtime.
Advantages of Pneumatic Conveying in Coal and Coke Transport
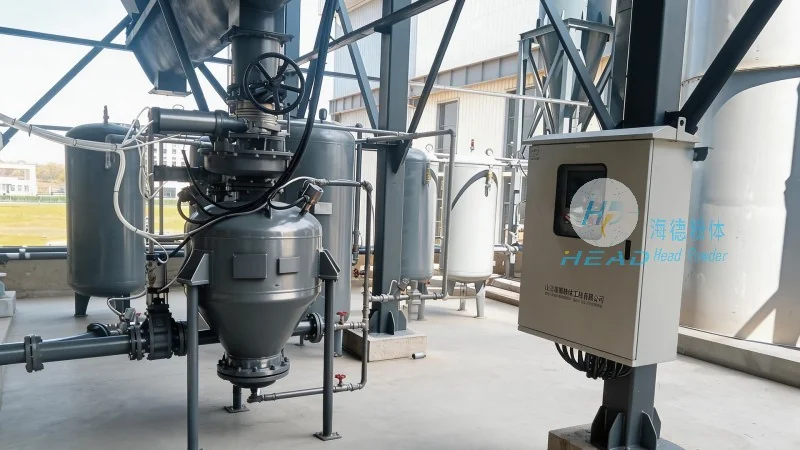
Several key advantages make pneumatic conveying an ideal choice for coal and coke handling. Firstly, it provides a dust-free environment, which is crucial for maintaining workplace safety and compliance with environmental regulations. Unlike traditional methods that generate significant dust, pneumatic systems contain the material within a sealed pipeline, preventing airborne particles from contaminating the air and affecting workers' health. Secondly, these systems offer high flexibility in terms of layout and routing. Pipelines can be installed in various configurations, including vertical, horizontal, or a combination of both, allowing for complex material flow paths without the need for extensive infrastructure modifications. Thirdly, pneumatic conveying enables continuous and automated material transport, which improves production throughput and reduces labor costs. The ability to operate 24/7 with minimal maintenance further enhances the economic viability of these systems.
HeadPowder's Expertise in Pneumatic Conveying Solutions
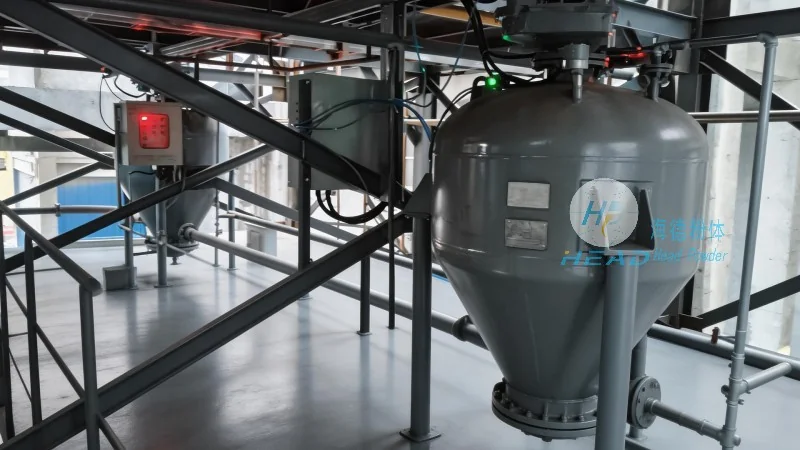
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, has established itself as a trusted provider of customized pneumatic conveying solutions for the coal and coke sector. The company leverages advanced engineering principles and years of industry experience to design systems that meet the specific requirements of each client. Whether it's a new plant installation or the upgrade of an existing system, HeadPowder's team of experts conducts thorough assessments to determine the most suitable conveying method, material characteristics, and operational parameters. The company's product portfolio includes a range of components such as rotary valves, airlocks, and filter units, all engineered to ensure reliable and efficient operation. By focusing on quality and customer satisfaction, HeadPowder has built a reputation for delivering durable and cost-effective pneumatic conveying systems that enhance the productivity and safety of coal and coke handling operations.
Conclusion
In conclusion, pneumatic conveying plays a vital role in the efficient and safe transport of coal and coke. The technology's ability to provide dust-free, flexible, and automated material handling makes it an indispensable component of modern industrial operations. With its expertise and commitment to excellence, HeadPowder Engineering Co., Ltd. continues to provide innovative solutions that address the unique challenges of the coal and coke industry, helping clients achieve optimal performance and operational efficiency.




