Rapeseed material pneumatic conveying represents a critical technology in the processing and handling of rapeseed, delivering efficient and reliable methods for transporting seeds between different stages of production. This article delves into the working principle and key characteristics of this system, offering a comprehensive overview of its application and benefits.
Exploring the Working Principle of Rapeseed Material Pneumatic Conveying
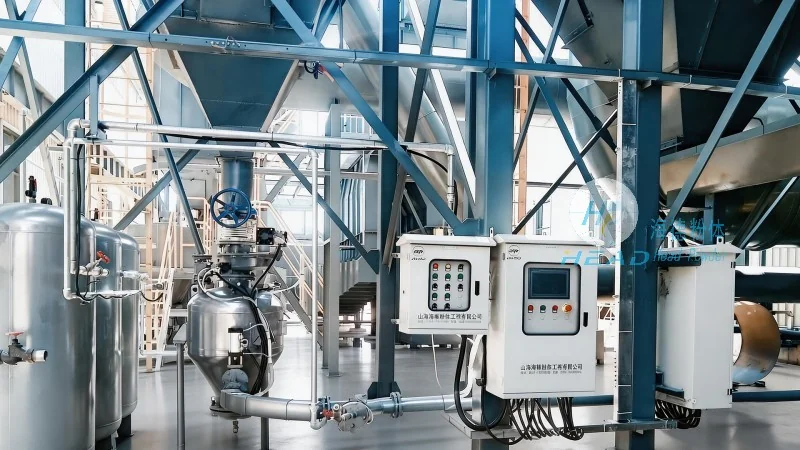
The fundamental mechanism of rapeseed material pneumatic conveying centers on utilizing air as the primary conveying medium. The system typically comprises several key components: a material hopper, a blower or fan to generate airflow, a network of pipelines, and a receiving hopper. When the system is activated, the blower produces a controlled flow of air within the pipeline. As rapeseed material is introduced into the hopper, it is drawn into the pipeline by the air stream, forming a suspension of particles in the air. This suspended mixture is then transported through the pipeline to the receiving hopper. The air flow is carefully regulated to ensure the material is conveyed without excessive pressure or friction, thereby minimizing product damage and ensuring efficient transport while maintaining the quality of the rapeseed.
Key Characteristics of Rapeseed Material Pneumatic Conveying Systems
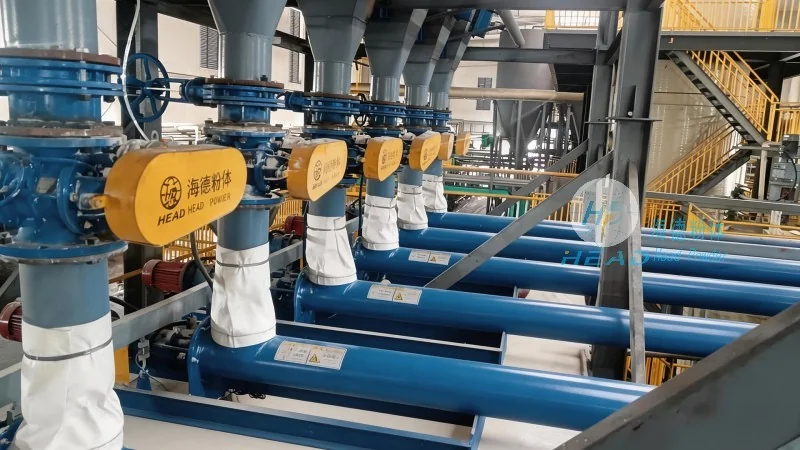
Several distinct characteristics define the performance and suitability of rapeseed material pneumatic conveying systems. Firstly, the system provides a dust-free and hygienic conveying process, which is essential for preserving the quality and integrity of rapeseed, particularly in food processing applications where product purity is paramount. Secondly, the system offers a flexible and compact design, allowing for seamless integration into existing processing lines and adaptation to various spatial constraints within a facility. Thirdly, the system is capable of handling a wide range of material sizes and densities, making it versatile for different rapeseed varieties and processing stages, from raw seed to processed products. Additionally, the pneumatic conveying system is energy-efficient compared to traditional mechanical conveyors, reducing operational costs and environmental impact by minimizing energy consumption and mechanical wear. Finally, the system is easy to maintain and clean, with components that can be easily disassembled and sanitized, ensuring compliance with industry standards and regulations, particularly in food and agricultural sectors.
About Shandong HeadPowder Engineering Co., Ltd.
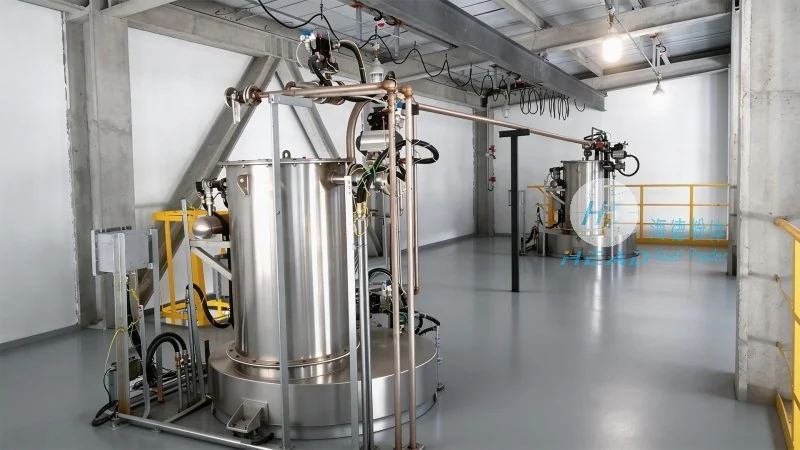
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of pneumatic conveying systems and related equipment. With a strong commitment to innovation and quality, HeadPowder specializes in designing and producing customized solutions for diverse material handling applications, including those involving rapeseed and other agricultural products. The company is dedicated to delivering reliable, efficient, and cost-effective solutions that meet the specific needs of its clients. HeadPowder's products are engineered to deliver optimal performance, durability, and safety, ensuring long-term satisfaction and operational excellence for its customers. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility and a dedicated research and development team focused on advancing pneumatic conveying technology.




