Straw powder, a byproduct of agricultural activities, is increasingly being utilized in various industrial processes. The efficient and reliable transport of this material is crucial for optimizing production workflows. Pneumatic conveying systems have emerged as a preferred solution for handling straw powder due to their ability to minimize material degradation and operational costs.
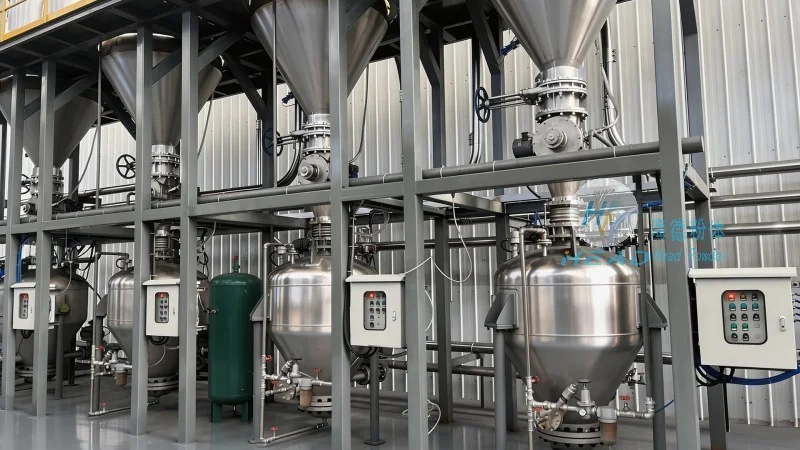
Overview of Pneumatic Conveying Systems
Pneumatic conveying systems utilize air or gas to transport bulk materials like straw powder through a pipeline. These systems are categorized into two main types: positive pressure and negative pressure systems. Positive pressure systems push material forward using compressed air, while negative pressure systems draw material in using vacuum. Each type offers distinct advantages depending on the specific requirements of the straw powder handling application.
Types of Pneumatic Conveying Systems for Straw Powder
1. Positive Pressure Conveying: This system operates by blowing air into the material, creating a positive pressure that propels the powder through the pipeline. It is ideal for applications requiring high material flow rates and long-distance transport. The design typically includes a blower, a hopper for material storage, and a discharge point at the destination. Positive pressure systems are effective in preventing material contamination and are suitable for handling fine or dusty straw powders.
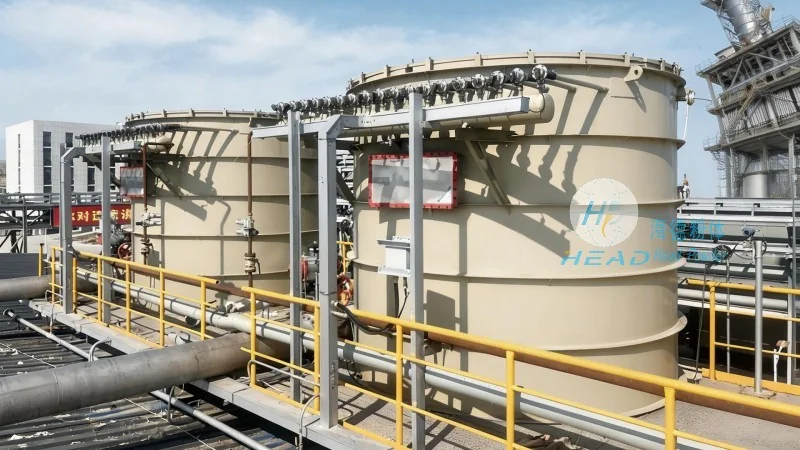
2. Negative Pressure (Vacuum) Conveying: In contrast, negative pressure systems use a vacuum to draw material from the source into the pipeline. This method is well-suited for short-distance transport and applications where the material needs to be collected from multiple points. The system comprises a vacuum pump, a collection hopper, and a discharge unit. Negative pressure conveying is advantageous for handling materials that are sensitive to pressure changes or for environments where dust control is critical.
3. Combination Systems: Some applications may benefit from a hybrid approach, combining elements of both positive and negative pressure systems. These systems are designed to optimize performance based on varying operational conditions, such as fluctuating material flow rates or changes in pipeline length. By integrating multiple conveying modes, combination systems can enhance efficiency and reduce energy consumption.
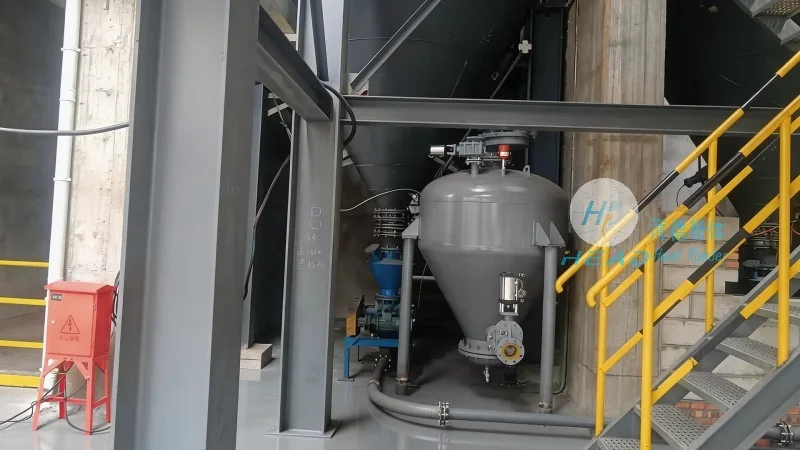
Practical Applications in Straw Powder Processing
The practical application of pneumatic conveying systems in straw powder processing spans multiple industries. In the agricultural sector, these systems are used for transporting straw powder from storage facilities to processing plants, ensuring a continuous supply of raw material. In the biofuel industry, pneumatic conveyors facilitate the transport of straw powder to biomass boilers or gasifiers, where it is converted into energy. Additionally, in the animal feed industry, these systems help in delivering straw powder to feed mills, improving production efficiency and reducing handling time.
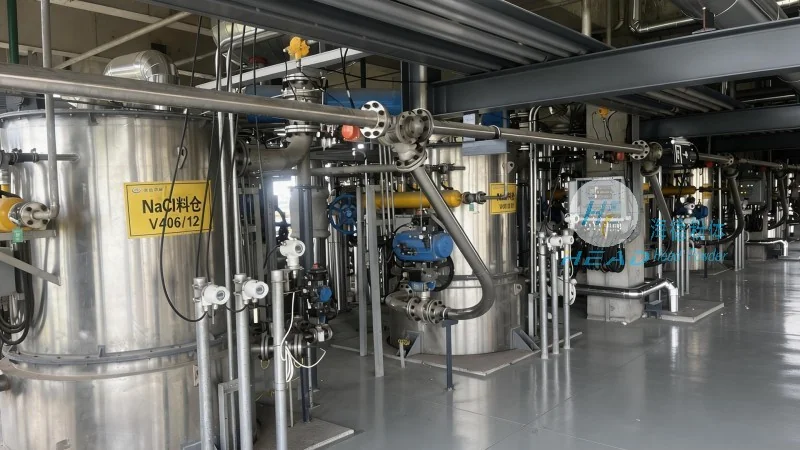
Key Considerations for Selecting a Pneumatic Conveying System
When selecting a pneumatic conveying system for straw powder transport, several factors must be considered. The first is the material characteristics, including particle size, moisture content, and flowability. Straw powder typically consists of fine particles, which may require specialized equipment to prevent blockages or degradation. The second consideration is the distance and layout of the transport route. Longer distances may necessitate higher air pressure or more powerful blower systems, while complex layouts may require additional components like bends or valves. Energy efficiency is another critical factor, as pneumatic conveying systems can consume significant power. Therefore, choosing a system with optimal air flow and pressure control is essential to minimize operational costs.
HeadPowder's Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique needs of straw powder handling. With years of experience in the industry, HeadPowder has developed a range of solutions that address the specific challenges of straw powder transport, such as material variability and environmental regulations. The company's engineers work closely with clients to assess their operational requirements and recommend the most suitable system configuration. HeadPowder's products are known for their durability, efficiency, and compliance with industry standards, ensuring reliable performance in diverse applications.




