For breweries, efficiently handling and transporting beer mash and other byproducts is a critical operational challenge. Traditional methods like manual handling or mechanical conveyors often present significant drawbacks, including high labor costs, equipment wear and tear, and potential contamination risks. This is where advanced pneumatic conveying systems, specifically designed for beer brewery waste, offer a superior solution. The following content introduces the design principles and practical applications of such a system, highlighting its benefits and the engineering expertise behind it.
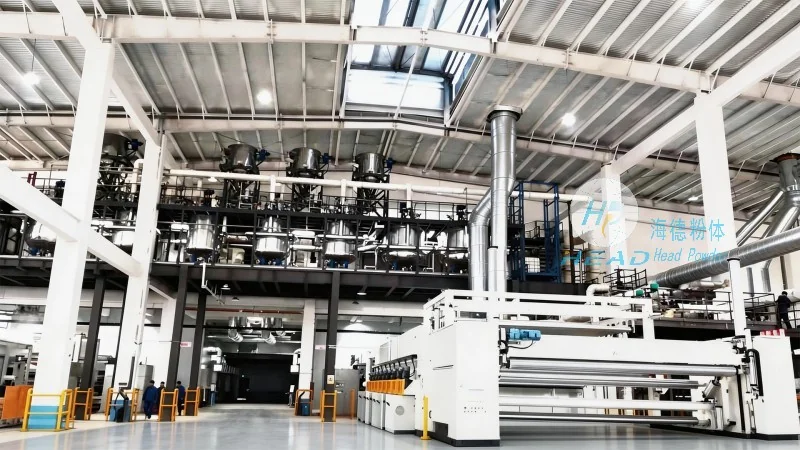
Understanding the Need for Specialized Pneumatic Conveying in Breweries
Breweries generate large volumes of beer mash, a solid-liquid mixture that requires careful management to maintain product quality and operational efficiency. Conventional conveyors may struggle with the sticky, abrasive nature of beer mash, leading to blockages, increased maintenance, and reduced throughput. Pneumatic conveying systems, which use air pressure to transport materials, provide a non-contact method that minimizes product degradation and equipment damage. This makes them ideal for handling sensitive brewery waste while ensuring consistent performance.
Key Design Considerations for Beer Mash Pneumatic Conveying
The design of a pneumatic conveying system for beer mash involves several critical factors to ensure optimal performance. First, the system must be tailored to the specific characteristics of the material, including its moisture content, particle size, and flowability. For beer mash, which is typically wet and viscous, a positive displacement or pressure pneumatic system is often preferred. These systems generate sufficient air pressure to move the material through pipelines without clogging. Additionally, the system must incorporate features like air filtration and moisture control to prevent equipment corrosion and maintain hygiene standards. The choice of materials for pipelines and components is also crucial, as they need to withstand the corrosive nature of beer mash and cleaning agents.
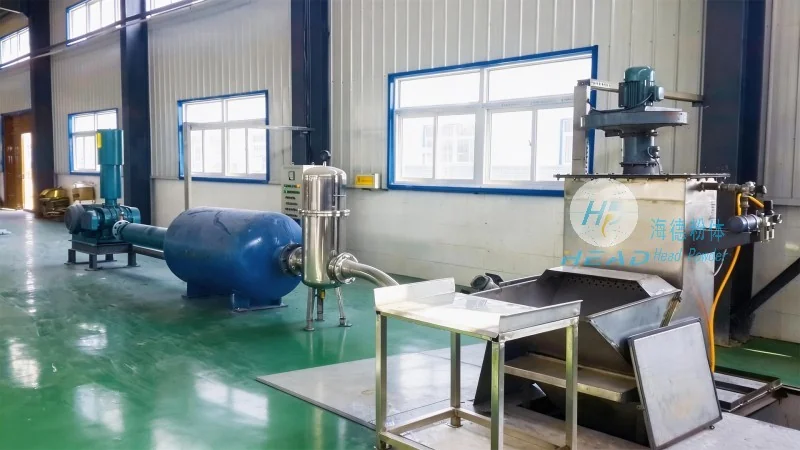
Components and Technology in the Pneumatic Conveying System
A typical pneumatic conveying system for beer mash includes several key components: a hopper for material storage, a feeder to control the flow rate, a compressor to generate air pressure, and a pipeline network to transport the material. The hopper is designed with a sloped bottom to facilitate material discharge and prevent buildup. The feeder, often a rotary valve or screw feeder, ensures a consistent flow of beer mash into the system. The compressor, usually an air-driven unit, provides the necessary pressure to move the material through the pipeline. The pipeline network is constructed from materials like stainless steel or food-grade plastic to resist corrosion and maintain hygiene. The system may also include features like air filters to remove moisture and debris, and pressure relief valves to prevent over-pressurization.
Benefits of Implementing a Pneumatic Conveying System for Beer Brewery Waste
Adopting a specialized pneumatic conveying system for beer mash offers numerous advantages for breweries. Firstly, it significantly reduces labor costs by automating the material handling process, eliminating the need for manual labor in transporting heavy and bulky waste. Secondly, it improves operational efficiency by increasing throughput and reducing downtime due to equipment blockages. Thirdly, it enhances product quality by minimizing contamination and degradation of the beer mash, which is essential for maintaining the quality of the final beer product. Additionally, the system reduces equipment wear and tear, lowering maintenance costs and extending the lifespan of the conveying equipment. Finally, it improves workplace safety by eliminating the need for manual handling of heavy loads, reducing the risk of injuries.
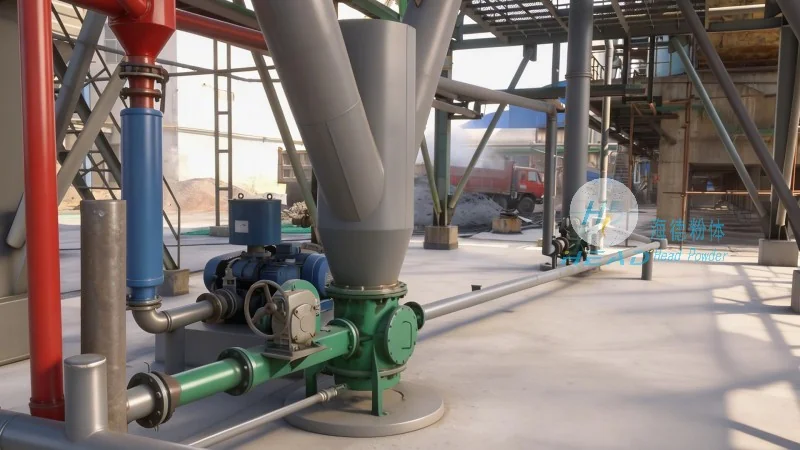
Engineering Expertise from Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing systems tailored to the unique needs of breweries. With years of experience in the industry, the company has developed a deep understanding of the challenges faced by breweries in handling beer mash and other waste products. The company's team of engineers and technicians work closely with clients to assess their specific requirements and design a customized pneumatic conveying system that meets their operational needs. The company uses advanced design software and testing facilities to ensure that the system is optimized for performance and reliability. Additionally, the company provides comprehensive after-sales support, including maintenance services and technical assistance, to ensure that the system operates at peak efficiency throughout its lifespan.
Conclusion and Application
Pneumatic conveying systems for beer brewery waste are a proven and effective solution for breweries looking to improve their operational efficiency and product quality. By leveraging advanced engineering and specialized technology, these systems offer a reliable and cost-effective way to handle beer mash and other byproducts. For breweries seeking to upgrade their material handling processes, partnering with a reputable engineering company like Shandong HeadPowder Engineering Co., Ltd. can provide the expertise and support needed to implement a successful pneumatic conveying system. With the right design and implementation, breweries can achieve significant improvements in productivity, cost savings, and overall operational performance.




