What is a Desulfurization Sodium Bicarbonate Powder Handling System? And What Are Its Design Princip
Release time:2026-09-14 15:11:16
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Desulfurization processes in industrial applications often rely on sodium bicarbonate as a key reagent. The efficient handling and transportation of this powder are critical to maintaining system performance and operational efficiency. This article explores the desulfurization sodium bicarbonate powder handling system, detailing its design principles and the engineering solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
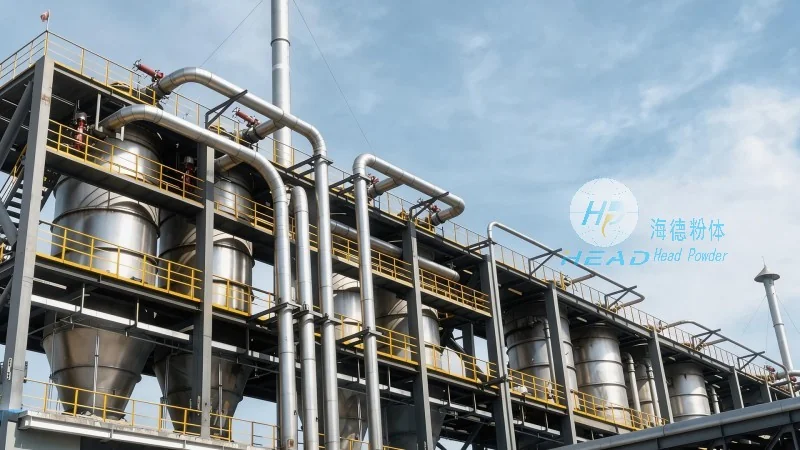
Understanding the Desulfurization Sodium Bicarbonate Powder Handling System
The desulfurization sodium bicarbonate powder handling system is a specialized equipment setup designed to safely and effectively transport sodium bicarbonate, a white crystalline powder commonly used in flue gas desulfurization (FGD) processes. This system addresses the unique challenges associated with handling fine powders, such as dust generation, caking, and material flow control. By integrating advanced engineering and material handling technologies, the system ensures consistent performance and minimal downtime in industrial desulfurization operations.
Key Components and Design Principles
The design of the desulfurization sodium bicarbonate powder handling system is based on several core principles to optimize performance and reliability. These include:
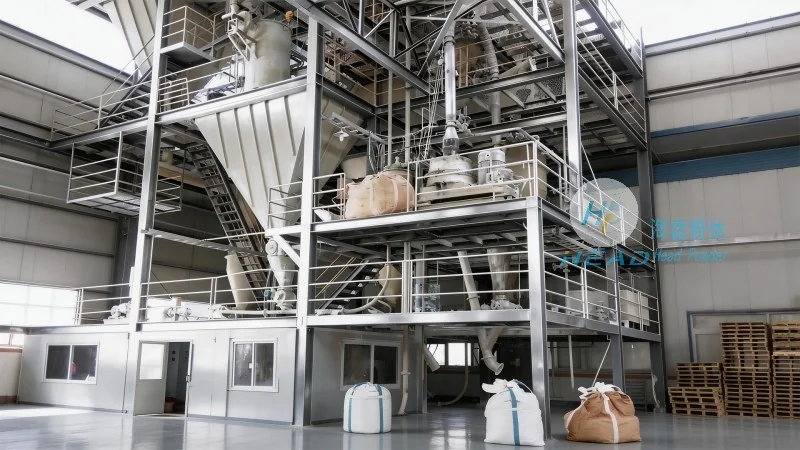
- Material Compatibility: Components are constructed from materials that are resistant to chemical corrosion and wear, ensuring long-term durability in harsh industrial environments.
- Flow Control and Dosing: The system incorporates precise flow control mechanisms, such as rotary valves and dosing pumps, to regulate the amount of sodium bicarbonate added to the desulfurization process. This ensures optimal reagent usage and maintains the desired pH levels in the flue gas treatment.
- Dust Suppression and Safety: Integrated dust collection and suppression systems are included to minimize airborne particulate emissions, enhancing workplace safety and compliance with environmental regulations.
- Automation and Monitoring: Modern systems feature automated controls and real-time monitoring capabilities, allowing operators to track system performance and detect potential issues before they lead to operational failures.
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design and manufacturing of such specialized powder handling systems. The company leverages years of experience in chemical engineering and material handling to develop customized solutions tailored to the specific needs of industrial desulfurization plants.
How the System Works: A Step-by-Step Overview
The operation of the desulfurization sodium bicarbonate powder handling system typically involves the following steps:
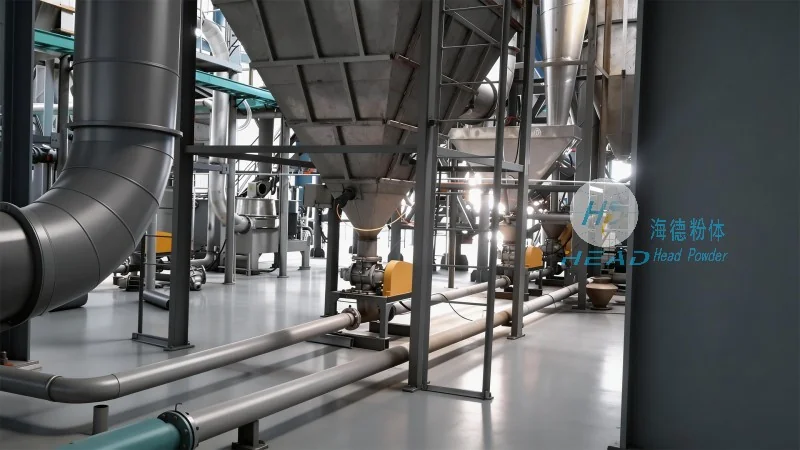
- Powder Storage: Sodium bicarbonate is stored in a sealed hopper or silo, which prevents moisture absorption and maintains the powder's quality.
- Pneumatic or Mechanical Conveying: The powder is conveyed from the storage hopper to the dosing point using either pneumatic systems (air-assisted) or mechanical systems (e.g., screw conveyors). This step ensures the powder is transported without clogging or degradation.
- Dosing and Mixing: The conveyed powder is introduced into the flue gas stream at a controlled rate, where it reacts with sulfur dioxide to form calcium sulfite or calcium sulfate, effectively removing sulfur compounds from the gas.
- System Maintenance: Regular maintenance, including cleaning of components and checking for wear, is essential to ensure the system operates efficiently and prolong its service life.
Benefits of the Desulfurization Sodium Bicarbonate Powder Handling System
Implementing a specialized powder handling system for sodium bicarbonate offers several advantages for industrial desulfurization operations:
- Improved Process Efficiency: Precise dosing and consistent flow control enhance the effectiveness of the desulfurization process, reducing the amount of reagent needed and lowering operational costs.
- Enhanced Safety and Environmental Compliance: Integrated dust suppression and sealed systems minimize environmental impact and ensure workplace safety, helping facilities meet regulatory requirements.
- Reduced Downtime: Robust design and automated controls reduce the likelihood of system failures, minimizing downtime and maintaining consistent production output.
- Customization and Scalability: The system can be tailored to accommodate varying production scales and process requirements, making it suitable for both small-scale and large-scale industrial applications.
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions for desulfurization sodium bicarbonate powder handling, combining advanced technology with expert engineering to meet the evolving needs of industrial desulfurization processes. With a focus on reliability, efficiency, and safety, the company's systems contribute to the sustainable operation of power plants and other industrial facilities.




