For industries dealing with corn cob processing, efficient material conveying is crucial for maintaining production efficiency and ensuring product quality. This article explores the working principle and key features of corn cob material conveying systems, highlighting how advanced engineering solutions from Shandong HeadPowder Engineering Co., Ltd. enhance operational performance in agricultural and food processing applications.
The Working Principle of Corn Cob Material Conveying
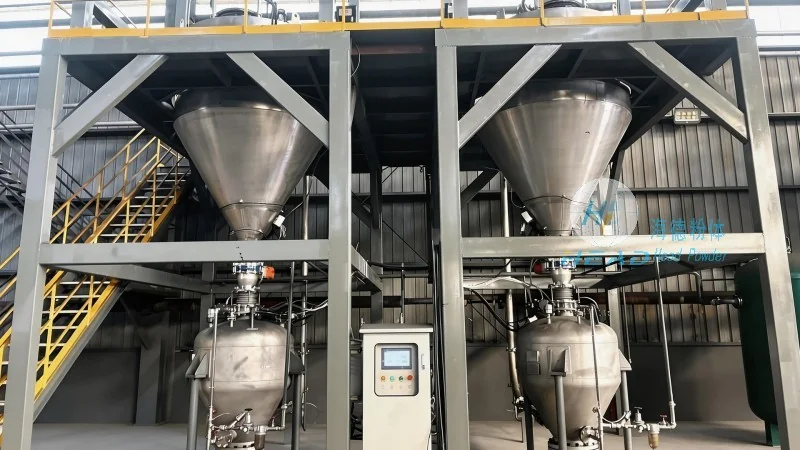
Corn cob material conveying systems typically operate based on mechanical or pneumatic principles, designed to handle the unique characteristics of corn cob material. The process begins with the collection of raw corn cobs, which are then fed into the conveying equipment. In mechanical systems, such as belt conveyors or screw conveyors, the material is transported through a series of rollers or screws that move the cobs along a designated path. Pneumatic systems, on the other hand, utilize air pressure to transport the material through a network of pipes, making them ideal for handling lightweight or dusty corn cob particles. The choice of system depends on factors like material size, moisture content, and the required conveying distance. Shandong HeadPowder Engineering Co., Ltd. specializes in designing customized conveying solutions that optimize these processes, ensuring minimal material loss and consistent flow rates.
Key Features of Corn Cob Material Conveying Systems
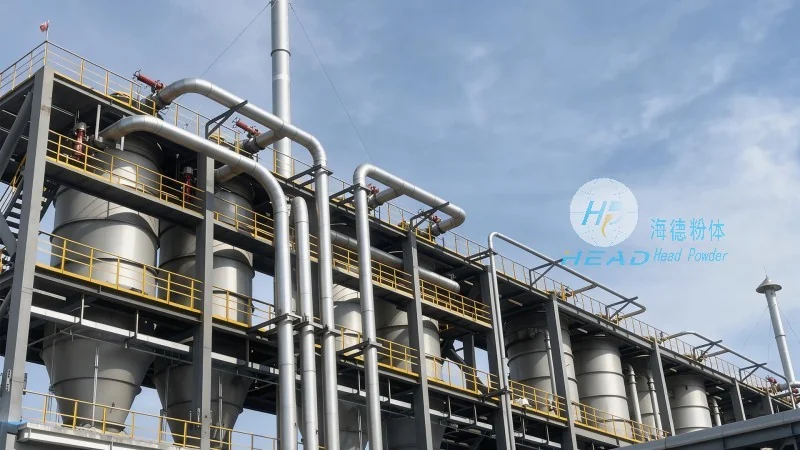
Effective corn cob material conveying systems possess several critical features that contribute to their efficiency and reliability. First, durability is essential, as corn cob material can be abrasive and may cause wear on equipment components. High-quality materials, such as stainless steel or corrosion-resistant alloys, are used in the construction of conveyor components to withstand long-term use. Second, the systems are designed for low maintenance, incorporating easy-to-clean and replaceable parts that reduce downtime. Third, they offer adjustable speed and capacity controls, allowing operators to adapt the conveying rate to varying production demands. Additionally, many modern systems include sensors and monitoring tools to detect blockages or irregularities in real-time, enhancing safety and operational efficiency. The advanced engineering of Shandong HeadPowder Engineering Co., Ltd. ensures that these features are integrated seamlessly, providing users with reliable and cost-effective solutions for corn cob material handling.
Customization and Application in Corn Cob Processing
Shandong HeadPowder Engineering Co., Ltd. understands that each corn cob processing facility has unique requirements. Therefore, their conveying systems are highly customizable to meet specific operational needs. For example, in feed mills or ethanol production plants, the conveying systems may need to handle large volumes of corn cobs while maintaining low moisture content. The company’s engineers work closely with clients to assess their production processes, material characteristics, and space constraints, then design tailored solutions that maximize efficiency and minimize energy consumption. The systems are also designed to be compatible with existing infrastructure, reducing installation time and costs. By focusing on the specific challenges of corn cob material, such as its irregular shape and varying density, the company’s solutions ensure smooth and consistent material flow, which is vital for downstream processing steps like grinding or drying.
Benefits of Using Advanced Conveying Solutions
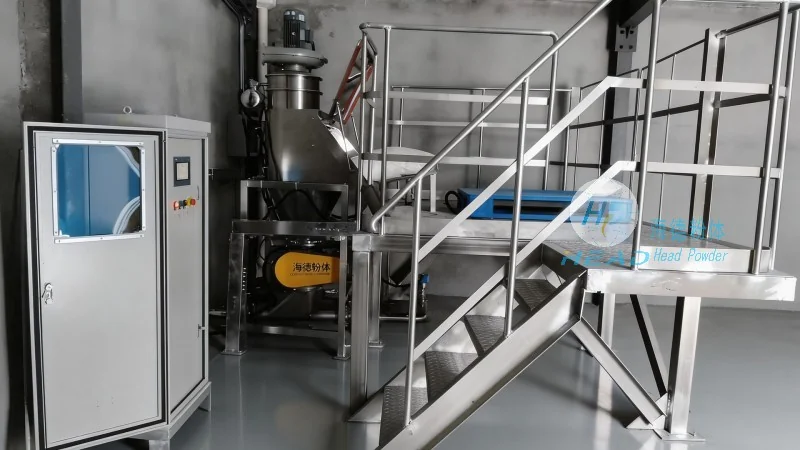
Implementing advanced corn cob material conveying systems from Shandong HeadPowder Engineering Co., Ltd. offers numerous benefits for businesses in the agricultural and food processing sectors. Firstly, improved productivity is achieved through consistent material flow and reduced downtime due to blockages or equipment failure. This leads to higher output and better resource utilization. Secondly, the systems enhance product quality by preventing material contamination and ensuring uniform handling of corn cobs. This is particularly important in applications where the quality of the final product, such as animal feed or biofuel, is directly related to the quality of the raw material. Thirdly, the low maintenance design of the systems reduces operational costs over time, as fewer repairs and replacements are needed. Additionally, the energy-efficient operation of the conveying systems contributes to lower utility bills and a smaller environmental footprint. Overall, the investment in advanced conveying technology from Shandong HeadPowder Engineering Co., Ltd. provides a competitive edge by optimizing production processes and ensuring long-term operational success.




