Coal ash, as a byproduct of coal combustion in thermal power plants, presents significant challenges in handling and transportation due to its fine powder nature and potential environmental impacts. The coal ash powder conveying system developed by Shandong HeadPowder Engineering Co., Ltd. addresses these challenges through an integrated design that ensures efficient, safe, and reliable transport of coal ash from production sites to disposal or utilization facilities. This system is engineered to meet the stringent requirements of modern industrial applications, combining advanced material handling technologies with robust structural components.
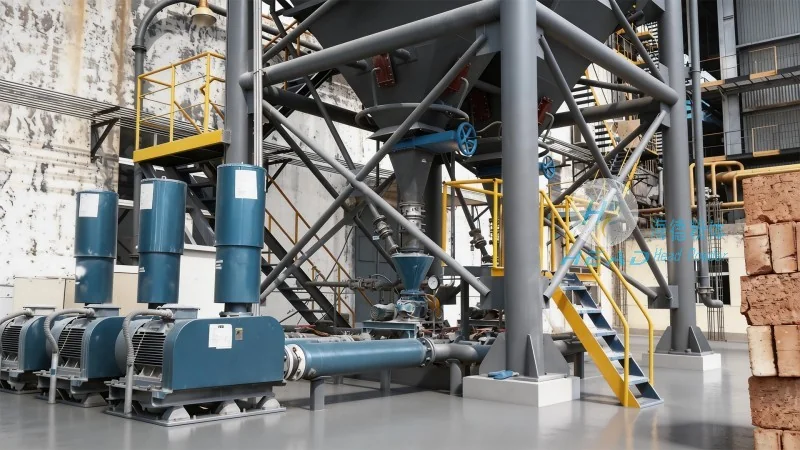
The core components of the coal ash powder conveying system include a series of specialized equipment such as feeders, conveyors, and control units. The feeders are designed to handle the bulk material with minimal dust generation, using adjustable speed mechanisms to regulate the flow rate. The conveyors, typically employing pneumatic or mechanical methods, transport the ash through pipelines or enclosed ducts, minimizing exposure to the environment and ensuring compliance with environmental regulations. Control units, equipped with sensors and automation systems, monitor the system's performance in real-time, providing feedback for optimal operation and preventing operational disruptions.
From a structural perspective, the system is built with durability and efficiency in mind. The material used for the conveying pipelines and components is selected for its resistance to corrosion and abrasion, which are common issues when handling coal ash. The system's modular design allows for easy installation and maintenance, reducing downtime and operational costs. Additionally, the integration of dust collection and filtration systems ensures that the process adheres to air quality standards, contributing to a cleaner and more sustainable operation.
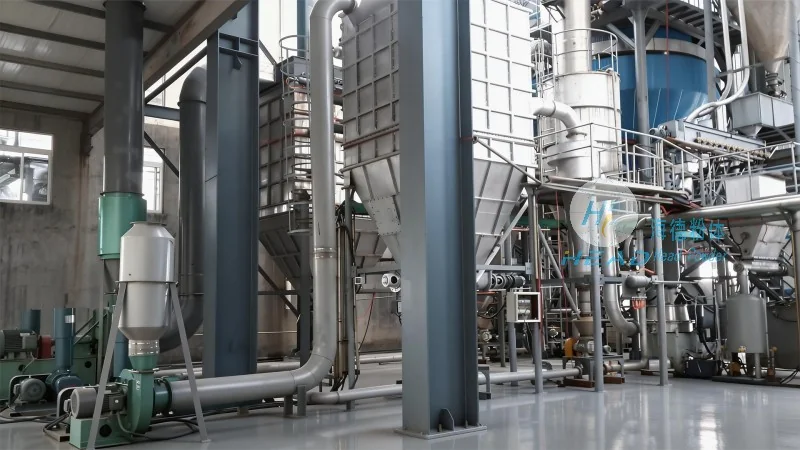
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, has leveraged years of experience to develop this comprehensive solution. The company's expertise in powder handling technology, combined with a commitment to innovation, has resulted in a system that not only meets but exceeds industry standards. By focusing on the specific needs of coal ash transportation, the system offers enhanced safety, reduced environmental impact, and improved operational efficiency for power plants and other industrial facilities.
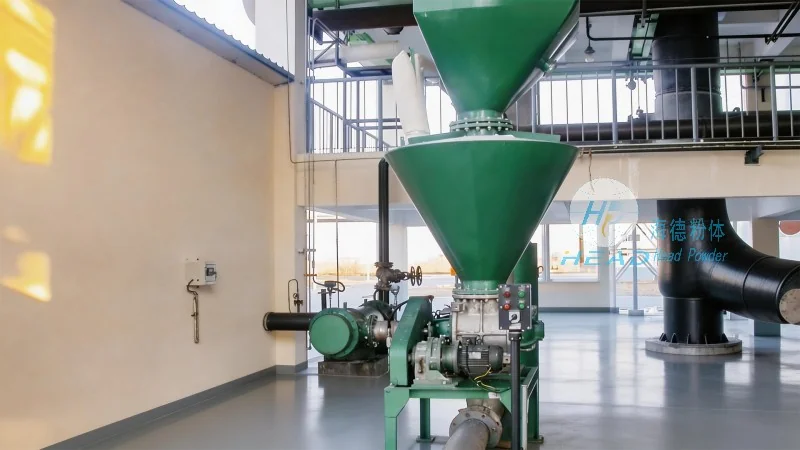
For industrial applications, the coal ash powder conveying system represents a critical advancement in material handling. Its ability to handle large volumes of fine powder while maintaining control over dust and emissions makes it an essential component in modern power generation and waste management. The system's adaptability to various site conditions and operational requirements further enhances its utility, making it a versatile solution for different industrial scenarios.
In conclusion, the coal ash powder conveying system by Shandong HeadPowder Engineering Co., Ltd. exemplifies a well-engineered approach to handling a challenging material. Through its combination of advanced technology, robust design, and environmental considerations, the system provides a reliable and efficient means of transporting coal ash. This solution not only supports the operational needs of power plants but also contributes to sustainable industrial practices, ensuring that the handling of coal ash is conducted in a manner that minimizes negative impacts on the environment and human health.




