For industrial applications involving the handling of hydroxide cobalt powder, the efficiency and reliability of the conveying system are critical factors. This article provides an in-depth overview of the operation process and working principle of the hydroxide cobalt powder conveying system equipment, highlighting key components and their functions. The system is designed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in advanced powder handling solutions. The company, with its headquarters in Shandong, China, has extensive experience in developing customized conveying systems tailored to the unique requirements of various industries, ensuring optimal performance and safety for hydroxide cobalt powder transport.
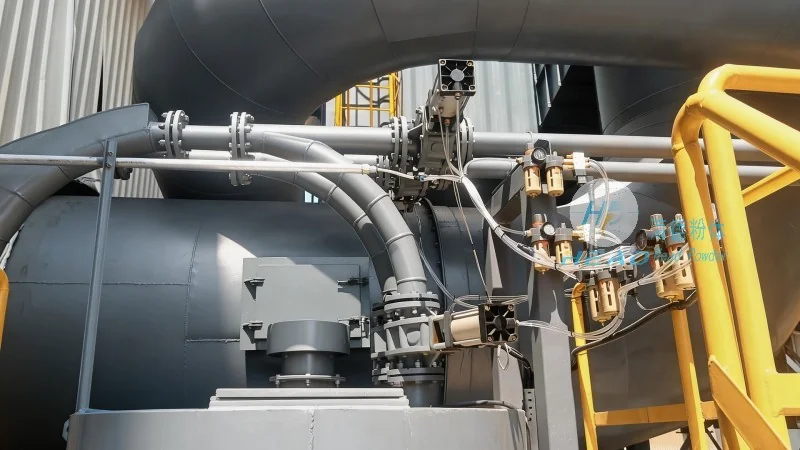
Key Components of the Hydroxide Cobalt Powder Conveying System
The hydroxide cobalt powder conveying system typically consists of several core components that work in tandem to facilitate the movement of the powder. These components include feed hoppers, conveyor belts or screw conveyors, control panels, and dust collection systems. Each component plays a vital role in the overall operation, ensuring that the powder is handled with precision and minimal loss. The feed hopper is responsible for storing and feeding the hydroxide cobalt powder into the system, while the conveyor mechanism (either belt or screw) transports the material through the system. The control panel allows operators to monitor and adjust the system parameters, such as speed and pressure, to optimize performance. The dust collection system is integrated to maintain air quality and prevent contamination, which is crucial for maintaining product purity and compliance with safety standards.
Operation Process of the Hydroxide Cobalt Powder Conveying System
The operation process of the hydroxide cobalt powder conveying system begins with the loading of the hydroxide cobalt powder into the feed hopper. The powder is then released into the conveyor mechanism under controlled conditions. The conveyor system moves the powder through the system, often using a series of interconnected sections to transport it to the desired destination, such as a storage silo or processing unit. During the transport process, the system maintains consistent flow rates and pressure levels to prevent clogging or material degradation. The control panel continuously monitors the system's performance, adjusting parameters as needed to ensure smooth operation. At the end of the conveying process, the powder is discharged into the target container, completing the cycle. The entire operation is designed to be automated, reducing the need for manual intervention and minimizing the risk of human error.
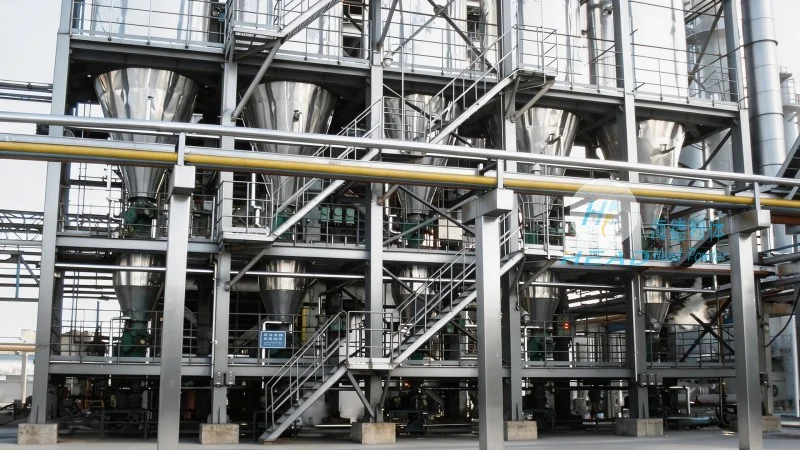
Working Principle of the Hydroxide Cobalt Powder Conveying System
The working principle of the hydroxide cobalt powder conveying system is based on the principles of mechanical transport and material flow. The system utilizes a combination of gravity and mechanical force to move the powder from the feed hopper to the discharge point. The conveyor mechanism, whether a belt or screw, applies a consistent force to the powder, ensuring that it moves through the system without segregation or agglomeration. The control panel regulates the speed and tension of the conveyor, maintaining optimal conditions for the powder's characteristics. The dust collection system operates in parallel, capturing any airborne particles and preventing them from escaping into the environment. This integrated approach ensures that the system operates efficiently while maintaining environmental and safety standards. The system's design also considers the hygroscopic nature of hydroxide cobalt powder, incorporating features such as sealed hoppers and moisture-resistant materials to prevent moisture absorption and maintain product quality.
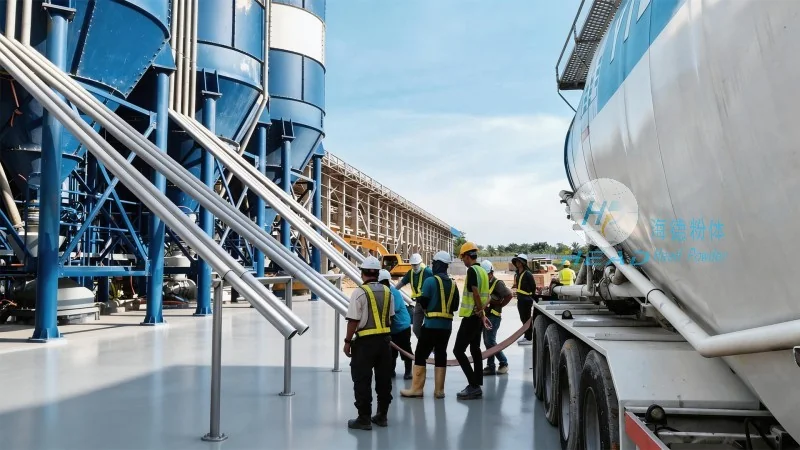
Advantages of the Hydroxide Cobalt Powder Conveying System
The hydroxide cobalt powder conveying system offers several advantages over traditional manual handling methods. Firstly, it enhances operational efficiency by automating the transport process, reducing downtime and increasing throughput. Secondly, it improves product quality by minimizing exposure to air and moisture, which can affect the powder's properties. Thirdly, it enhances safety by reducing the risk of dust explosions and inhalation hazards, as the system is equipped with dust collection and explosion-proof features. Additionally, the system provides precise control over flow rates and pressure, ensuring consistent product delivery to downstream processes. The integration of advanced control technology allows for real-time monitoring and adjustment, further optimizing performance and reducing maintenance costs.
Application Scenarios and Industry Impact
The hydroxide cobalt powder conveying system is widely used in various industrial applications, particularly in the battery manufacturing industry where hydroxide cobalt is a key raw material. The system is essential for the efficient handling of hydroxide cobalt powder from storage to processing units, ensuring a steady supply of material for battery production. In addition to battery manufacturing, the system is also used in other industries such as chemical processing and pharmaceuticals, where precise handling of fine powders is critical. The reliability and efficiency of the system contribute to improved production yields and reduced waste, making it a valuable asset for companies operating in these sectors. The system's design flexibility allows it to be customized to meet the specific requirements of different applications, ensuring optimal performance in diverse industrial settings.




