Principles and Operational Characteristics of Sugar Pneumatic Conveying Systems
Release time:2026-09-19 00:01:29
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
For industries dealing with bulk sugar, efficient and reliable material handling is crucial to maintaining production flow and product quality. The sugar pneumatic conveying system, a key piece of equipment in this sector, operates on principles that ensure safe, effective transport of granular sugar. This article explores the underlying principles of such systems and highlights the specific operational characteristics and working scenarios where they excel.
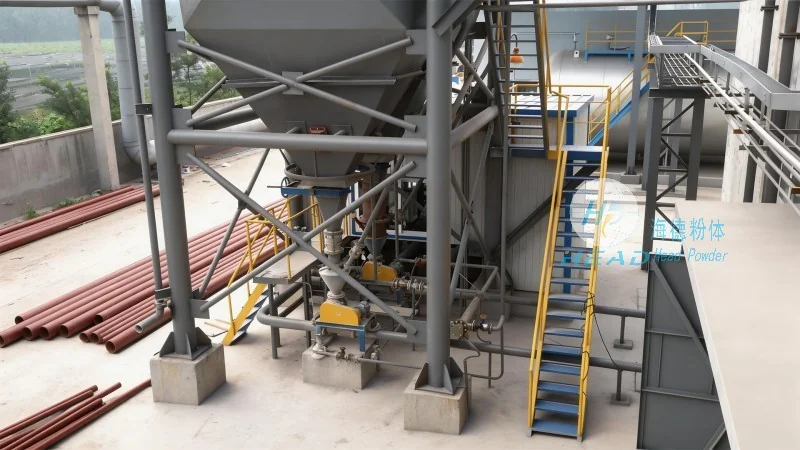
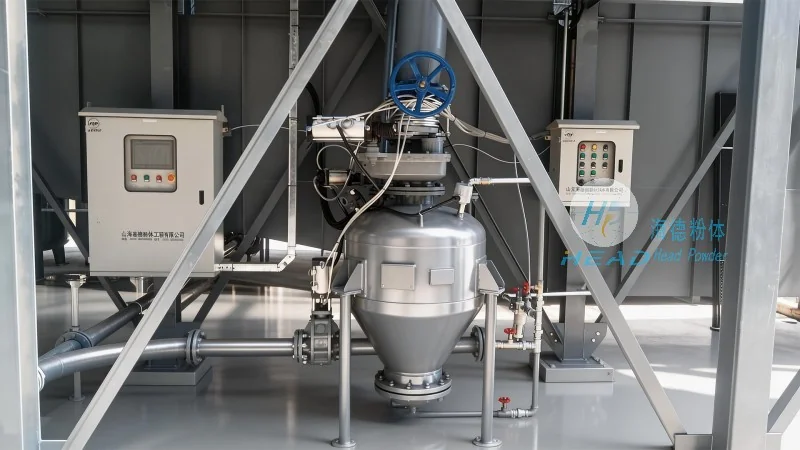
Understanding the Core Principles of Sugar Pneumatic Conveying Systems
The fundamental principle of pneumatic conveying involves using air or other gases to transport solid materials like sugar through a pipeline. In the case of sugar, this method leverages the pressure differential created by a blower or compressor to move the granules. The system typically consists of a hopper, a conveyor line, and a discharge point, with air being introduced to create a flow that carries the sugar particles. This approach eliminates the need for mechanical components like belts or rollers, reducing wear and maintenance requirements while ensuring a hygienic environment suitable for food-grade products.
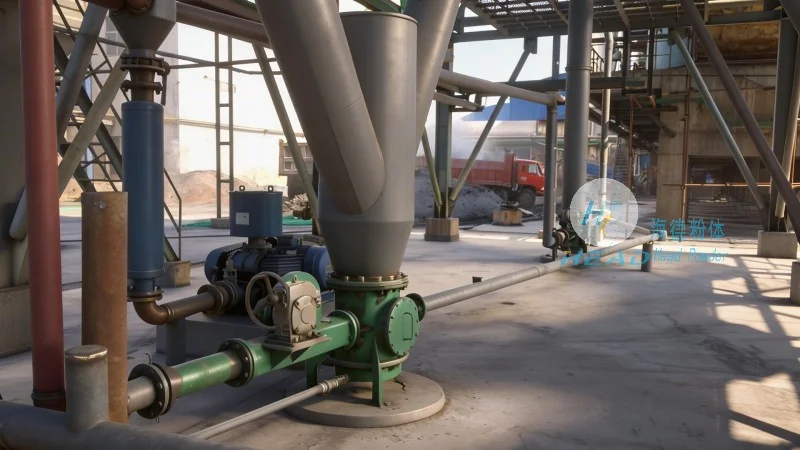
Key Working Scene Characteristics of Sugar Pneumatic Conveying Systems
These systems are particularly well-suited for applications in sugar processing plants, where they are used to move sugar from storage silos to processing lines, or between different stages of production. The ability to handle large volumes of sugar quickly and with minimal human intervention makes them ideal for high-throughput operations. Additionally, the enclosed nature of the system prevents dust and contamination, which is critical for maintaining the purity of the sugar product. In scenarios where space is limited or where a clean, dust-free environment is required, such as in food processing facilities, the pneumatic conveying system offers a superior solution compared to traditional bulk handling methods.
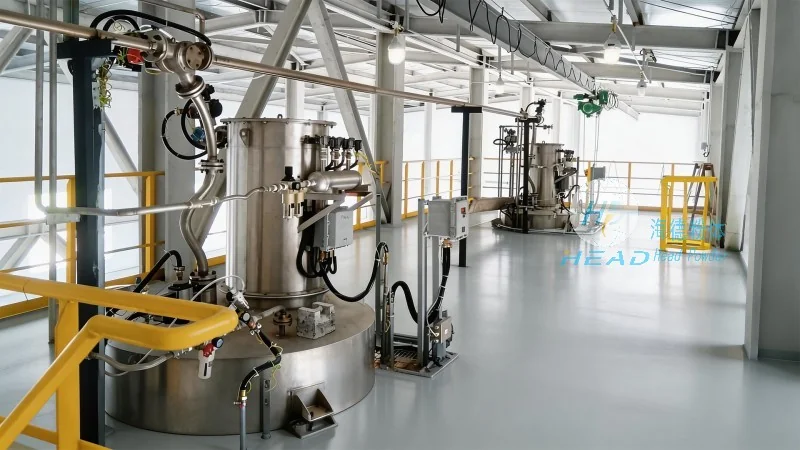
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of bulk material handling equipment, specializes in designing and producing advanced pneumatic conveying systems tailored to the needs of the sugar industry. With a focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable solutions for sugar transport. HeadPowder's systems are engineered to meet the stringent requirements of food processing, ensuring compliance with hygiene standards and operational efficiency. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver cutting-edge technology to global markets.




