Bulk material pneumatic conveying equipment is a critical piece of industrial machinery used for the efficient transport of granular or powder materials. This technology has revolutionized material handling in various industries, including agriculture, food processing, and chemical manufacturing. Understanding its working principle and key features is essential for selecting the right equipment for specific applications.
Working Principle of Pneumatic Conveying Systems
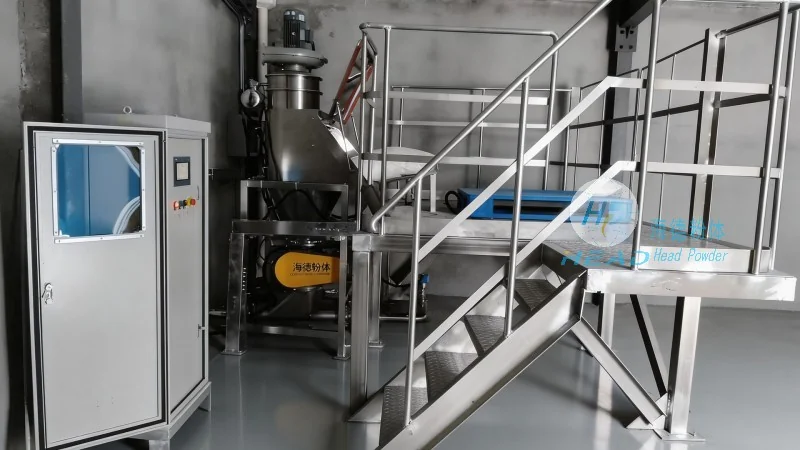
The core working principle of a pneumatic conveying system involves the use of compressed air or gas to transport bulk materials through a pipeline. The process typically begins with the material being fed into a hopper or feeder. From there, the material is drawn into the conveying line by the pressure differential created by the moving air. The air flow, often generated by a blower or compressor, creates a vacuum or pressure that propels the material forward. There are two main types of pneumatic conveying: pressure and vacuum systems. Pressure systems use positive pressure to push material through the line, while vacuum systems use negative pressure to pull material from the source. The choice between these systems depends on factors such as the distance, material characteristics, and the need for dust control.
Key Features of Bulk Material Pneumatic Conveyors
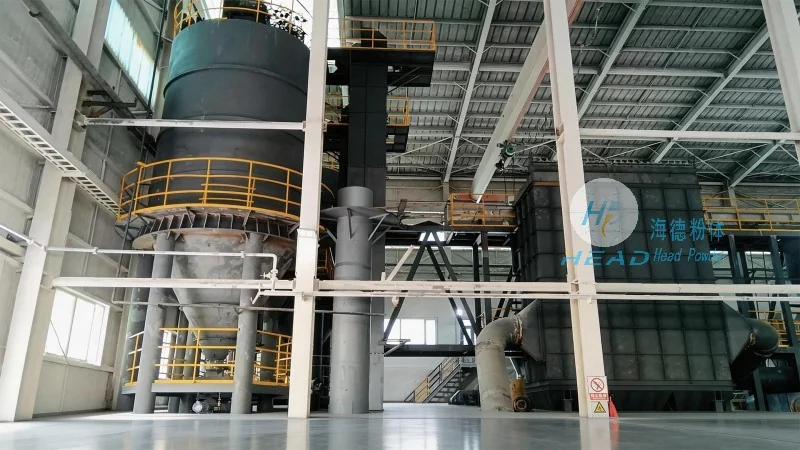
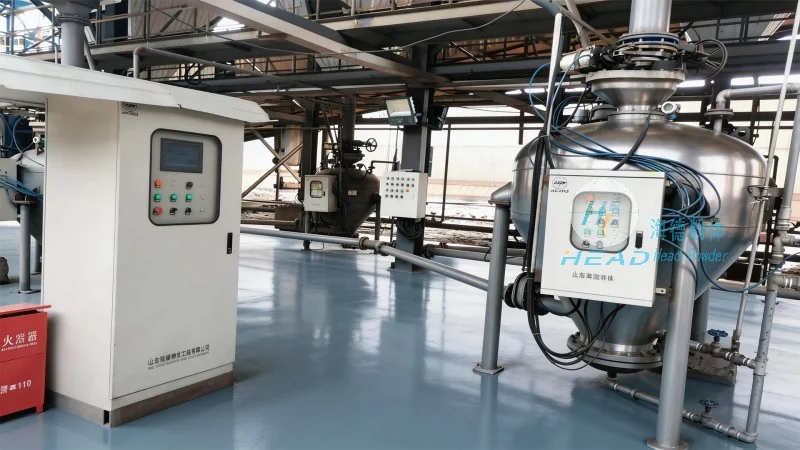
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in designing and manufacturing high-quality pneumatic conveying equipment. Their products are known for several key features that enhance performance and reliability. One of the primary features is the ability to handle a wide range of materials, from fine powders to coarse grains, without causing degradation or contamination. The equipment is also designed for minimal maintenance, with components such as seals and bearings that are built to withstand the abrasive nature of bulk materials. Additionally, the systems are equipped with advanced control mechanisms that allow for precise regulation of flow rates and pressure, ensuring consistent and efficient material transport. Another notable feature is the integration of dust collection and filtration systems, which help maintain a clean and safe working environment by capturing and filtering airborne particles.
Applications and Benefits in Industrial Settings
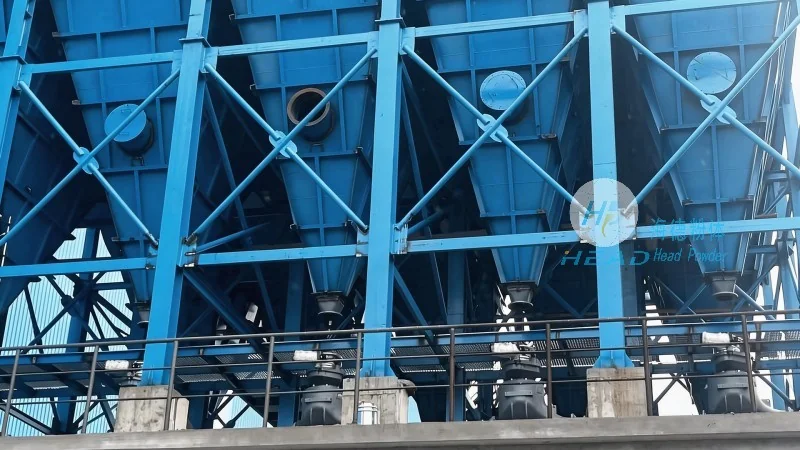
Bulk material pneumatic conveying equipment offers numerous benefits in industrial applications. It provides a dust-free and hygienic method of transporting materials, which is particularly important in food and pharmaceutical industries where contamination control is paramount. The system also allows for the transport of materials over long distances without the need for multiple transfer points, reducing the risk of material loss and improving overall efficiency. Furthermore, the equipment is compact and can be easily integrated into existing production lines, making it a flexible solution for various operational needs. The use of pneumatic conveying also minimizes the need for manual handling, enhancing workplace safety and reducing labor costs.
Conclusion and Company Overview
For businesses seeking reliable and efficient bulk material handling solutions, HeadPowder Engineering Co., Ltd. offers a range of pneumatic conveying systems tailored to meet diverse industrial requirements. With a focus on quality, innovation, and customer satisfaction, the company has established itself as a trusted partner in the industry. Based in Shandong, China, HeadPowder leverages advanced engineering and manufacturing capabilities to deliver products that meet international standards and customer expectations. Whether for short or long-distance material transport, their equipment is designed to provide durable performance and consistent results, ensuring smooth operations in various industrial settings.




