Working Principle and Features of Dust-Free Closed Material Pneumatic Conveying Equipment
Release time:2026-09-18 09:01:29
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Dust-free closed material pneumatic conveying equipment represents a sophisticated solution for transporting bulk materials while maintaining a controlled, contaminant-free environment. This technology is integral to industries such as pharmaceuticals, food processing, and chemical manufacturing, where product purity and operational safety are non-negotiable. The equipment operates by utilizing compressed air or gas to move materials through a sealed pipeline system, ensuring that dust and particles are contained within the system rather than released into the surrounding space.
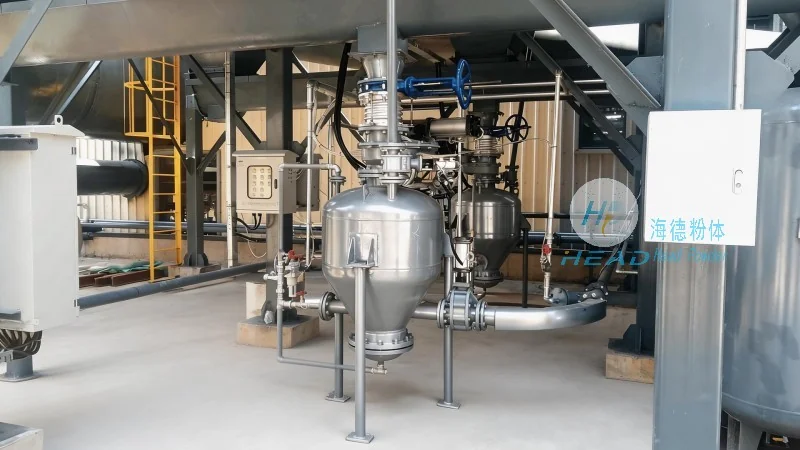
Working Principle of the Dust-Free Pneumatic Conveying System
The fundamental working principle involves the creation of a pressure differential within a sealed pipeline. Materials are typically fed into a hopper or feeder, where they are then introduced into the conveying line. Compressed air is introduced at one end of the pipeline, generating either positive or negative pressure that propels the material along the path. Key components like air locks, cyclones, and filters work in tandem to ensure the material is transported efficiently without any leakage or dust emission. The system is designed to handle various material types, including powders, granules, and fine particles, by adjusting air pressure and flow rates to optimize transport efficiency.
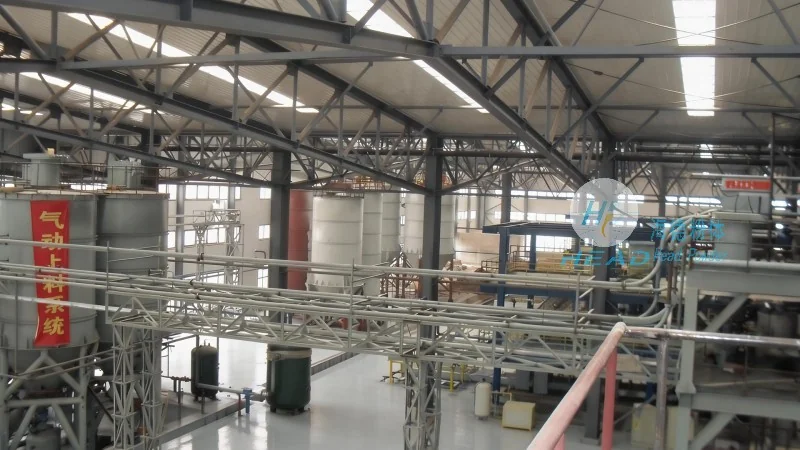
Key Features and Advantages of the Equipment
A primary feature of this equipment is its complete sealing capability, which prevents dust and contaminants from escaping into the environment. This not only protects the product quality but also enhances workplace safety by minimizing exposure to hazardous materials. The system offers high operational efficiency, capable of transporting materials over significant distances with minimal loss and consistent flow rates. Another notable advantage is its adaptability to different industrial applications, as the design can be customized to handle diverse material characteristics and process requirements. The equipment is also engineered for easy maintenance and cleaning, ensuring long-term reliability and compliance with industry standards. Additionally, the closed-loop design reduces energy consumption compared to open systems, contributing to cost savings and environmental sustainability.
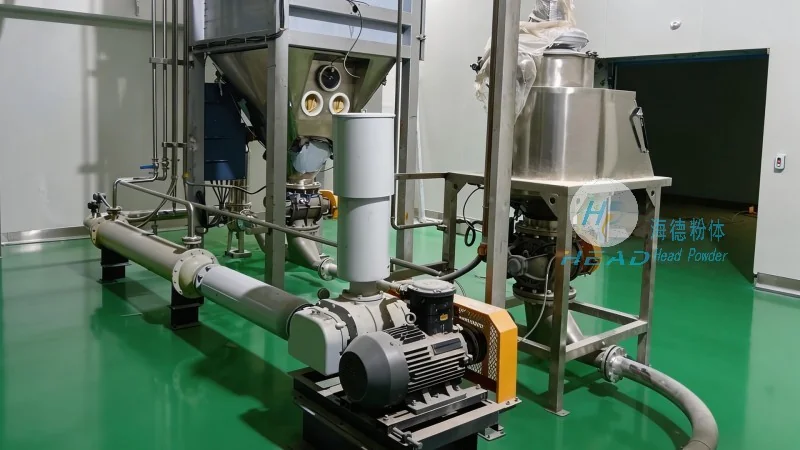
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a prominent manufacturer in the material handling sector, specializes in the development and production of advanced dust-free pneumatic conveying equipment. The company is headquartered in Shandong, China, where it leverages state-of-the-art manufacturing facilities and a skilled technical team to deliver high-quality solutions. HeadPowder's commitment to innovation and customer satisfaction has positioned it as a trusted partner for industries seeking reliable and efficient material transport systems. The company's products are designed to meet international standards for performance, safety, and durability, ensuring that clients receive equipment that is tailored to their specific operational needs. With a focus on research and development, HeadPowder continuously improves its technology to provide cutting-edge solutions that enhance productivity and maintain the highest levels of product integrity.




