For industrial applications involving the handling of ash powders, efficient and reliable material transport is crucial. The ash powder pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., offers a sophisticated solution to meet these demands. This article explores the working principle and key features of such systems, providing insights into their operational efficiency and practical applications.
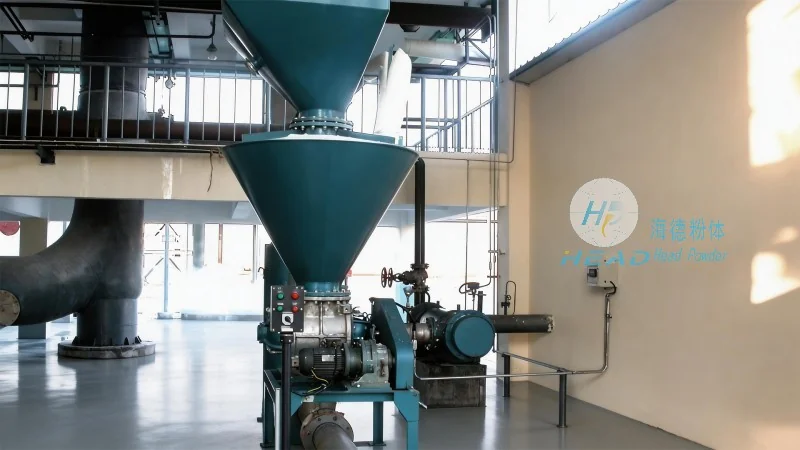
Introduction to Ash Powder Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying equipment. The ash powder pneumatic conveying system is engineered to safely and effectively transport ash powder particles from one location to another within industrial facilities. This technology is particularly valuable in power plants, where large volumes of ash are generated and require systematic handling to ensure environmental compliance and operational efficiency.
Working Principle of the Ash Powder Pneumatic Conveying System
The core mechanism of the ash powder pneumatic conveying system relies on the principles of fluid dynamics and air movement. The system operates by generating a high-pressure air stream, which is then used to transport the ash powder particles through a pipeline network. The process typically involves several key components: a dust collector or hopper to collect the ash powder, a blower or compressor to generate the air pressure, and a pipeline system that connects the source and destination points. As the air flows through the pipeline, it entrains the ash particles, forming a suspension that is propelled forward. The velocity and pressure of the air are carefully controlled to ensure that the ash particles are transported without clogging or degradation. The system may also include features such as cyclone separators or filters to separate the ash from the air at the receiving end, allowing for clean air discharge and material recovery.
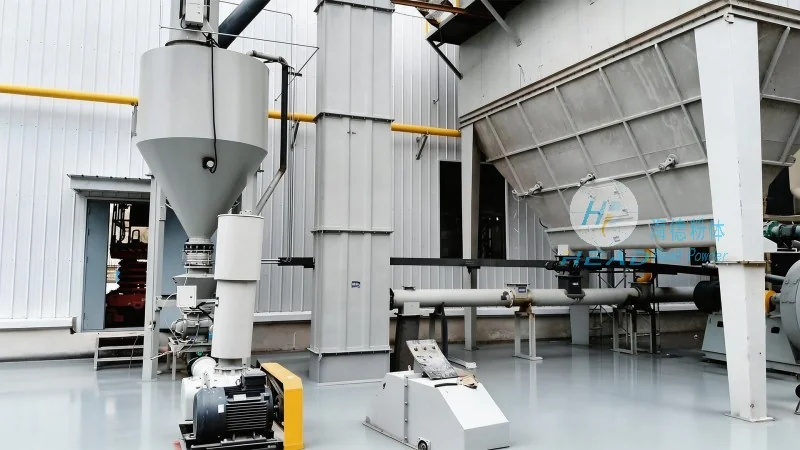
Key Features of the Ash Powder Pneumatic Conveying System
The ash powder pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. incorporates several distinctive features that enhance its performance and usability. Firstly, the system is designed for high efficiency in material transport, with the ability to handle large volumes of ash powder at a consistent rate. This ensures that the operational downtime is minimized, as the system can maintain a steady flow of material without interruptions. Secondly, the system offers excellent flexibility in terms of layout and configuration. The modular design allows for easy integration into existing industrial setups, and the pipeline can be customized to fit the specific geometry of the facility. This adaptability is crucial for power plants and other industrial sites where space constraints and existing infrastructure may vary.
Thirdly, the system prioritizes safety and environmental compliance. The use of enclosed pipelines and filtration systems prevents the release of ash particles into the environment, reducing the risk of air pollution and health hazards. Additionally, the system is equipped with safety valves and pressure relief mechanisms to prevent over-pressurization and potential accidents. The design also minimizes the need for manual handling of ash powders, which can be hazardous due to dust inhalation and skin irritation. By automating the transport process, the system enhances workplace safety and reduces the exposure of personnel to harmful materials.
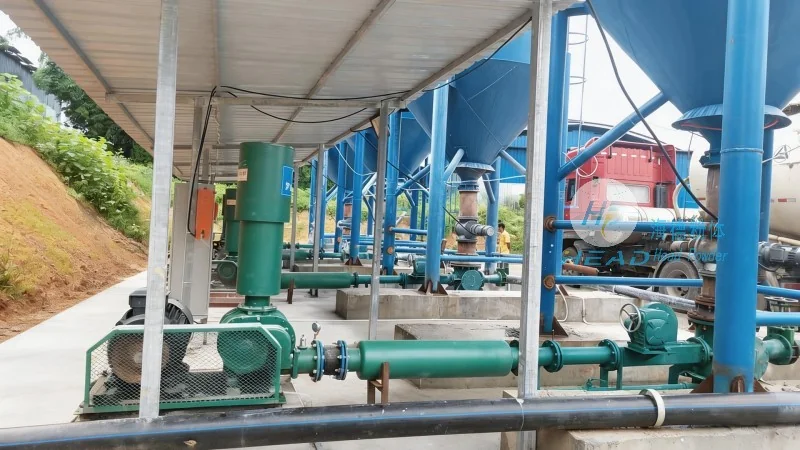
Operational Advantages and Applications
The ash powder pneumatic conveying system provides several operational advantages that make it an attractive choice for industrial applications. One of the primary benefits is the reduction in material handling costs. By eliminating the need for manual or mechanical conveyors, such as belt conveyors or bucket elevators, the system reduces labor costs and maintenance expenses. The enclosed pipeline design also minimizes material loss and contamination, ensuring that the ash powder remains in a clean and usable state throughout the transport process. This is particularly important for power plants, where the ash may be repurposed as a raw material for cement production or other industrial applications.
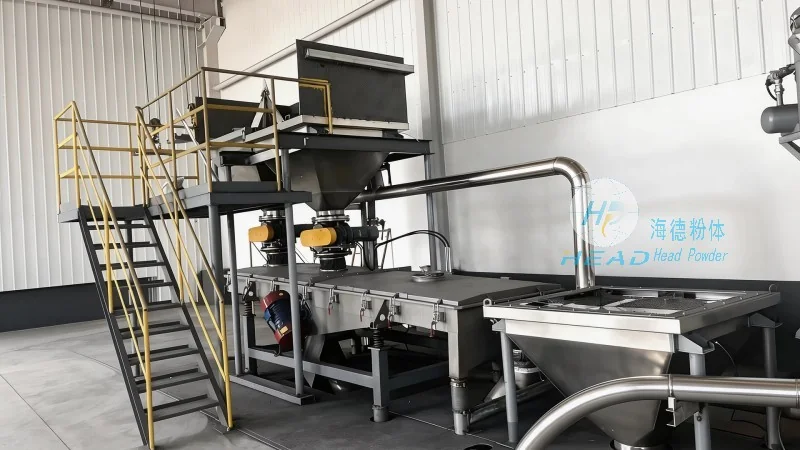
Furthermore, the system offers improved process control and monitoring capabilities. Modern pneumatic conveying systems are equipped with sensors and control panels that allow operators to monitor the flow rate, pressure, and temperature of the system in real-time. This enables proactive maintenance and troubleshooting, reducing the likelihood of system failures and downtime. The data collected from these sensors can also be used to optimize the system's performance over time, leading to increased efficiency and cost savings.
Conclusion
In conclusion, the ash powder pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated and efficient solution for the transport of ash powders in industrial settings. By leveraging the principles of pneumatic conveying, the system offers high efficiency, flexibility, and safety features that address the challenges of handling large volumes of ash. The integration of advanced technology and careful design ensures that the system meets the demanding requirements of power plants and other industrial facilities, contributing to improved operational performance and environmental compliance. As a leading manufacturer based in Shandong, China, HeadPowder continues to innovate in the field of pneumatic conveying equipment, providing reliable solutions for the ever-evolving needs of the industrial sector.




