Working Principle and Features of Recycled Sand Material Handling Equipment
Release time:2026-09-17 20:01:24
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Recycled sand, also known as reclaimed sand, is a critical component in modern construction and manufacturing processes. As the demand for sustainable building materials grows, the efficient handling and transportation of recycled sand have become essential. This article explores the working principle and key features of specialized equipment designed for this purpose, highlighting how such machinery enhances operational efficiency and supports environmental sustainability.
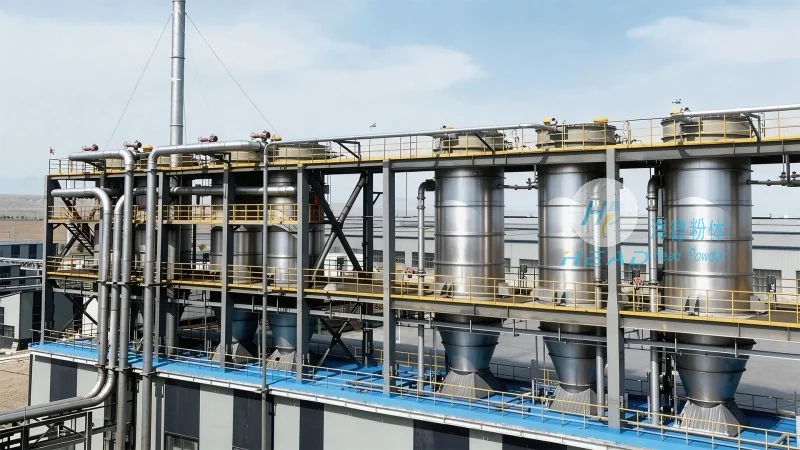
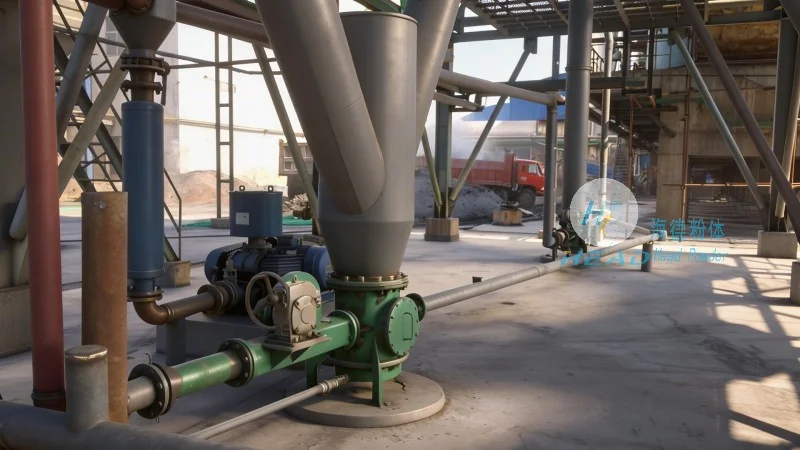
Working Principle of Recycled Sand Material Handling Equipment
The core function of recycled sand material handling equipment is to transport sand that has been processed from construction waste or industrial byproducts. The process typically involves several integrated components working in sequence. First, the sand is collected and fed into a hopper or storage bin. From there, a conveyor system, often equipped with specialized belts or buckets, moves the material through the handling process. Many systems incorporate a screening or sorting mechanism to ensure the sand meets quality standards before transport. The equipment may also include a dust control system to maintain air quality and protect the environment. The entire operation is driven by electric motors or hydraulic systems, which provide the necessary power to move the material from the source to the destination, such as a storage silo or a mixing plant. This integrated approach ensures that the recycled sand is handled safely and efficiently, minimizing downtime and maximizing throughput.
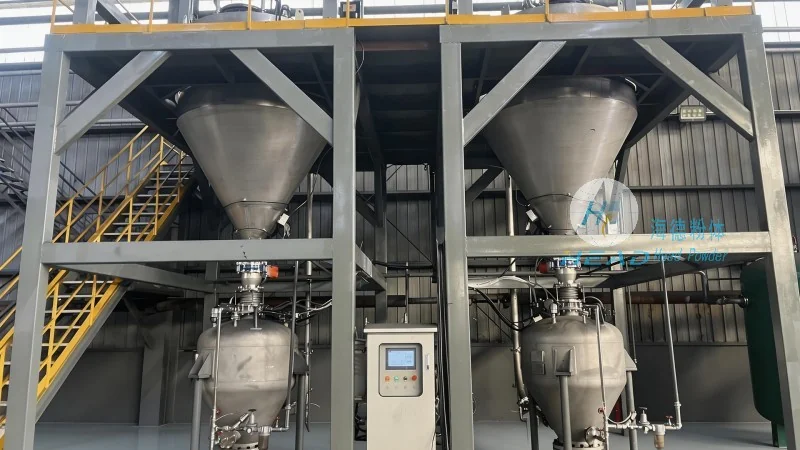
Key Features of Recycled Sand Material Handling Equipment
Specialized equipment for recycled sand material handling offers several advantages that make it indispensable in industrial applications. One of the primary features is its high capacity and durability, designed to handle large volumes of sand with minimal maintenance. The equipment is often constructed from corrosion-resistant materials, such as stainless steel or high-grade alloys, which ensures longevity even in harsh environments. Another critical feature is the advanced control systems, which allow for precise regulation of the material flow, preventing overloading or underloading of the conveyor. The equipment also includes safety features, such as emergency stop buttons and overload protection, to ensure operator safety and equipment longevity. Additionally, many models are equipped with automated monitoring systems that track performance metrics, enabling real-time adjustments to optimize efficiency. These features collectively contribute to a reliable and efficient handling solution for recycled sand, supporting both productivity and sustainability goals.
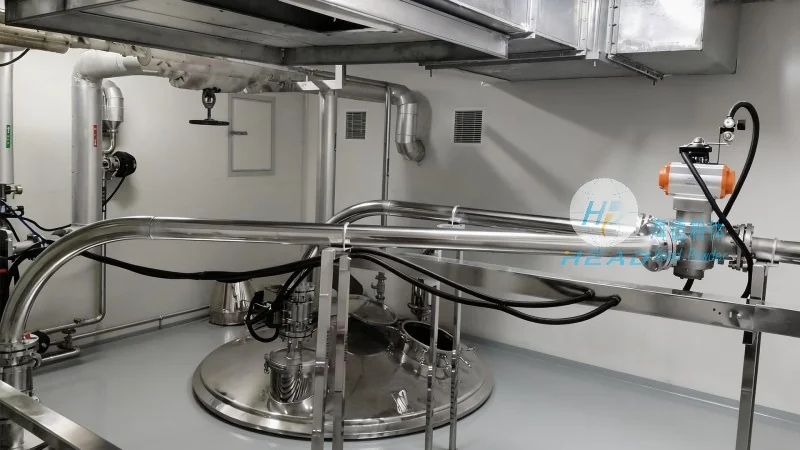
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized material handling equipment for the construction and recycling industries. With a focus on innovation and quality, the company has developed advanced solutions tailored to the unique challenges of recycled sand processing. Based in Shandong, China, headpowder leverages years of industry experience to deliver equipment that meets the highest standards of performance and reliability. The company’s commitment to sustainability aligns with global trends, making it a trusted partner for businesses seeking to enhance their recycling operations and reduce environmental impact. By combining cutting-edge technology with rigorous testing, headpowder ensures that its equipment delivers consistent results, helping clients achieve their operational and environmental objectives.




