HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and supply of advanced solid powder pneumatic conveying systems. These systems are engineered to efficiently transport bulk solid materials such as powders, granules, and fine particles through a pressurized or vacuum environment using air or other gases. The core principle of pneumatic conveying involves the creation of a flow channel where the solid particles are suspended and propelled by the moving gas stream, enabling seamless material transfer across various industrial applications.
Core Principles of Pneumatic Conveying Systems
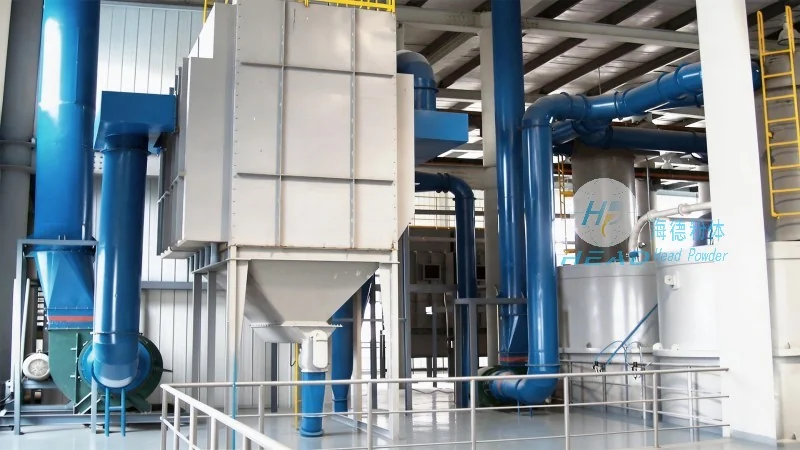
The fundamental principle of solid powder pneumatic conveying systems is the suspension and transport of solid particles within a gas stream. This process relies on the interaction between the gas velocity and the particle characteristics, including size, density, and shape. The system typically operates under either positive pressure (pressure conveying) or negative pressure (vacuum conveying), each offering distinct advantages based on the material being handled and the layout of the conveying line.
Pressure conveying systems use compressed air to push the material through the pipeline, making them suitable for long-distance or high-rise applications where a continuous flow is required. The pressure is maintained by a blower or compressor, ensuring the material moves efficiently without clogging. In contrast, vacuum conveying systems draw material into the system using a vacuum pump, which is ideal for handling fine powders or materials that are sensitive to pressure changes. This method is often used for short-distance or vertical transport where the material needs to be collected from multiple points.
Key Components and Their Functions
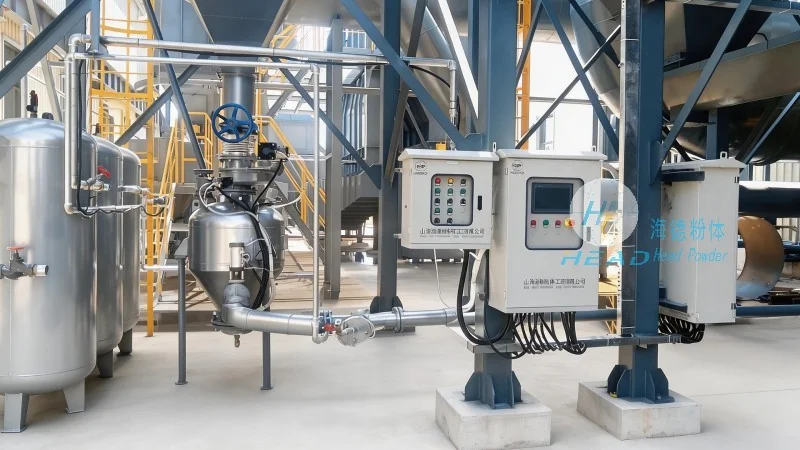
Modern solid powder pneumatic conveying systems consist of several critical components that work in tandem to ensure reliable operation. These include the material feed hopper, which stores and feeds the powder into the system; the air supply unit (blower or compressor), which generates the necessary pressure or vacuum; the conveying line, which transports the material; and the control system, which monitors and adjusts the flow parameters. Additionally, components such as rotary valves, filters, and cyclones are integrated to manage material flow, prevent dust emissions, and ensure the system operates within safe and efficient parameters.
Application Scenarios and Industry Use Cases
The versatility of solid powder pneumatic conveying systems makes them indispensable in a wide range of industries. In the pharmaceutical sector, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination, ensuring compliance with stringent regulatory standards. The food and beverage industry utilizes pneumatic conveying for handling powders like sugar, flour, and spices, maintaining hygiene and preventing cross-contamination. In the chemical industry, they are employed to transport reactive powders and fine chemicals, where dust control and explosion-proof designs are critical for safety. The mining and mineral processing sector also benefits from these systems, as they efficiently convey raw materials and byproducts over long distances with minimal maintenance.
Advantages of Pneumatic Conveying Over Traditional Methods
Compared to traditional mechanical conveying methods like screw conveyors or belt conveyors, solid powder pneumatic conveying systems offer several advantages. One of the most significant benefits is the ability to handle a wide variety of materials, including those that are abrasive, sticky, or prone to caking. The enclosed system also reduces dust emissions, improving workplace safety and environmental compliance. Additionally, pneumatic conveying can be more flexible in terms of layout, allowing for vertical and horizontal transport in a single system, which simplifies the overall plant design. The system's ability to operate continuously without the need for frequent maintenance also contributes to cost savings and increased productivity.
Customization and Scalability for Diverse Needs
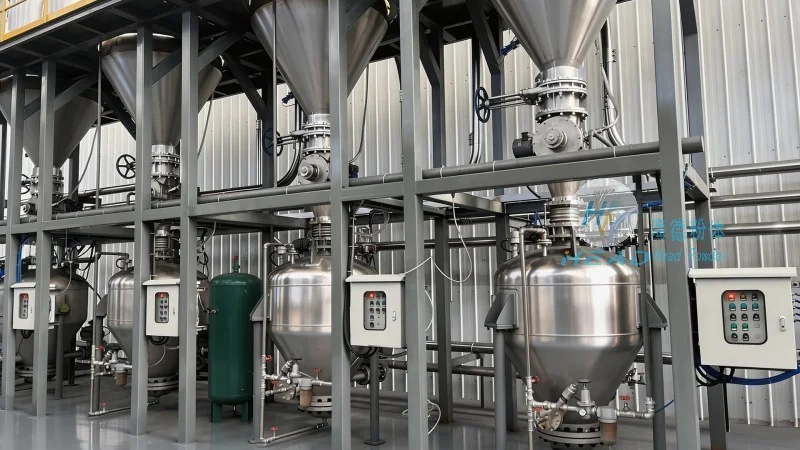
HeadPowder understands that each industrial application has unique requirements. Therefore, their solid powder pneumatic conveying systems are designed to be highly customizable. Clients can choose from different types of conveying lines, such as dilute phase or dense phase systems, based on the material's properties and the required flow rate. The company also offers scalable solutions, from small-scale systems for laboratory use to large-scale industrial systems capable of handling thousands of tons of material per day. This flexibility ensures that the system can adapt to the evolving needs of the client's operations, providing long-term value and reliability.
Quality Assurance and Technical Support
As a manufacturer based in Shandong, China, HeadPowder adheres to strict quality control standards to ensure the reliability and performance of their pneumatic conveying systems. Each system undergoes rigorous testing and validation before delivery, including pressure testing, flow rate verification, and material compatibility checks. The company also provides comprehensive technical support, including installation guidance, maintenance training, and on-site troubleshooting. This commitment to quality and customer service has made HeadPowder a trusted partner for industries worldwide, delivering efficient and durable solutions for solid powder handling.




