

[W]Working Principle and Features of Dust Collector Ash Pneumatic Conveying Systems
For industrial applications that require efficient handling of dust collector ash, pneumatic conveying systems offer a reliable and effective solution. This article delves into the working principle and key features of such systems, providing insights into how they operate and the advantages they bring to material transport processes.
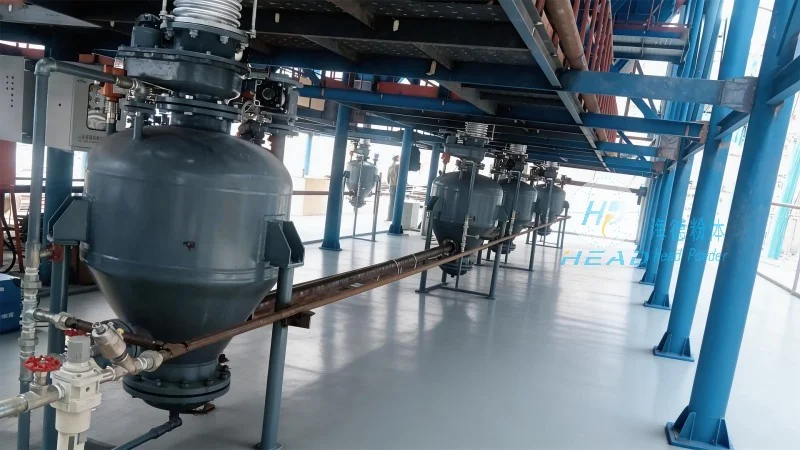
Introduction to Dust Collector Ash Pneumatic Conveying Systems
Dust collector ash, often generated from industrial processes like cement production, power generation, or metal smelting, poses challenges in terms of handling and disposal. Traditional methods such as manual shoveling or mechanical conveyors may be inefficient, costly, and pose health risks due to dust exposure. Pneumatic conveying systems provide a closed-loop solution that addresses these issues by transporting ash through a network of pipes using compressed air or other gases.
Working Principle of Pneumatic Conveying Lines
The core working principle of a dust collector ash pneumatic conveying system involves the use of a blower or compressor to generate airflow within a pipeline. The system typically consists of several components, including a hopper for ash storage, a feeder to control the flow rate, a conveying line (often made of stainless steel or other corrosion-resistant materials), and a receiver for the transported material. The process begins when ash is discharged from the hopper into the feeder, which then feeds the material into the conveying line. As compressed air is introduced, it creates a low-pressure zone that draws the ash particles into the pipeline, where they are carried to the destination receiver. The air and ash mixture then passes through a separator, where the air is released and the ash is collected in the receiver. This continuous cycle ensures efficient and safe transport of dust collector ash.
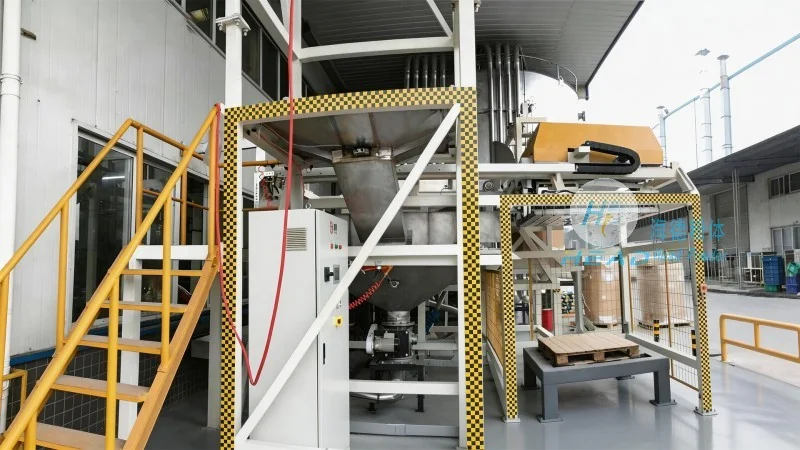
Key Features and Advantages of Pneumatic Conveying Systems
Several distinct features make pneumatic conveying systems particularly suitable for handling dust collector ash:
Closed-Loop Operation: The system operates in a closed environment, minimizing dust emissions and preventing contamination of the surrounding air. This is crucial for maintaining a safe working environment and complying with environmental regulations.
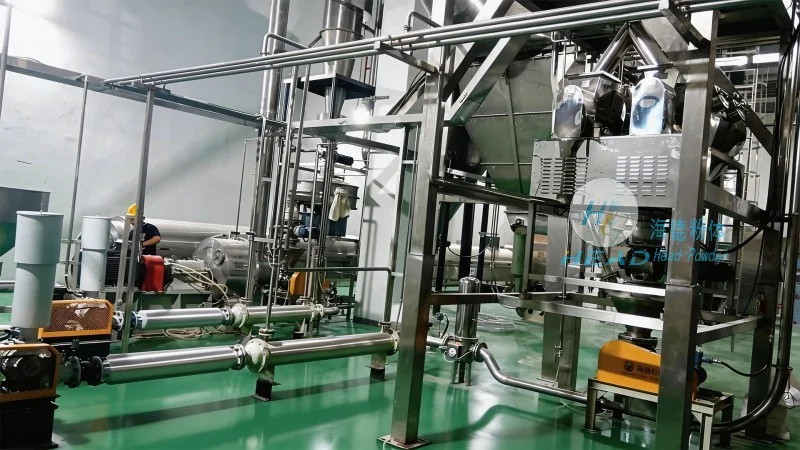
Efficient Material Transport: By using compressed air, the system can transport ash over significant distances with minimal energy consumption compared to traditional mechanical conveyors. The ability to handle both fine and coarse particles makes it versatile for various industrial applications.
Low Maintenance Requirements: Pneumatic conveying systems typically have fewer moving parts compared to mechanical conveyors, reducing the need for frequent maintenance and lowering long-term operational costs.
Customizable Design: Systems can be tailored to specific industrial needs, including varying pipe sizes, pressure levels, and material flow rates. This flexibility allows for integration into existing production lines without major modifications.
Applications and Industries
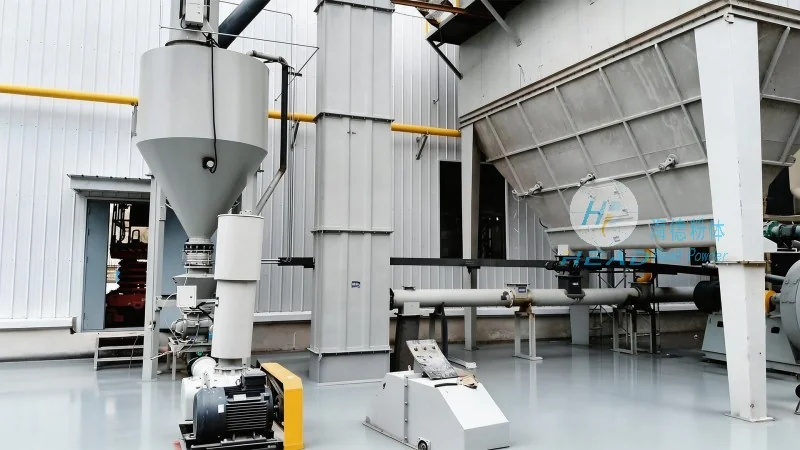
Dust collector ash pneumatic conveying systems are widely used across various industries where ash handling is a critical process. These include cement manufacturing, thermal power plants, steel production, and recycling facilities. The systems are particularly beneficial in applications where dust control and material transport efficiency are paramount.
Conclusion
In summary, dust collector ash pneumatic conveying systems offer an efficient, safe, and environmentally friendly solution for transporting ash from dust collectors. By understanding the working principle and leveraging the key features of these systems, industries can enhance their material handling processes, reduce operational costs, and improve overall safety. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying solutions tailored to meet the unique needs of industrial clients in China.