Calcium nitrite, a critical chemical compound utilized in industrial sectors such as water treatment, food preservation, and corrosion control, necessitates efficient and reliable handling systems for safe and effective transport. The pneumatic conveying equipment designed for calcium nitrite provides a solution that integrates advanced technology with robust engineering to meet modern industrial demands. Manufactured by Shandong HeadPowder Engineering Co., Ltd., a leading entity in the field, this equipment is engineered to deliver high performance and durability in handling calcium nitrite under diverse operational conditions.
Key Components and Structural Design of the Pneumatic Conveying System
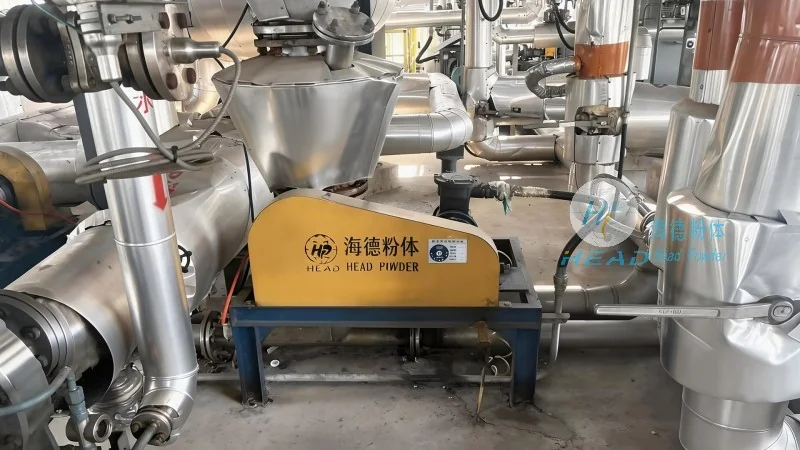
The pneumatic conveying system for calcium nitrite comprises several essential components that operate in unison to achieve efficient material transport. Primary components include the hopper, which serves as the storage and feeding unit where calcium nitrite is loaded; the air compressor or blower, responsible for generating the air pressure required to move the material; the conveying pipeline, which transports the material from the hopper to the discharge point; and the control system, which monitors and regulates material and air flow. Each component is engineered with precision to ensure optimal performance and minimal maintenance, reflecting the high standards of engineering upheld by Shandong HeadPowder Engineering Co., Ltd.
Working Principle of the Pneumatic Conveying Process
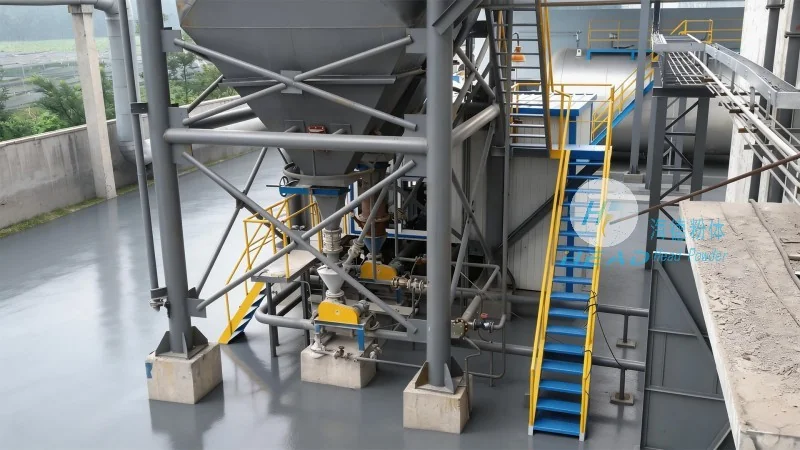
The operation of the calcium nitrite pneumatic conveying equipment is based on the principle of pneumatic transport, where material particles are suspended and carried by a stream of air within the conveying pipeline. The process initiates with calcium nitrite being fed from the hopper into the pipeline via a feeder mechanism. Simultaneously, the air compressor supplies a high-pressure air stream that creates a flow within the pipeline. As the air flows, it lifts and suspends the calcium nitrite particles, moving them along the pipeline to the discharge point. The air speed and pressure are carefully controlled to ensure material is conveyed without degradation or blockage. The system also incorporates air filtration and moisture control features to maintain calcium nitrite quality during transport. This working principle, combined with robust design, ensures reliable and efficient handling of calcium nitrite, critical for maintaining product quality and operational efficiency in industrial applications.
Operation Process: Step-by-Step Execution
The operation of the calcium nitrite pneumatic conveying system follows a systematic process to ensure smooth, continuous material transport. The first step involves loading calcium nitrite into the hopper, where it is stored until needed. The hopper is equipped with a level indicator to monitor material levels, ensuring the feeder operates effectively. Once loaded, the feeder mechanism begins, feeding calcium nitrite into the conveying pipeline at a controlled rate. Simultaneously, the air compressor activates, generating the necessary air pressure to initiate the conveying process. The air flow is adjusted to maintain consistent velocity, crucial for preventing material deposition or blockage in the pipeline. As material is conveyed, the system continuously monitors flow rate and pressure, making real-time adjustments for optimal performance. The discharge point is designed to handle material efficiently, ensuring delivery to the next process stage without loss or contamination. The entire operation is controlled by a sophisticated control system integrating all components, providing a seamless and reliable transport process. This step-by-step operation, as implemented by Shandong HeadPowder Engineering Co., Ltd., ensures calcium nitrite is handled safely and efficiently, meeting high industrial standards.
Advantages and Benefits of the Pneumatic Conveying Equipment
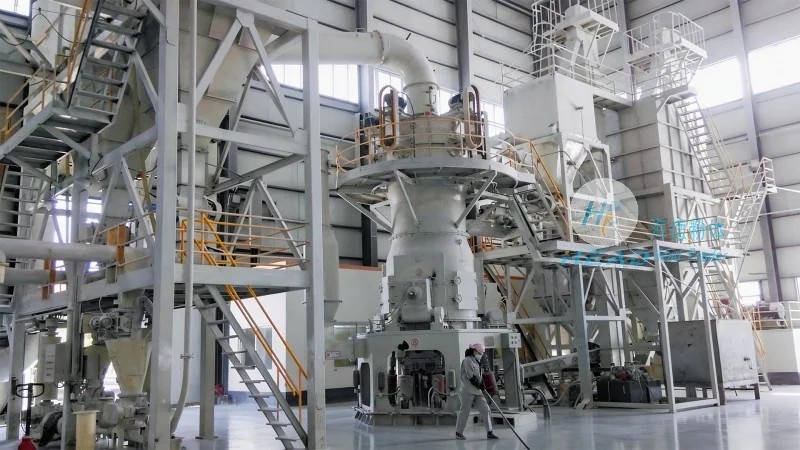
The pneumatic conveying equipment for calcium nitrite offers several advantages, making it a preferred choice for industrial applications. A key benefit is handling calcium nitrite in a dust-free environment, essential for product quality and worker safety. The system provides continuous, uniform material flow, reducing degradation or segregation risks. It is also compact and space-efficient, suitable for limited installations. Air use as the conveying medium minimizes mechanical wear from belts or screws. The robust construction ensures long-term durability and low maintenance costs, offering a cost-effective solution. These advantages, combined with high performance and reliability, make it ideal for industries requiring efficient calcium nitrite transport.




