

What is a Mineral Powder Pneumatic Conveying System? Exploring Design Principles
A mineral powder pneumatic conveying system is a specialized industrial equipment designed to transport dry powders, such as minerals, through a pipeline using air pressure. This technology is widely used in various industries, including mining, chemical processing, and food production, to efficiently move bulk materials from one location to another without the need for mechanical components like belts or buckets. The system operates by creating a pressure differential that propels the powder particles through the pipeline, making it an ideal solution for applications where traditional conveying methods may be impractical or inefficient.
Key Components of a Pneumatic Conveying System
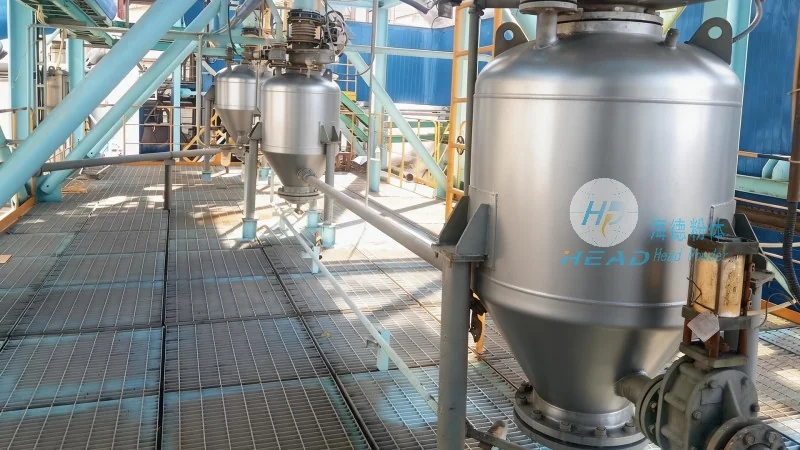
The core components of a mineral powder pneumatic conveying system include the material feed hopper, the air compressor, the conveying pipeline, the control valves, and the discharge hopper. The feed hopper is responsible for storing and feeding the powder into the system, while the air compressor generates the necessary air pressure to move the material. The pipeline, typically made of stainless steel or other corrosion-resistant materials, transports the powder and air mixture. Control valves regulate the flow of air and material, ensuring smooth operation and preventing blockages. The discharge hopper collects the material at the end of the pipeline, completing the conveying process.
Design Principles and Operational Mechanisms
The design of a mineral powder pneumatic conveying system is based on several fundamental principles to ensure optimal performance and efficiency. One of the primary principles is the use of air as the conveying medium, which allows for the transportation of dry powders without the need for additional mechanical components. The system operates by creating a pressure difference between the inlet and outlet of the pipeline. At the inlet, the air is compressed and mixed with the powder, forming a suspension that is then propelled through the pipeline by the pressure differential. The velocity of the air and the size of the powder particles are critical factors in determining the system's efficiency, as they affect the flow rate and the risk of blockages. Additionally, the system's design considers factors such as the material's properties, including its density, moisture content, and particle size distribution, to ensure that the conveying process is effective and safe.
Advantages of Pneumatic Conveying for Mineral Powders
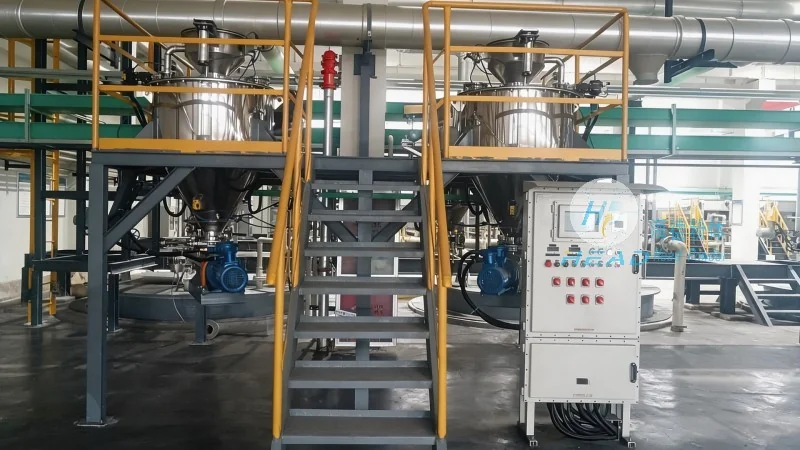
Compared to traditional conveying methods like belt conveyors or bucket elevators, pneumatic conveying systems offer several advantages for transporting mineral powders. One of the key benefits is the ability to handle a wide range of powder types, including fine and abrasive materials, without causing wear and tear on the equipment. The system also provides a more hygienic and dust-free environment, which is particularly important in industries such as food and pharmaceuticals where contamination must be minimized. Furthermore, pneumatic conveying systems are more flexible in terms of layout, as they can be installed in various configurations, including vertical, horizontal, or a combination of both, to suit the specific requirements of the application. This flexibility allows for the optimization of the conveying process and the reduction of material handling costs.
Applications and Industry Use Cases
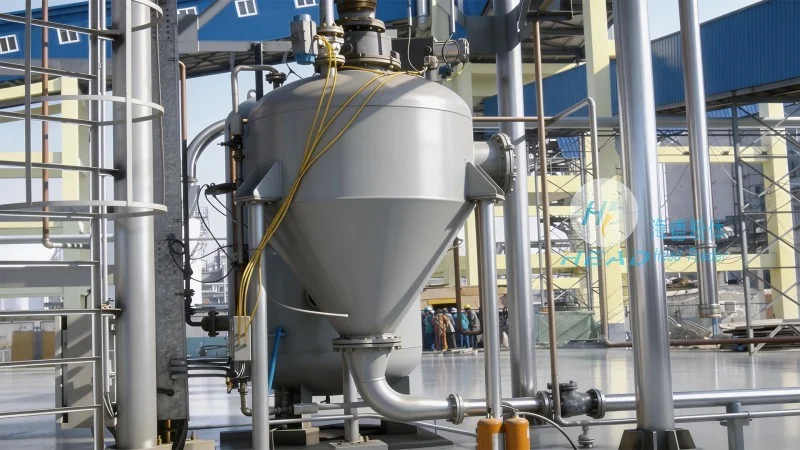
Mineral powder pneumatic conveying systems are used in a variety of applications across different industries. In the mining industry, they are used to transport crushed minerals from processing plants to storage facilities or for further processing. In the chemical industry, they are employed to move raw materials and finished products between processing units, ensuring a continuous and efficient production flow. The food industry also utilizes pneumatic conveying systems to transport ingredients such as flour, sugar, and spices, maintaining the quality and hygiene of the products. Additionally, in the pharmaceutical industry, these systems are used to handle powders that require strict contamination control, ensuring that the final products meet regulatory standards.
Customization and Scalability
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of industrial conveying equipment, offers customized pneumatic conveying systems tailored to the specific needs of each client. The company's expertise in designing and manufacturing these systems allows for the optimization of the equipment to meet the unique requirements of different applications. The systems can be scaled to handle varying capacities, from small-scale operations to large industrial plants, ensuring that the conveying process is efficient and cost-effective. The company's commitment to quality and innovation ensures that their products are reliable and durable, providing long-term performance and minimal maintenance requirements.