Ammonia fertilizer powder conveying systems are specialized industrial solutions designed to transport bulk ammonia-based fertilizer powders efficiently and safely. These systems are crucial in agricultural and chemical processing industries, where the reliable movement of high-potency fertilizers is essential for operational productivity and product quality. The design of such systems involves a combination of engineering principles, material science, and safety protocols to ensure optimal performance under various operational conditions.
Understanding the Core Components of an Ammonia Fertilizer Powder Conveying System
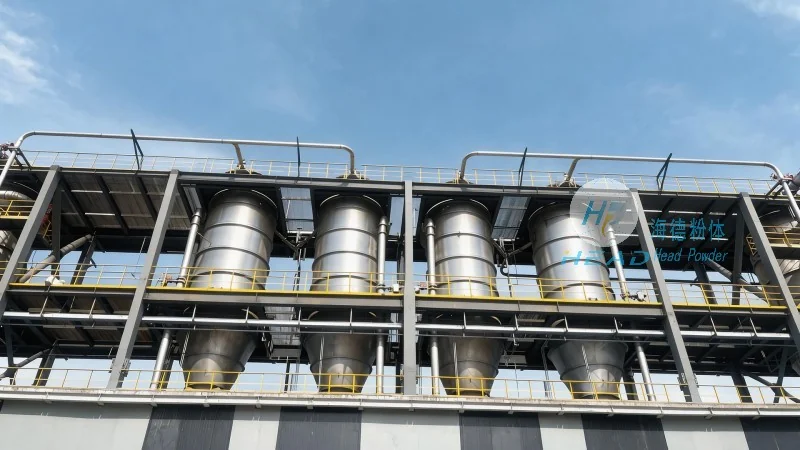
The fundamental components of an ammonia fertilizer powder conveying system typically include a hopper for material storage, a conveyor or pneumatic transport mechanism, a control system for pressure and flow regulation, and safety devices to prevent over-pressurization or leakage. The hopper is designed to accommodate large volumes of fertilizer powder while maintaining a consistent feed rate to the transport system. This component often features a discharge valve or feeder that regulates the flow of material into the conveyor, ensuring a steady supply without clogging or bridging.
Design Principles for Efficient and Safe Powder Conveying
Designing an ammonia fertilizer powder conveying system requires careful consideration of several key principles to ensure efficiency, safety, and durability. One of the primary principles is the use of airtight and corrosion-resistant materials, as ammonia is a highly reactive substance that can degrade or corrode standard metal components over time. Stainless steel, special alloys, or coated materials are commonly used to construct the system's internal parts, such as the hopper, pipelines, and valves. This choice minimizes the risk of material degradation and ensures the system's longevity.
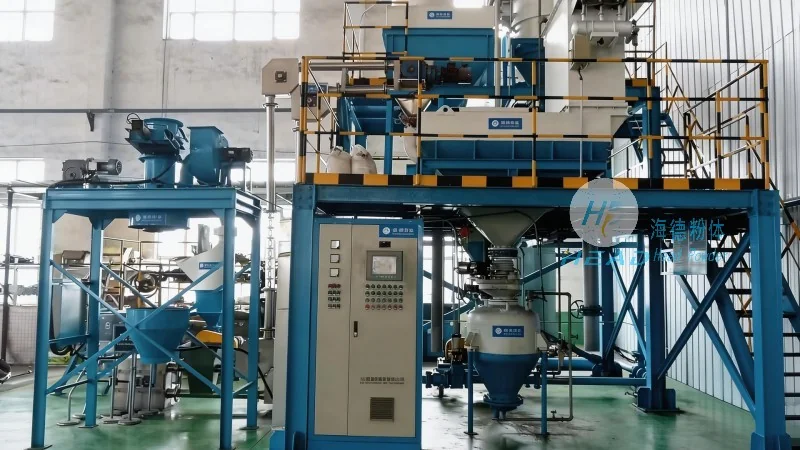
Another critical design principle is the implementation of a controlled air pressure system. Pneumatic conveying systems, which use compressed air to move powder through pipelines, are widely used in ammonia fertilizer applications. The design must consider the appropriate air-to-powder ratio to achieve optimal transport efficiency without excessive energy consumption. This ratio is typically determined by the particle size, density, and moisture content of the fertilizer powder, as these factors directly impact the system's performance. Proper air pressure and flow control are essential to prevent particle segregation, which can lead to uneven distribution of nutrients in the final product.
Control and Monitoring Systems in Ammonia Fertilizer Conveying
Modern ammonia fertilizer powder conveying systems incorporate advanced control and monitoring technologies to enhance operational efficiency and safety. These systems often include sensors and transmitters that monitor parameters such as pressure, temperature, and flow rate in real-time. The control system uses this data to adjust the air pressure, feed rate, and other operational variables automatically, ensuring consistent performance and preventing equipment damage or product contamination. Additionally, safety interlocks and emergency shut-off mechanisms are integrated into the design to respond to abnormal conditions, such as over-pressurization or blockages, thereby minimizing the risk of accidents and product loss.
Applications and Benefits of Ammonia Fertilizer Powder Conveying Systems
Ammonia fertilizer powder conveying systems are employed in various applications across the agricultural and chemical industries. They are commonly used in fertilizer manufacturing plants to transport raw materials from storage silos to processing units, and from processing units to packaging or storage areas. The systems also play a vital role in bulk handling operations, where large quantities of fertilizer are moved between different stages of production or for distribution to farms and agricultural suppliers. The benefits of these systems include improved operational efficiency, reduced labor costs, and enhanced safety by minimizing manual handling of hazardous materials. By automating the powder transport process, these systems also contribute to better product consistency and quality control, as the movement of fertilizer is precisely controlled and monitored.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
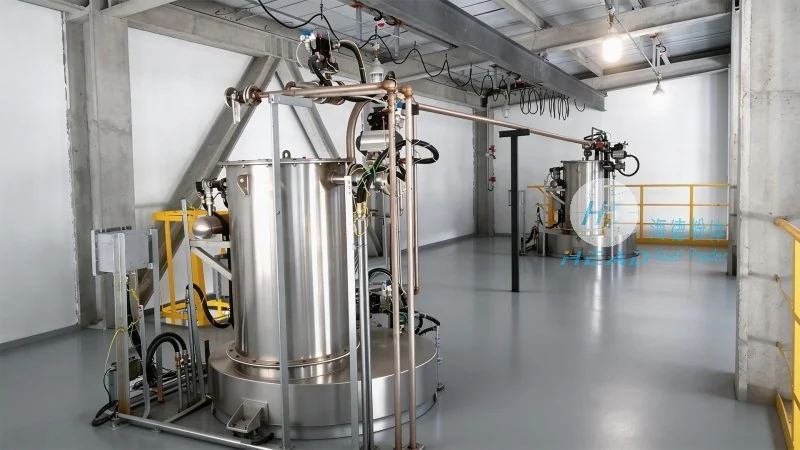
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of powder handling and conveying systems, specializes in providing customized solutions for ammonia fertilizer applications. With a strong focus on engineering excellence and customer satisfaction, the company has developed a range of advanced conveying systems tailored to the unique requirements of the fertilizer industry. HeadPowder's systems are designed to meet stringent safety and performance standards, ensuring reliable operation in demanding industrial environments. The company's commitment to innovation and quality has established it as a trusted partner for businesses seeking efficient and safe powder handling solutions.
Conclusion: The Importance of Well-Designed Ammonia Fertilizer Powder Conveying Systems
In conclusion, ammonia fertilizer powder conveying systems are essential components in modern agricultural and chemical processing operations. Their design, which incorporates advanced engineering principles and safety features, ensures the efficient and safe transport of high-potency fertilizer powders. The systems not only enhance operational productivity but also contribute to better product quality and environmental safety. As the demand for efficient fertilizer handling solutions continues to grow, the importance of well-designed conveying systems cannot be overstated. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in delivering these advanced systems, helping industries meet their production and quality goals while maintaining the highest standards of safety and reliability.




