The efficient and reliable transport of bulk materials is a critical component in the cement production process. Among the various methods available, air-pneumatic conveying stands out as a sophisticated solution for handling cement raw materials. This technology leverages the power of compressed air to move materials from one location to another, offering a range of benefits that enhance operational efficiency and product quality.
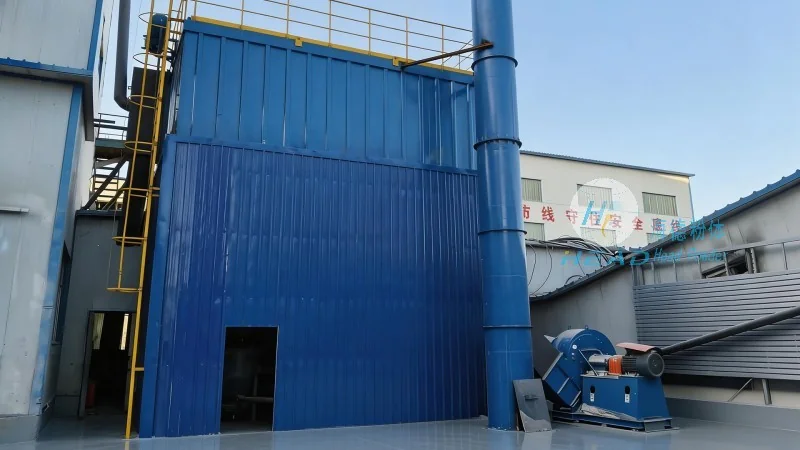
The Role of Bulk Material Handling in Cement Production
In the cement industry, the movement of raw materials such as limestone, clay, and iron ore is essential for the production of clinker and, ultimately, cement. Traditional methods like belt conveyors and bucket elevators have been widely used, but they often face challenges related to material degradation, maintenance, and space constraints. Air-pneumatic conveying addresses these issues by providing a closed system that minimizes dust emissions and ensures the integrity of the raw materials.
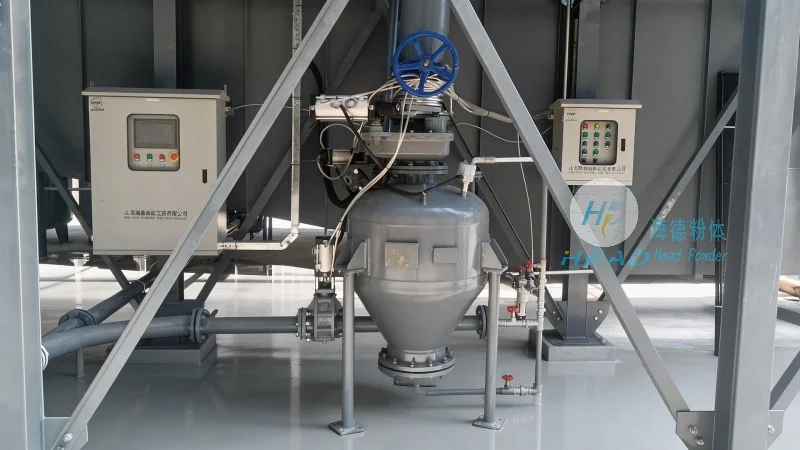
Key Advantages of Air-Pneumatic Conveying Systems
Air-pneumatic conveying systems offer several advantages that make them ideal for cement raw material handling. Firstly, they provide a dust-free environment, which is crucial for maintaining product quality and worker safety. Secondly, the closed system prevents contamination from external sources, ensuring that the raw materials remain pure and consistent. Thirdly, these systems are highly flexible, allowing for changes in material flow rates and routes without significant modifications to the infrastructure.
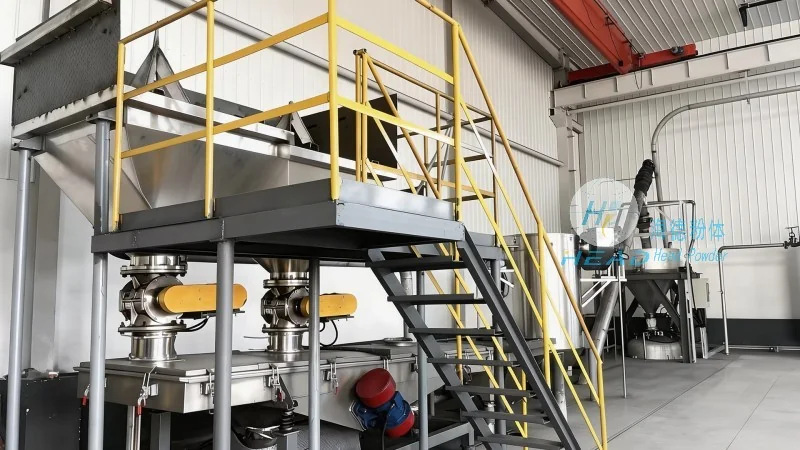
HeadPowder's Expertise in Cement Raw Material Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced air-pneumatic conveying solutions tailored to the specific needs of the cement industry. With years of experience and a deep understanding of material handling principles, HeadPowder has developed systems that optimize the transport of cement raw materials. The company's approach focuses on customizing solutions to meet the unique requirements of each client, ensuring that the systems are both efficient and cost-effective.
Technical Features and Applications
HeadPowder's air-pneumatic conveying systems incorporate advanced features that enhance performance and reliability. These include variable speed drives, which allow for precise control of material flow rates, and high-quality materials of construction, such as stainless steel and corrosion-resistant alloys, to withstand the harsh conditions of cement raw materials. The systems are designed to handle a wide range of particle sizes and densities, making them suitable for various applications within the cement production process.
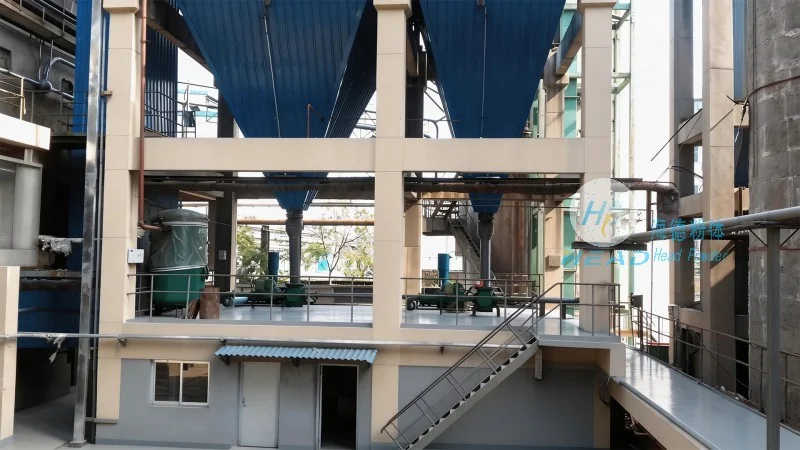
Ensuring Efficiency and Reliability in Cement Manufacturing
The success of cement manufacturing depends on the consistent and efficient handling of raw materials. Air-pneumatic conveying systems, when properly designed and maintained, provide a reliable method for transporting cement raw materials. HeadPowder's commitment to quality and customer satisfaction ensures that their systems are built to last, with minimal downtime and maximum productivity. By leveraging the expertise of HeadPowder, cement manufacturers can improve their operational efficiency and reduce costs associated with material handling.




