HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced bulk material pneumatic conveying systems. These systems are crucial for efficiently transporting powders and granules from hoppers to processing units, ensuring seamless material handling in various industrial applications.
Understanding the Core Principle of Pneumatic Conveying Systems
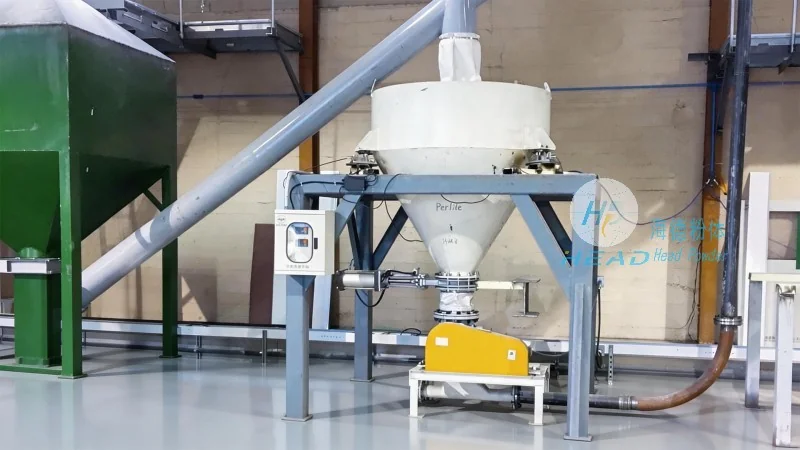
The fundamental principle behind pneumatic conveying systems is the use of compressed air or vacuum to move bulk materials through a pipeline. In a typical hopper-based system, material is drawn from the storage hopper and propelled through a duct by the force of air. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational reliability. The system operates by creating a pressure differential—either positive (air pressure pushing material) or negative (vacuum pulling material)—to achieve material transport. The choice between positive and negative pressure depends on the material characteristics, such as particle size, moisture content, and flowability, as well as the distance and elevation changes required for transport.
Key Working Scenarios and Application Characteristics
HeadPowder's pneumatic conveying systems are tailored to diverse industrial scenarios, each with unique requirements for material handling. For instance, in the chemical industry, these systems are used to transport reactive powders or granules safely, minimizing exposure to human operators and reducing the risk of contamination. The systems are also widely applied in the food and pharmaceutical sectors, where hygiene and material purity are paramount. In these industries, the design incorporates stainless steel components and sealed pipelines to prevent cross-contamination and ensure compliance with regulatory standards.
Advantages in Material Handling Efficiency
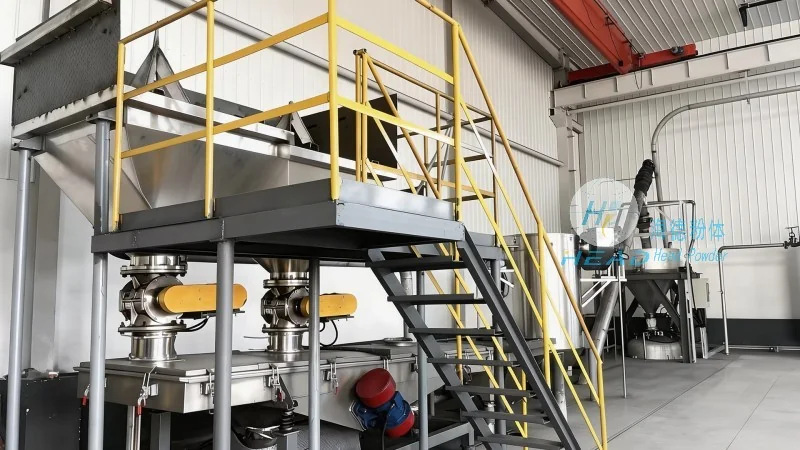
One of the primary advantages of pneumatic conveying systems is their ability to handle a wide range of materials, from fine powders to coarse granules, without degradation. Unlike mechanical conveyors, which can cause material breakage or segregation, pneumatic systems maintain the integrity of the material, preserving its quality for downstream processes. Additionally, these systems offer flexibility in layout, allowing for horizontal, vertical, or mixed-direction transport, which is essential for complex production lines. The automated operation of the system reduces labor costs and enhances safety, as it minimizes human interaction with potentially hazardous materials.
Customization and Scalability for Diverse Needs
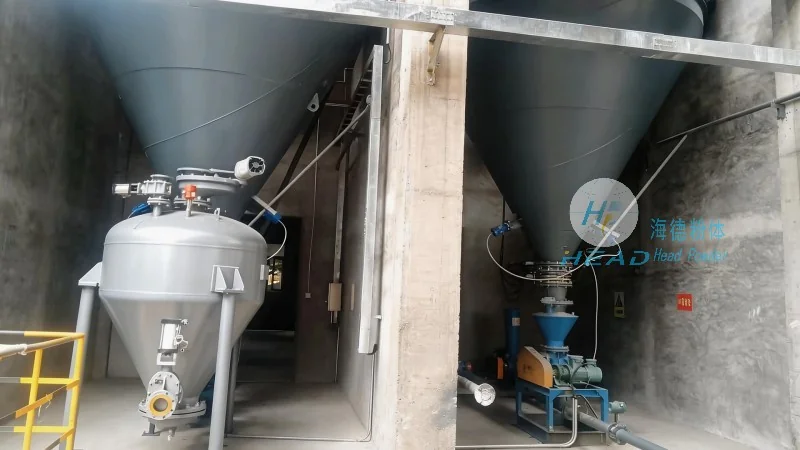
HeadPowder recognizes that each industrial facility has distinct operational needs, and thus, offers customized pneumatic conveying solutions. The company's engineers work closely with clients to assess material properties, transport distances, and process requirements, ensuring the system is optimized for maximum efficiency. Whether it's a small-scale operation requiring a compact system or a large-scale facility needing high-capacity transport, HeadPowder provides scalable solutions that can be expanded or modified as production demands evolve. The modular design of the systems allows for easy integration with existing infrastructure, minimizing downtime during installation.
Conclusion: Enhancing Operational Performance with Advanced Technology
HeadPowder's expertise in pneumatic conveying systems from hoppers enables industries to achieve efficient, reliable, and safe material handling. By leveraging the core principles of air-based transport and adapting to diverse application scenarios, these systems address the challenges of traditional mechanical conveyors while meeting modern industrial standards. As a result, companies in sectors such as chemicals, food, and pharmaceuticals can improve productivity, reduce costs, and maintain product quality, ultimately enhancing their overall operational performance.




