Ammonium bicarbonate, a critical chemical in various industrial applications, demands reliable and efficient transport methods to maintain product integrity and operational efficiency. Traditional bulk handling techniques often face challenges such as dust contamination, material degradation, and limited distance capabilities. In response to these challenges, pneumatic conveying technology has emerged as a leading solution, offering a clean, efficient, and versatile approach to moving ammonium bicarbonate from source to destination. This article explores the benefits and applications of pneumatic conveying for ammonium bicarbonate transport, highlighting how companies like Shandong HeadPowder Engineering Co., Ltd. (headpowder) leverage this technology to deliver superior results.
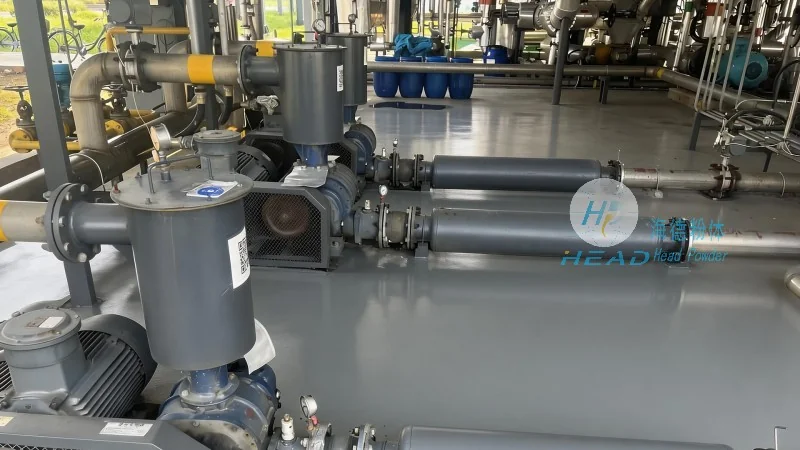
Pneumatic Conveying as a Clean and Efficient Method for Ammonium Bicarbonate Transport
Pneumatic conveying utilizes compressed air or other gases to transport dry bulk materials, including ammonium bicarbonate, through a closed system of pipes. This method eliminates the need for mechanical components like conveyor belts or buckets, reducing friction and wear while minimizing the risk of product contamination. For ammonium bicarbonate, which is sensitive to moisture and environmental factors, pneumatic conveying provides a dust-free environment, preserving the chemical's purity and extending shelf life. The technology also allows for precise control over flow rates and pressure, ensuring consistent and reliable delivery, even over long distances. By integrating advanced engineering principles, pneumatic conveying systems can handle varying particle sizes and bulk densities, making them adaptable to diverse industrial requirements.
HeadPowder's Expertise in Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the unique needs of clients in the chemical and industrial sectors. With a strong focus on innovation and quality, headpowder has established itself as a trusted partner for businesses requiring efficient and clean transport of ammonium bicarbonate. The company's team of engineers and technicians works closely with clients to assess operational parameters, such as required throughput, distance, and environmental constraints, to develop optimal system configurations. Whether for short-distance intra-facility transport or long-distance inter-facility transfer, headpowder's solutions are engineered to maximize efficiency while minimizing operational costs and environmental impact.
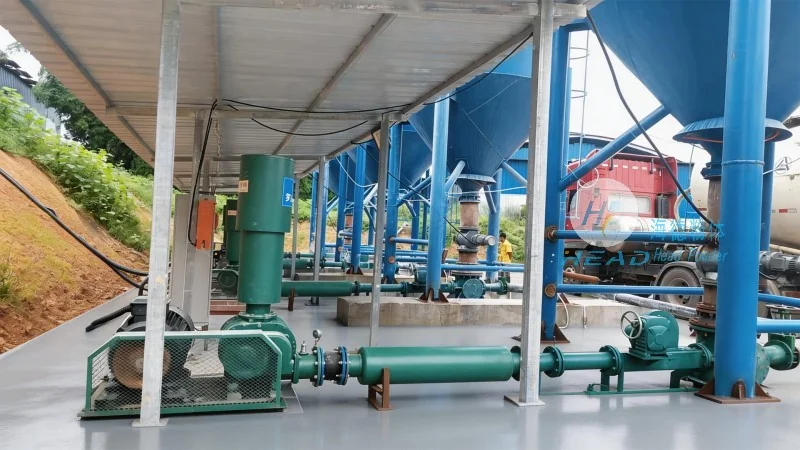
Key Advantages of Pneumatic Conveying for Ammonium Bicarbonate
The adoption of pneumatic conveying for ammonium bicarbonate transport offers several distinct advantages that traditional methods cannot match. Firstly, it provides a completely enclosed system, preventing dust emissions and protecting both the product and the surrounding environment from contamination. This is particularly important for ammonium bicarbonate, which can be hazardous if released into the air or water. Secondly, pneumatic conveying enables high throughput with minimal energy consumption, as the system operates efficiently even at low pressures. This results in lower operational costs and reduced carbon footprint compared to alternative methods. Additionally, the technology allows for easy integration with existing processing equipment, facilitating seamless workflow and enhancing overall productivity. By leveraging advanced materials and design, headpowder's pneumatic conveying systems ensure durability and long-term reliability, reducing maintenance requirements and downtime.
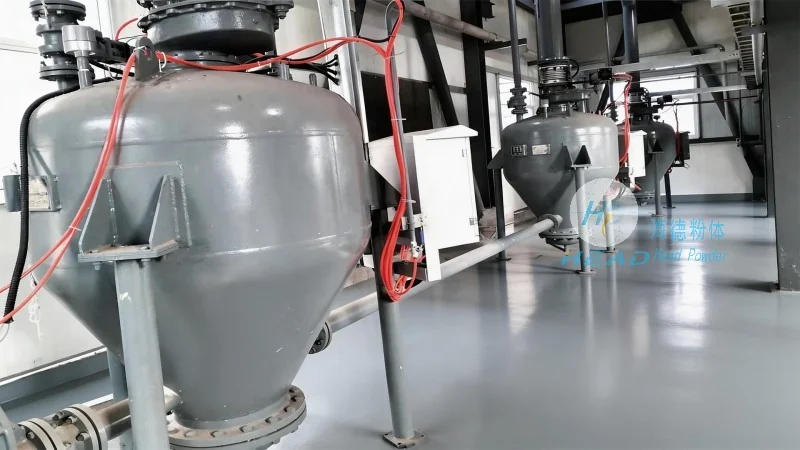
Customized Solutions for Diverse Industrial Needs
Understanding that no two industrial applications are identical, headpowder offers a range of pneumatic conveying solutions to accommodate varying conditions. For instance, clients may require systems with different pressure levels, such as low-pressure or high-pressure designs, depending on the distance and material characteristics. The company also provides options for vacuum or pressure-based conveying, allowing flexibility in system configuration. Furthermore, headpowder's solutions can be integrated with automation and control systems, enabling real-time monitoring and adjustment of transport parameters. This level of customization ensures that each system is optimized for the specific requirements of the ammonium bicarbonate transport process, whether it involves handling large volumes in a fertilizer plant or smaller quantities in a laboratory setting.
In conclusion, pneumatic conveying represents a significant advancement in the efficient and clean transport of ammonium bicarbonate. By combining advanced engineering with a customer-centric approach, companies like Shandong HeadPowder Engineering Co., Ltd. are enabling industries to achieve higher productivity, lower costs, and improved environmental compliance. As the demand for sustainable and reliable bulk handling solutions continues to grow, pneumatic conveying remains a top choice for businesses seeking to optimize their ammonium bicarbonate transport operations. With headpowder's expertise and commitment to quality, clients can trust that their transport needs will be met with the most effective and environmentally friendly solutions available.




