For breweries and malt processing facilities, the efficient and hygienic transport of malt is a critical operational challenge. Traditional methods such as belt conveyors or manual handling often introduce contamination risks and require extensive cleaning, impacting both product quality and production timelines. This article explores the air-flow conveying technology as a superior solution for enhancing malt transport efficiency while maintaining the highest standards of cleanliness.
Understanding Air-Flow Conveying Technology
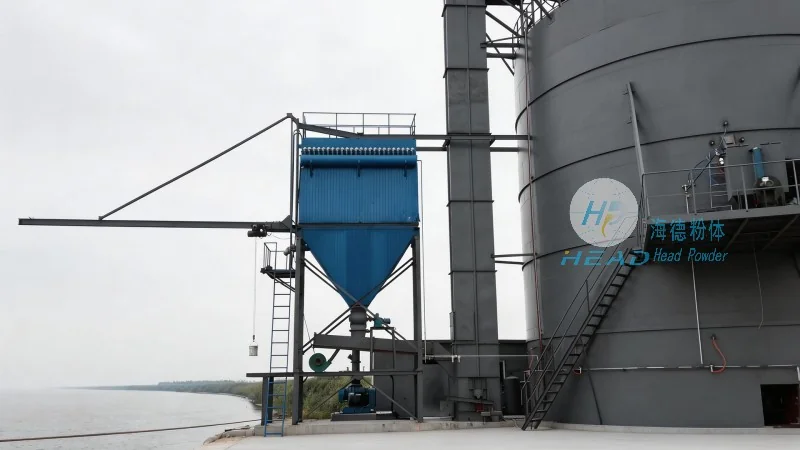
Air-flow conveying, also known as pneumatic conveying, utilizes compressed air or vacuum to move bulk materials like malt through a network of pipes. This method offers several advantages over conventional transport systems. By eliminating direct contact with mechanical components, the risk of cross-contamination is significantly reduced, which is essential for maintaining the purity of malt used in brewing. Additionally, air-flow systems can handle a wide range of particle sizes and moisture content, making them versatile for different types of malt processing.
The Benefits of Air-Flow Conveying for Malt
One of the primary benefits of air-flow conveying is its ability to maintain a clean and sterile environment. Unlike mechanical conveyors that may trap dust or debris, pneumatic systems keep the entire transport path enclosed, preventing external contaminants from entering the malt. This is particularly important in the brewing industry, where even minor impurities can affect the flavor and quality of the final product. Furthermore, air-flow systems allow for precise control over the flow rate and direction of the malt, enabling seamless integration with other processing equipment.
HeadPowder Engineering's Expertise in Malt Conveying Solutions
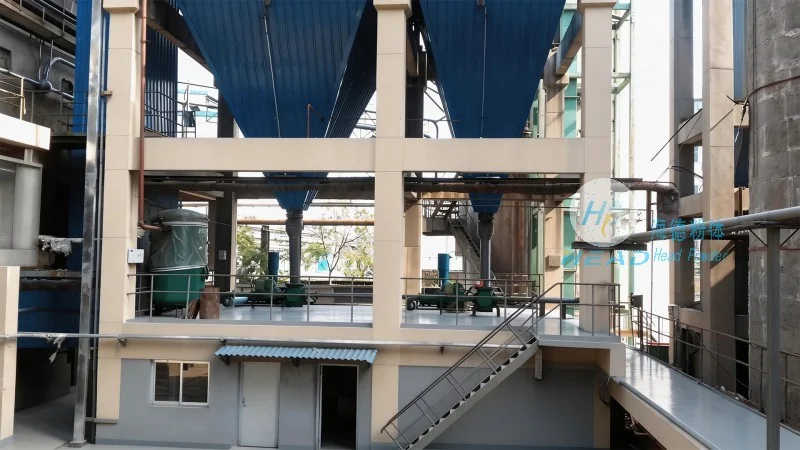
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for the food and beverage industry, specializes in designing and implementing advanced air-flow conveying systems tailored to the specific needs of malt transport. With years of experience in the field, HeadPowder has developed customized solutions that optimize efficiency, reduce downtime, and ensure compliance with industry hygiene standards. The company's team of engineers works closely with clients to assess their operational requirements and recommend the most suitable air-flow system configuration, whether it involves positive pressure, negative pressure, or a combination of both.
Key Features of HeadPowder's Air-Flow Conveying Systems
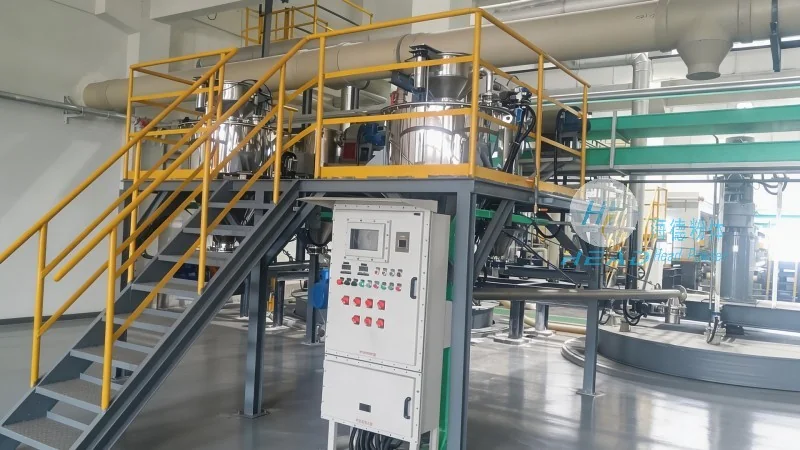
HeadPowder's air-flow conveying systems are equipped with several features that enhance their performance and reliability. These include high-efficiency air filters to maintain air quality, adjustable velocity controls to prevent material degradation, and robust pipe materials that resist corrosion and wear. The systems are also designed for easy maintenance, with quick-access components that allow for routine cleaning and inspection without disrupting production. By leveraging these features, HeadPowder's solutions help breweries and malt producers achieve consistent, high-quality malt transport while minimizing operational costs.
Conclusion: Choosing Clean and Efficient Malt Transport
In conclusion, air-flow conveying technology represents a significant advancement in the efficient and hygienic transport of malt. By eliminating the limitations of traditional methods, this technology offers a superior alternative that meets the demanding requirements of modern breweries. With its ability to maintain cleanliness, control flow precisely, and integrate seamlessly with existing equipment, air-flow conveying is an ideal choice for facilities seeking to enhance their malt transport efficiency. As a trusted partner in the industry, Shandong HeadPowder Engineering Co., Ltd. provides the expertise and solutions needed to implement these advanced systems, ensuring that malt processing remains both productive and compliant with the highest standards of quality and hygiene.




