For industrial applications involving the transport of coal ash particles, traditional methods often face significant challenges such as material degradation, equipment wear, and operational inefficiencies. Pneumatic conveying systems offer a robust and effective solution to address these issues, providing a reliable method for handling coal ash particles with precision and efficiency. This article explores how pneumatic conveying systems, developed by Shandong HeadPowder Engineering Co., Ltd., specifically address the unique challenges associated with coal ash particle transport.
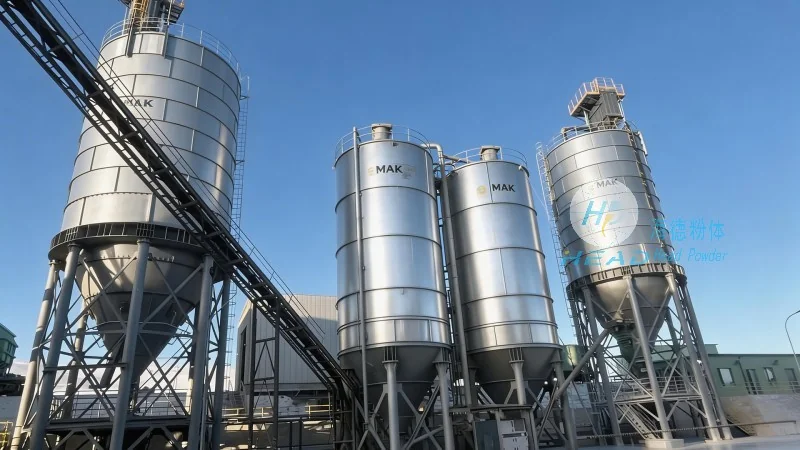
Key Features of Pneumatic Conveying Systems for Coal Ash
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the demands of coal ash particle transport. These systems utilize air pressure to move particles through pipelines, eliminating the need for mechanical components that can cause wear and tear over time. The company's solutions are engineered to handle the abrasive nature of coal ash, ensuring long-term operational reliability and minimal maintenance requirements. By integrating high-efficiency air compressors and specialized pipeline designs, the systems maintain consistent particle flow rates while reducing energy consumption and operational costs.
Benefits of Using Pneumatic Conveying for Coal Ash Transport
The adoption of pneumatic conveying systems for coal ash particle transport brings numerous benefits to industrial operations. Firstly, it enhances material handling efficiency by enabling continuous, automated transport of coal ash from source to destination without the need for manual intervention. This reduces labor costs and improves overall productivity. Secondly, the system minimizes material degradation, as particles are conveyed in a controlled environment, preventing breakage or contamination that can occur with traditional methods like belt conveyors or trucks. Additionally, the reduced wear on equipment extends the lifespan of machinery, leading to lower maintenance expenses and higher return on investment. The systems also offer flexibility in layout, allowing for complex pipeline configurations to accommodate various industrial setups.
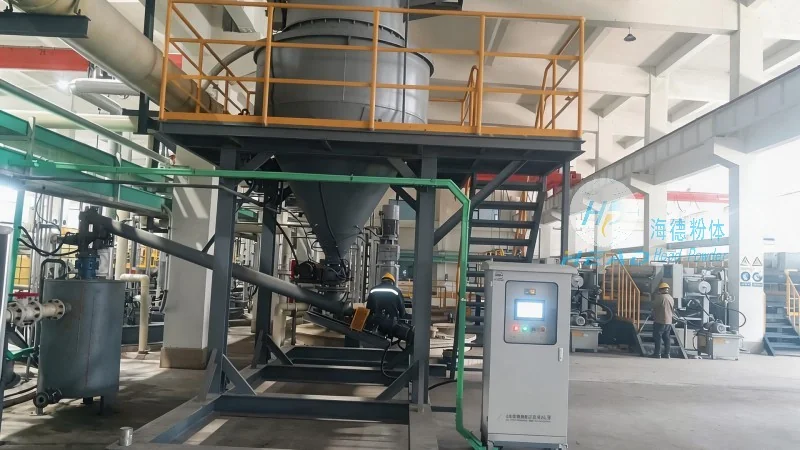
Technical Advancements in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. leverages cutting-edge technology to enhance the performance of pneumatic conveying systems for coal ash transport. Advanced control systems allow for real-time monitoring of particle flow rates, pressure levels, and system performance, enabling operators to adjust parameters dynamically for optimal efficiency. The company's systems incorporate energy-efficient air compressors and optimized pipeline designs that minimize pressure drop, reducing energy consumption and operational costs. Furthermore, the use of high-quality materials in pipeline construction ensures resistance to corrosion and abrasion, extending the system's service life. These technical advancements ensure that the pneumatic conveying systems are not only effective but also sustainable and cost-effective for long-term industrial use.
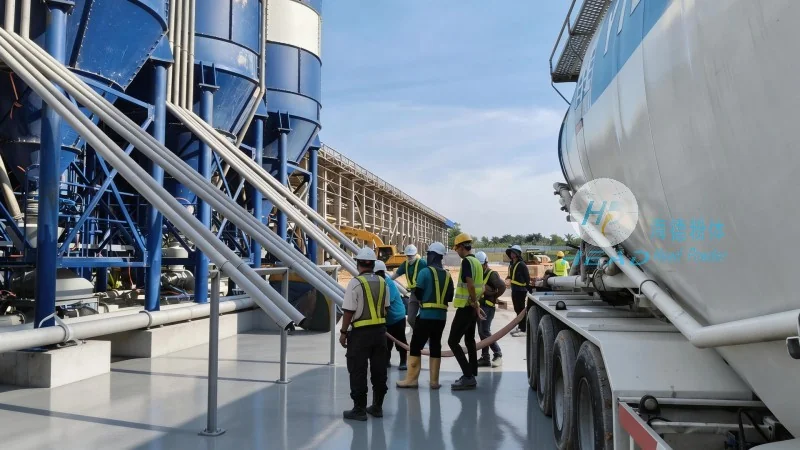
Application Examples and Case Studies
The effectiveness of pneumatic conveying systems for coal ash particle transport is demonstrated through various industrial applications. For instance, in power plants, these systems efficiently transport coal ash from combustion chambers to storage facilities, streamlining the waste management process. In construction material processing facilities, the systems facilitate the transport of coal ash for use as a raw material in cement production, improving production efficiency and reducing transportation costs. Case studies from clients in the energy and construction sectors highlight the consistent performance and reliability of Shandong HeadPowder Engineering Co., Ltd.'s solutions, with many reporting significant improvements in operational efficiency and cost savings after implementing the pneumatic conveying systems.
Conclusion and Future Outlook
Pneumatic conveying systems developed by Shandong HeadPowder Engineering Co., Ltd. provide a comprehensive and effective solution to the challenges of coal ash particle transport. By leveraging advanced technology and specialized engineering, these systems enhance operational efficiency, reduce maintenance costs, and improve material handling reliability. As industrial demands for sustainable and efficient material transport continue to grow, the company's pneumatic conveying solutions remain at the forefront of innovation, offering tailored solutions that meet the specific needs of coal ash transport applications. With a focus on quality and performance, Shandong HeadPowder Engineering Co., Ltd. continues to deliver reliable and efficient pneumatic conveying systems that address the unique challenges of coal ash particle transport, ensuring long-term success for industrial operations.




