Stone powder, a crucial material in various industrial applications, requires efficient and reliable transportation methods to ensure smooth production processes. The development of specialized conveying systems has addressed these needs, with pneumatic conveying emerging as a preferred solution for handling stone powder. This article provides an overview of stone powder conveying systems, highlighting the key advantages of pneumatic conveying technology.
Overview of Stone Powder Conveying Systems
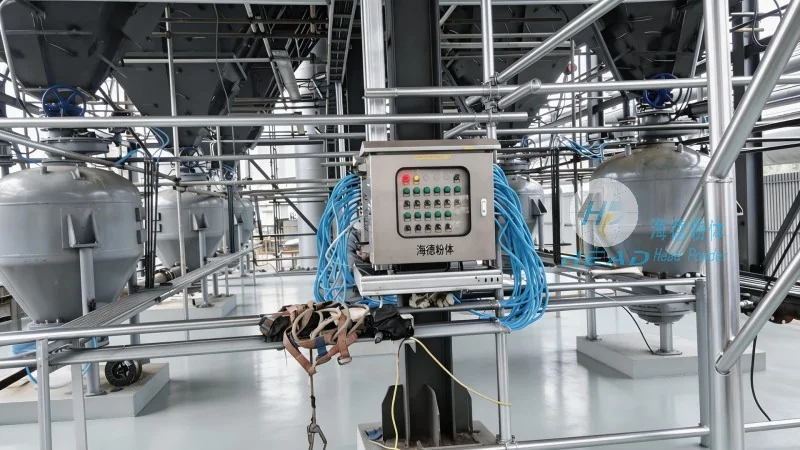
Stone powder, often derived from crushed stone or mineral processing, is a fine particulate material that poses unique challenges during transportation. Traditional methods like belt conveyors or bucket elevators may struggle with dust generation, material segregation, and operational inefficiencies when handling stone powder. To overcome these limitations, specialized conveying systems have been engineered to optimize the movement of stone powder from storage to processing units. These systems typically include components such as hoppers, feeders, pipelines, and control mechanisms, designed to maintain material flow and minimize losses.
HeadPowder: A Leading Provider of Stone Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable company based in Shandong, China, dedicated to providing advanced conveying solutions for stone powder and similar fine materials. With years of experience in the industry, HeadPowder has developed a range of systems tailored to meet the diverse needs of clients across various sectors, including construction, mining, and chemical processing. The company's commitment to innovation and quality has positioned it as a trusted partner for businesses seeking reliable and efficient stone powder handling solutions.
The Advantages of Pneumatic Conveying for Stone Powder
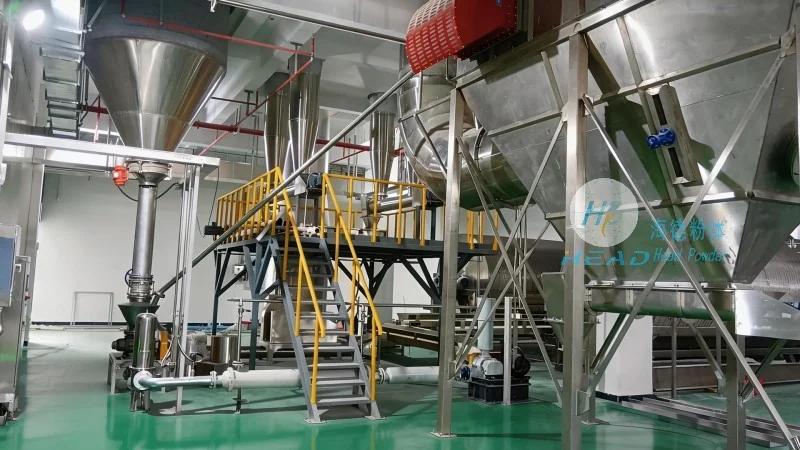
Pneumatic conveying, also known as air-based conveying, offers several advantages over traditional mechanical methods for transporting stone powder. One of the primary benefits is the ability to handle fine and abrasive materials without causing excessive wear on equipment. The system uses compressed air to move material through pipelines, reducing the risk of material degradation and ensuring consistent particle size distribution. Additionally, pneumatic conveying systems are highly flexible, allowing for changes in material flow direction and distance without the need for extensive reconfiguration. This adaptability makes them suitable for complex production layouts and varying operational requirements.
Key Features of HeadPowder's Stone Powder Conveying Systems
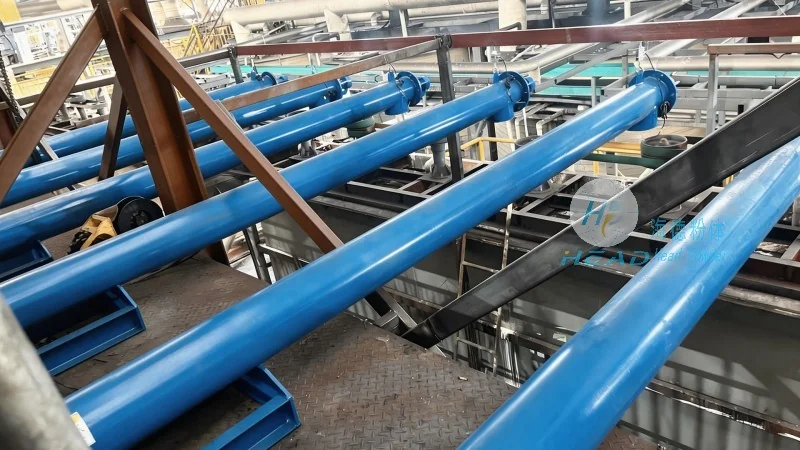
HeadPowder's stone powder conveying systems are equipped with advanced features that enhance performance and reliability. These systems incorporate high-quality materials and components to withstand the abrasive nature of stone powder, ensuring long service life and minimal maintenance. The company's designs often include dust collection and filtration systems to comply with environmental regulations and maintain a clean working environment. Furthermore, the systems are designed for easy integration with existing production lines, minimizing downtime during installation and operation. The control systems are user-friendly, allowing operators to monitor and adjust the conveying process efficiently, thereby optimizing material throughput and reducing operational costs.
Applications and Industry Impact
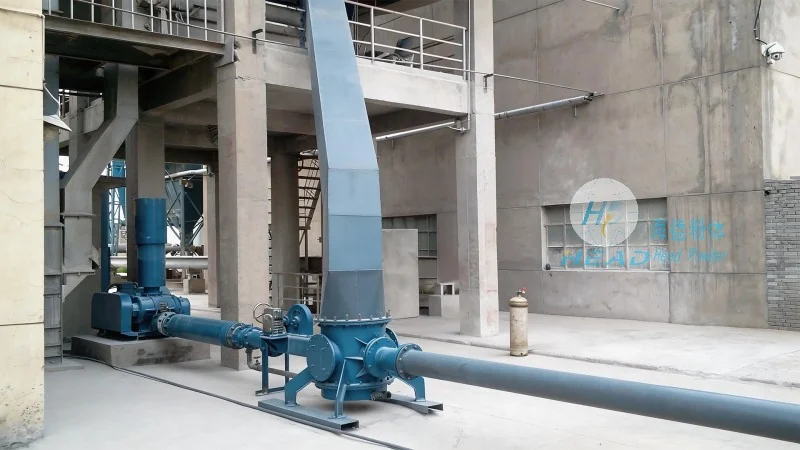
The effectiveness of stone powder conveying systems, particularly those utilizing pneumatic technology, has significantly improved operational efficiency in industries that rely on stone powder. In construction, for example, these systems facilitate the consistent supply of stone powder to mixing plants, ensuring uniform concrete quality. In mining operations, pneumatic conveying helps transport fine ore particles to processing facilities, enhancing productivity and reducing manual handling risks. The ability to handle large volumes of material with minimal labor and space requirements makes these systems ideal for high-volume production environments. By streamlining the transportation process, HeadPowder's systems contribute to overall cost reduction and improved product quality across various applications.
Conclusion and Future Prospects
As the demand for efficient material handling solutions continues to grow, the importance of advanced stone powder conveying systems, especially those leveraging pneumatic technology, becomes increasingly evident. HeadPowder, with its expertise and commitment to innovation, remains at the forefront of providing reliable and efficient solutions for stone powder transportation. The company's systems not only address current operational needs but also adapt to future technological advancements, ensuring that clients can maintain a competitive edge in their respective industries. By prioritizing quality, performance, and customer satisfaction, HeadPowder continues to be a key player in the development and application of stone powder conveying technologies.




