Bentonite, a versatile clay mineral widely used in various industrial applications, requires efficient and reliable transportation methods to ensure optimal performance in processing and handling. The introduction of specialized conveying systems has revolutionized the way bentonite is moved from storage to processing units, enhancing operational efficiency and safety. This overview focuses on the key components and operational principles of bentonite conveying systems, highlighting the critical role they play in modern industrial operations.
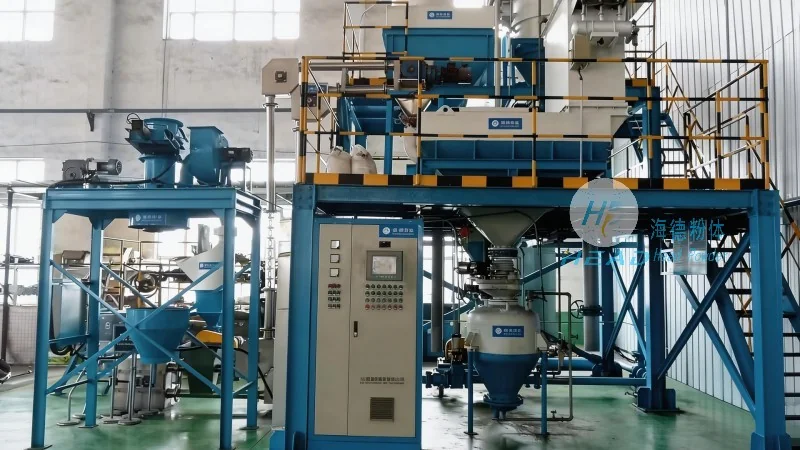
HeadPowder Engineering: Your Partner in Bentonite Conveying Solutions
HeadPowder, a leading manufacturer in the field, offers comprehensive bentonite conveying solutions tailored to meet the diverse needs of industrial clients. With a strong commitment to quality and innovation, HeadPowder Engineering Co., Ltd. has established itself as a trusted provider of advanced conveying systems. Based in Shandong, China, the company leverages local expertise and global standards to deliver robust, durable, and efficient equipment for bentonite handling. The company’s team of experienced engineers and technicians ensures that each system is designed to meet specific operational requirements, providing customized solutions that enhance productivity and reduce downtime.
Pneumatic Conveying: The Preferred Method for Bentonite Transport
Pneumatic conveying stands out as the most effective method for transporting bentonite due to its numerous advantages over traditional mechanical systems. This technique utilizes air pressure to move the material through a pipeline, offering several key benefits that make it ideal for bentonite applications. One of the primary advantages is the ability to handle fine, powdery materials without the need for mechanical components that can cause wear and tear or contamination. The system also provides a clean and hygienic environment, which is crucial for industries where product purity is paramount. Additionally, pneumatic conveying allows for flexible system designs, enabling the integration of multiple processing stages and facilitating easy expansion or modification as operational needs evolve.
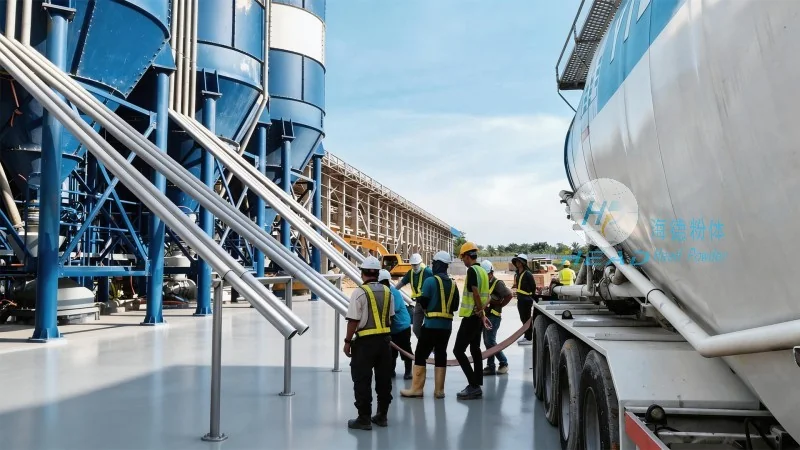
Key Advantages of Pneumatic Conveying for Bentonite
When considering the advantages of pneumatic conveying for bentonite, several critical benefits emerge that contribute to improved operational performance. First, the system offers high efficiency in material transport, with the ability to move large volumes of bentonite over long distances with minimal energy consumption. This efficiency translates into lower operational costs and increased productivity, making it a cost-effective solution for industrial applications. Second, pneumatic conveying provides excellent control over the material flow, allowing for precise regulation of the conveying rate and pressure. This control is essential for maintaining consistent product quality and preventing overloading or underloading of processing equipment. Third, the system is highly flexible, capable of adapting to different material characteristics and operational conditions. Whether dealing with dry or slightly moist bentonite, the system can be adjusted to ensure optimal performance, reducing the risk of material blockages or system failures. Finally, pneumatic conveying enhances safety by eliminating the need for manual handling of bulk materials, minimizing the risk of accidents and improving workplace safety standards.
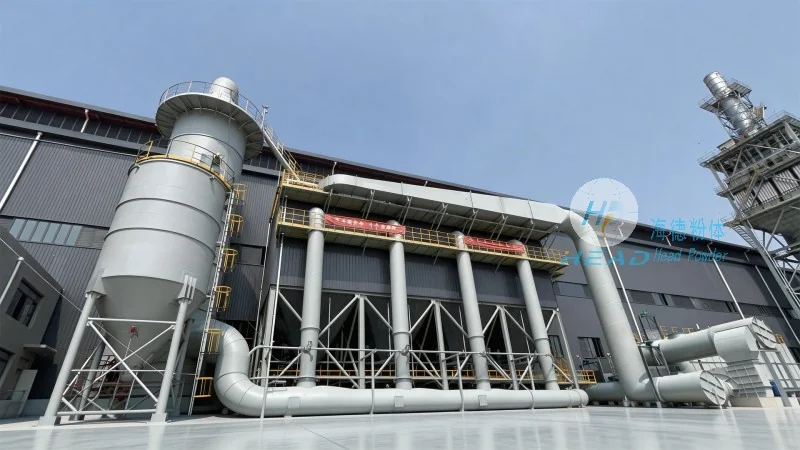
Customization and Integration: Tailoring Conveying Systems to Specific Needs
HeadPowder Engineering recognizes that each industrial application has unique requirements, and therefore, offers customized pneumatic conveying systems designed to meet specific operational needs. The company’s engineering team works closely with clients to understand their processing requirements, material characteristics, and operational constraints, ensuring that the final system is optimized for maximum efficiency and reliability. Customization may include adjustments to the system’s capacity, pressure levels, and material handling capabilities, as well as integration with existing processing equipment. This tailored approach ensures that the conveying system not only meets current needs but also accommodates future expansion or changes in production processes. The company also provides comprehensive support, including installation, commissioning, and maintenance services, ensuring that clients receive a complete solution from a single source.
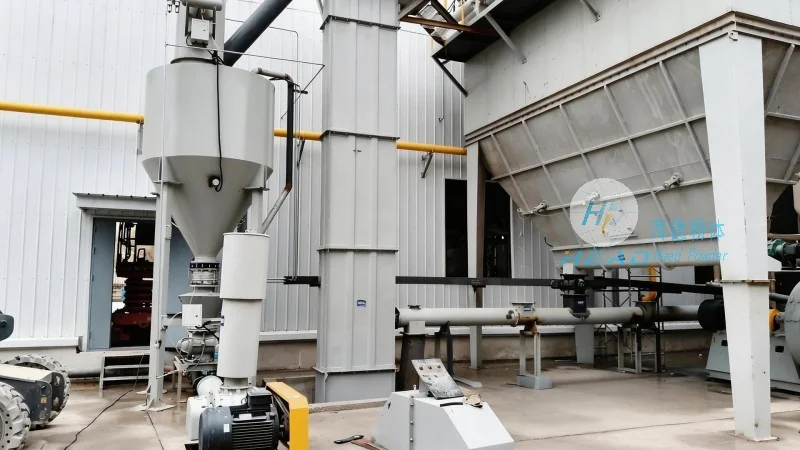
Enhancing Productivity and Cost-Effectiveness
The implementation of advanced bentonite conveying systems, particularly pneumatic conveying, significantly enhances productivity and cost-effectiveness in industrial operations. By reducing material handling time and improving the efficiency of the transport process, companies can increase their overall production output. The lower energy consumption associated with pneumatic systems also contributes to reduced operational costs, providing a competitive advantage in the market. Additionally, the reduced need for manual labor in material handling improves workplace safety and reduces the risk of accidents, leading to lower insurance costs and improved employee morale. The durability and reliability of the equipment, combined with minimal maintenance requirements, further contribute to long-term cost savings and operational stability.
Conclusion: Choosing the Right Bentonite Conveying Solution
In conclusion, the introduction of advanced bentonite conveying systems, particularly pneumatic conveying, has transformed the way bentonite is handled in industrial applications. The advantages of these systems, including efficiency, flexibility, and safety, make them the preferred choice for many industries. HeadPowder Engineering Co., Ltd., with its expertise and commitment to quality, offers reliable and customized solutions that meet the specific needs of clients. By investing in advanced conveying systems, industrial companies can enhance their operational efficiency, reduce costs, and improve product quality, ensuring long-term success in their respective markets.




