For those in the food processing industry, especially those dealing with maltose, understanding the technology behind efficient material handling is crucial. A maltose pneumatic conveying system is a specialized equipment designed to transport maltose and similar granular or powdered materials through a pipeline using air pressure. This system offers a clean, efficient, and cost-effective solution for moving maltose from one location to another within a production facility.
Introduction to Maltose Pneumatic Conveying Systems
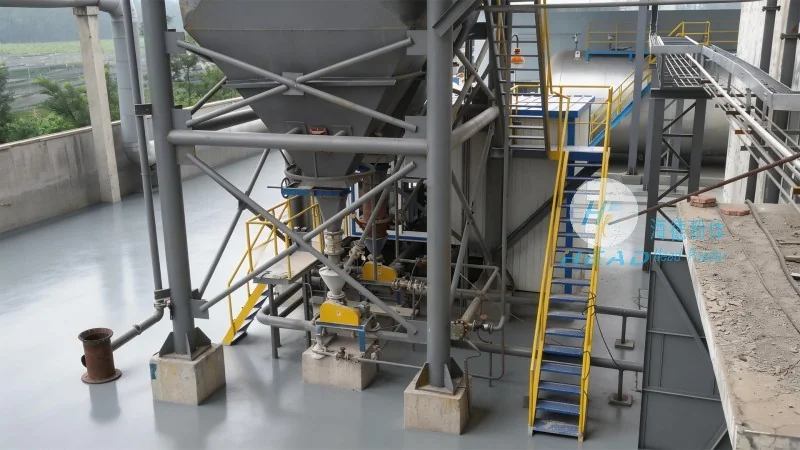
A maltose pneumatic conveying system is a type of pneumatic conveying equipment specifically engineered for the transport of maltose, a common sugar used in food and beverage production. Unlike traditional mechanical conveyors, which rely on belts or screws, pneumatic systems use air to move materials. This method is particularly advantageous for handling fine powders and granules like maltose, as it minimizes product contamination and reduces the risk of material degradation.
Understanding the Core Function of Maltose Pneumatic Conveying Systems
The primary function of a maltose pneumatic conveying system is to transport maltose from a source, such as a storage silo or production line, to a destination, like a mixing tank or packaging area. The system operates by creating a pressure differential within the pipeline. Air is introduced into the system, either by a blower or compressor, and is used to lift and move the maltose particles through the pipeline. The design ensures that the maltose remains suspended in the air stream, preventing clogging and ensuring smooth flow.
Design Principles of Maltose Pneumatic Conveying Systems
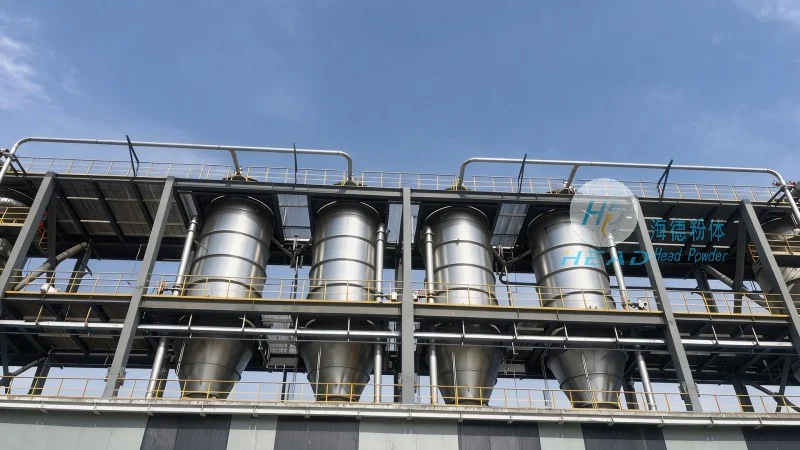
The design of a maltose pneumatic conveying system is based on several key principles to ensure optimal performance and efficiency. The first principle is the selection of the appropriate air velocity. The air velocity must be high enough to keep the maltose particles suspended but low enough to prevent excessive wear on the pipeline and components. This balance is critical for maintaining the system's longevity and minimizing maintenance costs. Another key design principle is the use of appropriate pipeline materials. Since maltose is a food product, the system must use materials that are food-grade and resistant to corrosion and contamination. Common materials include stainless steel and food-grade plastics.
Key Components and Their Roles in the System
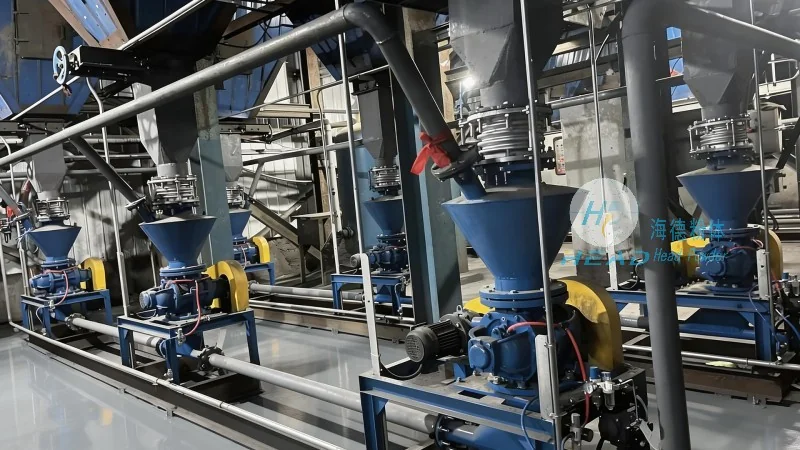
A maltose pneumatic conveying system consists of several key components, each playing a vital role in the overall operation. The main components include a material feeder, which introduces the maltose into the system; a blower or compressor, which provides the air pressure; a pipeline system, which transports the maltose; and a receiver, which collects the maltose at the destination. The material feeder is designed to handle the specific characteristics of maltose, such as its granular size and flowability. The blower or compressor generates the necessary air pressure to move the maltose through the pipeline. The pipeline system is typically made of flexible or rigid materials, depending on the application, and is equipped with valves and fittings to control the flow. The receiver is designed to collect the maltose and prevent it from spilling or contaminating the surrounding environment.
Application Scenarios and Benefits of Using Maltose Pneumatic Conveying Systems
Maltose pneumatic conveying systems are widely used in various applications within the food processing industry. They are commonly used in the production of maltose-based products, such as maltose syrup, maltose powder, and other food additives. The system is also used in the pharmaceutical industry for transporting maltose used as a sweetener or excipient. The benefits of using a maltose pneumatic conveying system include improved hygiene, as the system is enclosed and prevents contamination from external sources. It also offers increased efficiency, as the system can transport maltose over long distances without the need for multiple transfer points. Additionally, the system reduces labor costs, as it automates the material handling process, and minimizes product loss, as the maltose is not exposed to the air or other contaminants during transport.
About the Company: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of pneumatic conveying systems, specializing in solutions for the food and pharmaceutical industries. With years of experience in the industry, the company has developed a reputation for producing high-quality, reliable, and efficient maltose pneumatic conveying systems. The company's headquarters is located in Shandong, China, and it serves clients both domestically and internationally. HeadPowder's team of engineers and technicians are dedicated to providing customized solutions that meet the specific needs of each client. The company's commitment to quality and customer satisfaction has made it a trusted partner for many businesses in the industry.




