In today’s industrial landscape, the efficient and safe handling of bulk powders is a top priority for manufacturers across various sectors. Pneumatic conveying systems have emerged as a leading technology for this purpose, offering a reliable method to transport materials from one location to another while maintaining product integrity. The role of pneumatic conveying in powder handling is not just about moving material; it’s about ensuring that the process is optimized for speed, safety, and cost-effectiveness. For companies dealing with sensitive or high-value powders, such as pharmaceuticals, food ingredients, or specialty chemicals, the choice of a proper conveying system can significantly impact their bottom line and brand reputation.
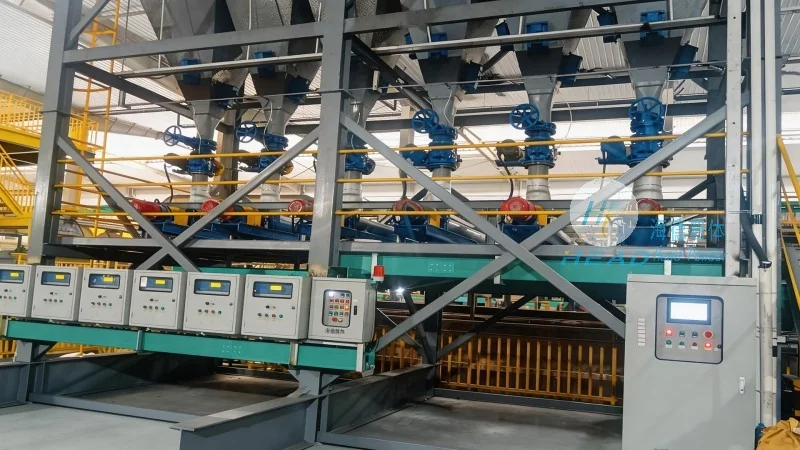
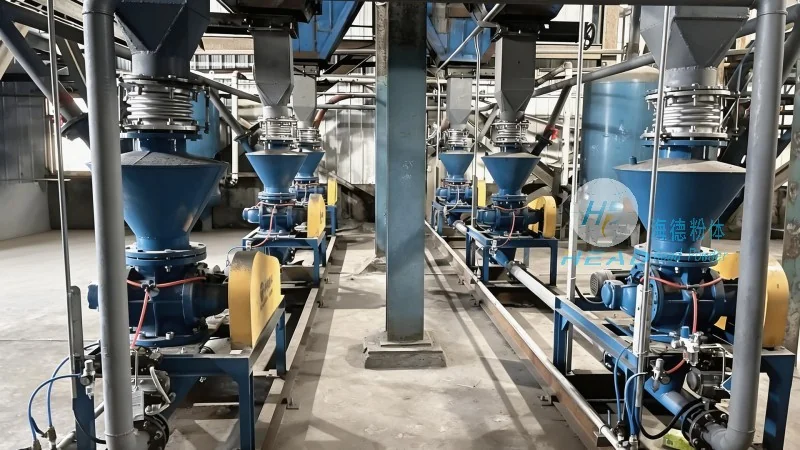
Key Advantages of Pneumatic Conveying for Powder Transport
One of the most significant advantages of pneumatic conveying is its ability to handle a wide variety of powder characteristics, including fine powders, cohesive materials, and even materials that are prone to dusting. Unlike mechanical systems that may cause product degradation through friction or mixing, pneumatic systems use a controlled air flow to transport materials, minimizing the risk of contamination and degradation. This is especially crucial in industries where product purity is non-negotiable, such as in the pharmaceutical and food industries. Additionally, pneumatic conveying systems are highly flexible, allowing for complex layouts that can accommodate vertical lifts, horizontal transfers, and even multi-stage processing within a single pipeline. This flexibility reduces the need for multiple pieces of equipment, streamlining the overall process and lowering operational costs.
How Pneumatic Conveying Enhances Process Efficiency
The efficiency of pneumatic conveying systems is a result of their continuous operation and low energy consumption. Unlike batch processing or intermittent mechanical systems, pneumatic conveyors can operate continuously, ensuring a steady flow of material without interruptions. This continuous operation leads to higher throughput and reduced downtime, which are critical for maintaining production schedules and meeting customer demands. Moreover, the enclosed nature of pneumatic systems effectively controls dust emissions, improving workplace safety and environmental compliance. This not only protects employees from respiratory hazards but also helps companies avoid fines and maintain a positive public image. By integrating pneumatic conveying into their processes, businesses can achieve a more sustainable and efficient operation, aligning with modern industrial standards and regulatory requirements.
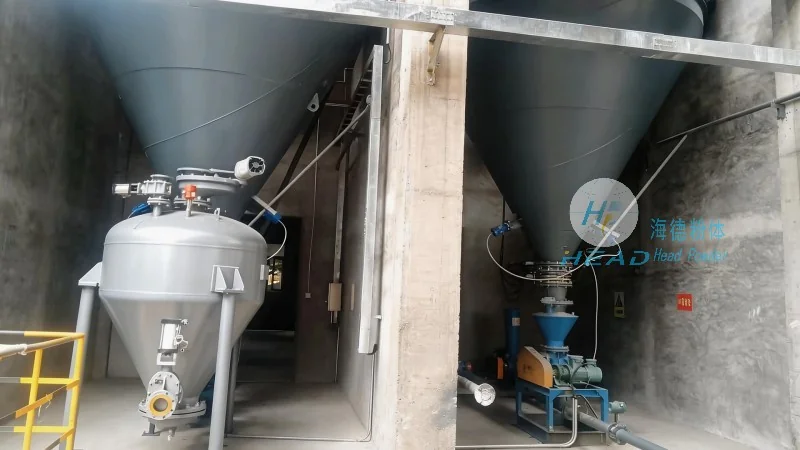
Customized Solutions from Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of pneumatic conveying solutions, dedicated to delivering high-quality systems that meet the specific needs of our clients. With years of experience in the industry, our team of experts understands the unique challenges faced by different sectors, from pharmaceuticals to food processing and chemical manufacturing. We offer customized designs that can be tailored to handle various powder types, flow rates, and system configurations. Our products are built with durable materials and advanced technology to ensure long-term reliability and minimal maintenance. By choosing our solutions, businesses can enhance their operational efficiency, reduce costs, and improve product quality. Our commitment to quality and customer satisfaction has made us a trusted partner for companies worldwide, helping them achieve their production goals while maintaining the highest standards of safety and environmental responsibility.




