Calcined ash, a byproduct of industrial processes such as cement production and power generation, requires efficient and reliable handling systems to ensure safe and effective transportation. The pneumatic conveying system is a critical solution for managing calcined ash, offering advantages like reduced labor costs, minimized environmental impact, and enhanced operational efficiency. This article provides an in-depth analysis of the components, operation, and benefits of a calcined ash pneumatic conveying system, tailored to meet the demands of modern industrial applications.
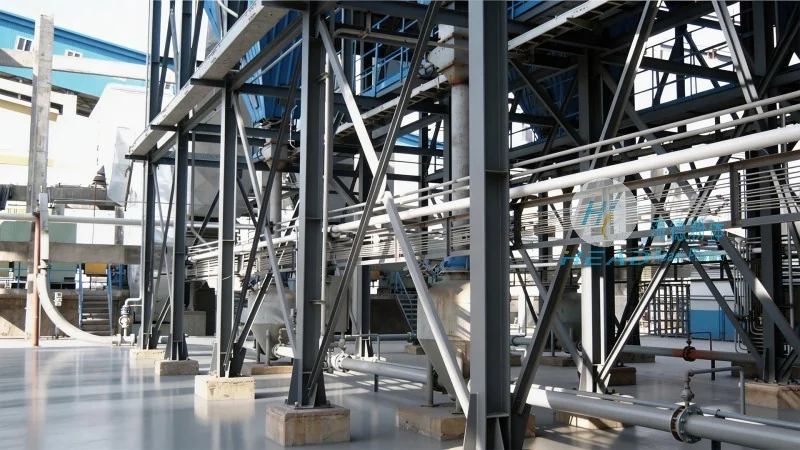
Key Components of the Pneumatic Conveying System
The calcined ash pneumatic conveying system consists of several essential components that work in tandem to achieve effective material transport. These include the ash hopper, which serves as the storage and feeding unit, equipped with a rotary valve to control the flow of ash into the system. The conveyor itself, typically a pipeline system, uses compressed air to move the ash particles through the pipeline. A filter system is also integral, designed to capture any fine particles and ensure compliance with air quality standards. Additionally, the system may incorporate a pressure vessel or receiver to manage the air pressure and ash collection, ensuring smooth operation and preventing blockages.
Operational Principles and Efficiency
The pneumatic conveying system operates on the principle of using air pressure to transport solid materials. In the case of calcined ash, the system utilizes positive pressure or negative pressure (or a combination of both) to move the ash particles through the pipeline. Positive pressure systems, where air is blown into the pipeline, are commonly used for long-distance or high-capacity transport, as they can handle larger volumes and overcome greater resistance. Negative pressure systems, where air is drawn out of the pipeline, are often employed for shorter distances or when the ash needs to be transported to a lower elevation. The efficiency of the system is influenced by factors such as the ash's particle size, moisture content, and density, as well as the design of the pipeline and the air pressure used. Proper maintenance and regular cleaning of the system components are crucial to maintain optimal performance and prevent system downtime.
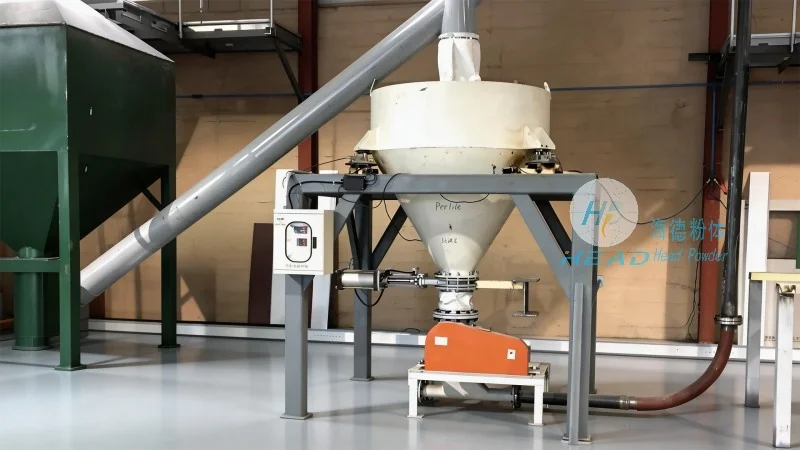
Benefits and Applications
The calcined ash pneumatic conveying system offers numerous benefits that make it a preferred choice for industrial applications. One of the primary advantages is the reduction in labor costs, as the system automates the ash handling process, eliminating the need for manual handling and reducing the risk of accidents. Additionally, the system minimizes environmental impact by containing the ash within the pipeline, preventing dust emissions and ensuring compliance with environmental regulations. The system also enhances operational efficiency by providing a continuous and reliable flow of ash, which is essential for maintaining the productivity of downstream processes. The system is widely used in cement plants, power stations, and other industrial facilities where calcined ash needs to be transported from the production site to storage or disposal areas.
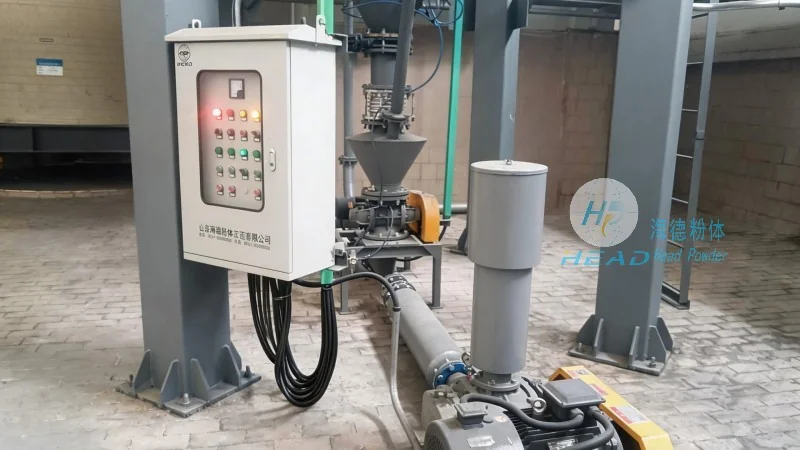
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of industrial engineering solutions, specializing in the design and manufacturing of calcined ash pneumatic conveying systems. With a strong focus on innovation and quality, the company has established itself as a trusted partner for industries requiring efficient and reliable ash handling solutions. The company's team of experienced engineers and technicians works closely with clients to understand their specific needs and develop customized solutions that meet their operational requirements. HeadPowder's commitment to excellence is reflected in its adherence to international standards and rigorous quality control processes, ensuring that each system is built to the highest specifications and delivers long-term performance and reliability.
Conclusion
In conclusion, the calcined ash pneumatic conveying system is a vital component in modern industrial operations, providing an efficient and reliable solution for handling calcined ash. The system's ability to automate the ash handling process, reduce environmental impact, and enhance operational efficiency makes it an essential investment for industries such as cement production and power generation. With the expertise and experience of companies like Shandong HeadPowder Engineering Co., Ltd., industries can rely on high-quality pneumatic conveying systems that meet their specific needs and contribute to their overall success. As the demand for sustainable and efficient industrial solutions continues to grow, the calcined ash pneumatic conveying system remains a key technology in ensuring the safe and effective management of industrial byproducts.




