Organic fertilizer granule pneumatic conveying systems represent a critical technology in the agricultural and fertilizer processing industries. These systems are designed to efficiently transport granular organic fertilizers from storage or processing areas to application points, such as spreaders or storage silos. The technology leverages air pressure to move materials, offering advantages over traditional mechanical conveying methods in terms of speed, flexibility, and reduced wear on equipment. For businesses involved in organic fertilizer production and distribution, understanding the components, operation, and benefits of these systems is essential for optimizing operational efficiency and maintaining product quality.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design, development, and supply of advanced pneumatic conveying solutions. With a strong focus on innovation and customer-centric engineering, HeadPowder has established itself as a trusted partner for companies seeking reliable and efficient organic fertilizer handling systems. HeadPowder’s expertise spans the entire spectrum of pneumatic conveying technologies, from basic bulk material transport to complex, multi-stage systems tailored to specific industrial needs. The company’s commitment to quality and performance has earned it a reputation for delivering durable, high-performance equipment that meets the demanding requirements of modern fertilizer processing operations.
Key Components of the Organic Fertilizer Granule Pneumatic Conveying System
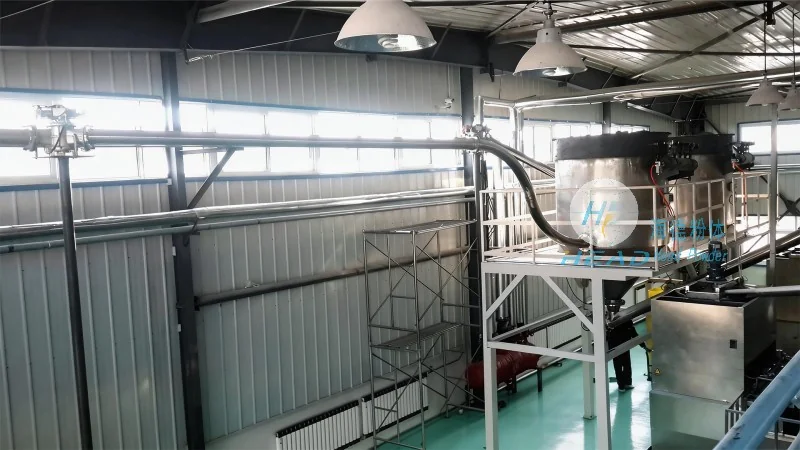
The organic fertilizer granule pneumatic conveying system consists of several core components that work in tandem to ensure efficient material transport. The primary components include a hopper or storage bin for holding the granular fertilizer, an air compressor or blower to generate the necessary air pressure, a conveying line (typically made of flexible or rigid tubing), and a receiver or discharge point where the material is deposited. Additionally, the system may incorporate accessories such as filters to remove dust and moisture from the air, pressure regulators to control air flow, and control valves to manage the conveying process. Each component plays a vital role in maintaining the system’s efficiency and ensuring the safe and reliable transport of organic fertilizer granules.
How the Pneumatic Conveying System Operates
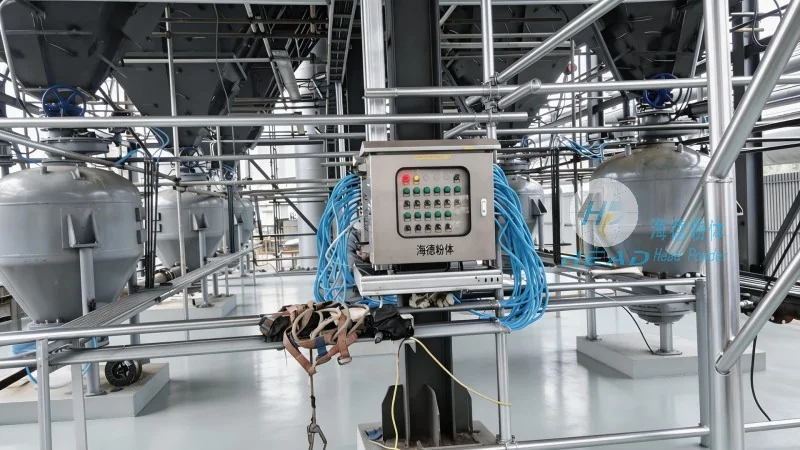
The operation of an organic fertilizer granule pneumatic conveying system involves a sequence of steps that utilize air pressure to move material through the conveying line. Initially, the granular fertilizer is fed into the hopper or storage bin. When the system is activated, the air compressor generates a high-pressure air stream, which is then introduced into the conveying line. The air stream creates a low-pressure zone within the line, causing the fertilizer granules to be drawn into the air stream and carried along the line to the receiver. The system may use either positive pressure (where air is forced into the line) or negative pressure (where air is drawn out of the line) to move the material, depending on the specific application and layout. The conveying line is typically designed with bends and turns to accommodate the path from the storage area to the discharge point, and the system may include pulse-jet or rotary airlock valves to regulate the flow of material and air. The receiver, often a silo or storage tank, collects the conveyed fertilizer, which can then be further processed or applied as needed.
Advantages of Using Organic Fertilizer Granule Pneumatic Conveying Systems
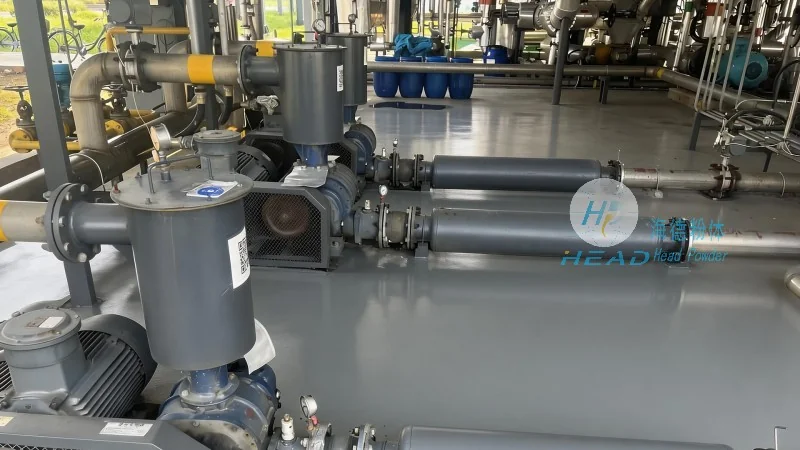
Organic fertilizer granule pneumatic conveying systems offer several key advantages over traditional mechanical conveying methods. One of the most significant benefits is the speed and efficiency of material transport. By using air pressure, the system can move large volumes of granular fertilizer quickly and with minimal downtime, reducing the time required for loading and unloading operations. Additionally, pneumatic conveying systems are highly flexible, allowing for easy reconfiguration of the conveying path to accommodate changes in production or storage layouts. This flexibility is particularly valuable in dynamic industrial environments where operational needs may change frequently. Another advantage is the reduced wear and tear on equipment, as the system minimizes contact between the fertilizer granules and mechanical components, such as belts or buckets. This results in lower maintenance costs and longer equipment lifespan. Furthermore, pneumatic conveying systems can handle a wide range of granule sizes and densities, making them suitable for various types of organic fertilizers, including compost, manure, and biochar-based products. The ability to transport materials in a dust-free environment also contributes to improved workplace safety and product quality, as it prevents contamination and dust accumulation.
Applications and Use Cases
Organic fertilizer granule pneumatic conveying systems are widely used in various applications within the agricultural and fertilizer industry. One common application is the transport of granular organic fertilizers from production facilities to storage silos or bulk storage tanks. This allows for efficient storage and distribution of the fertilizer, ensuring that it is readily available for application on farms or in agricultural settings. The systems are also used in the transfer of fertilizer from storage areas to application equipment, such as spreaders or sprayers, enabling precise and uniform distribution of the organic fertilizer over fields. Additionally, these systems are employed in the processing of organic waste materials, such as animal manure or agricultural residues, where the granules are produced and then conveyed to processing units for further treatment or packaging. The versatility of pneumatic conveying systems makes them suitable for both small-scale and large-scale operations, from individual farms to industrial fertilizer plants. In industrial settings, the systems may be integrated into larger production lines, where the organic fertilizer is conveyed to mixing or blending equipment before being packaged for sale. The ability to handle different types of organic fertilizers and adapt to various operational requirements makes the pneumatic conveying system a valuable asset for companies involved in organic fertilizer production and distribution.




