Small bag weighing and quantitative powder conveying equipment is a specialized device designed for precise handling and transportation of bulk powders. This equipment is widely used in various industries such as pharmaceuticals, food processing, and chemical manufacturing, where accurate dosage and efficient material transfer are critical for production efficiency and product quality. The following introduction will provide an overview of the equipment's structure and working principle, along with key features that make it an essential tool in modern industrial operations.
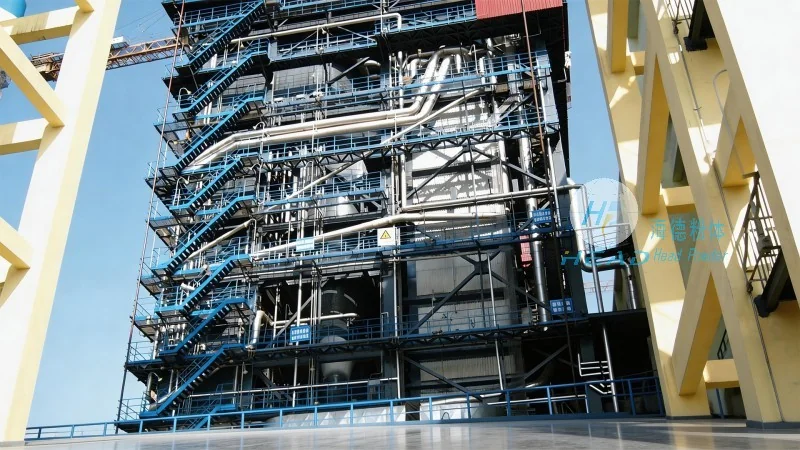
Overview of Small Bag Weighing and Quantitative Powder Conveying Equipment
Small bag weighing and quantitative powder conveying equipment, as the name implies, is engineered to handle powders in small bag formats. The primary function of this equipment is to weigh the powder within each bag and then transfer it to the next processing stage. It combines weighing technology with material conveying mechanisms to ensure that each bag is filled with the exact amount of powder required, minimizing waste and maximizing productivity. The equipment is typically designed to handle a wide range of powder types, including fine powders, granules, and other bulk materials, making it versatile for different industrial applications.
Key Components and Structure of the Equipment
The structure of small bag weighing and quantitative powder conveying equipment consists of several key components that work in tandem to achieve precise operation. The main components include a weighing platform, a bag holder or bag dispenser, a conveyor system, a control unit, and a feeding mechanism. The weighing platform is where the small bags are placed and weighed. It is equipped with load cells that accurately measure the weight of the powder in the bag. The bag holder or dispenser is responsible for holding and positioning the bags on the weighing platform. The conveyor system is used to transport the filled bags from the weighing area to the storage or packaging area. The control unit manages the entire operation, including the weighing process, bag movement, and conveyor control. The feeding mechanism ensures that the powder is fed into the bags at the correct rate and quantity.
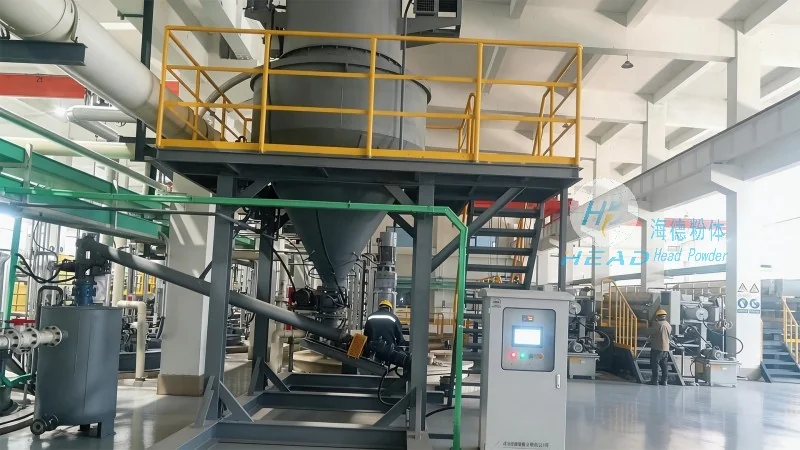
Working Principle of the Equipment
The working principle of small bag weighing and quantitative powder conveying equipment involves a series of steps that ensure accurate and efficient powder handling. The process typically begins with the placement of an empty bag on the weighing platform. The control unit then activates the feeding mechanism, which releases the powder into the bag at a controlled rate. As the powder is added, the load cells continuously monitor the weight of the bag. Once the desired weight is reached, the feeding mechanism stops, and the control unit signals the conveyor system to move the filled bag to the next stage. The bag is then either stored or transferred to the packaging line. This cycle repeats for each bag, ensuring consistent and accurate weighing and conveying of the powder.
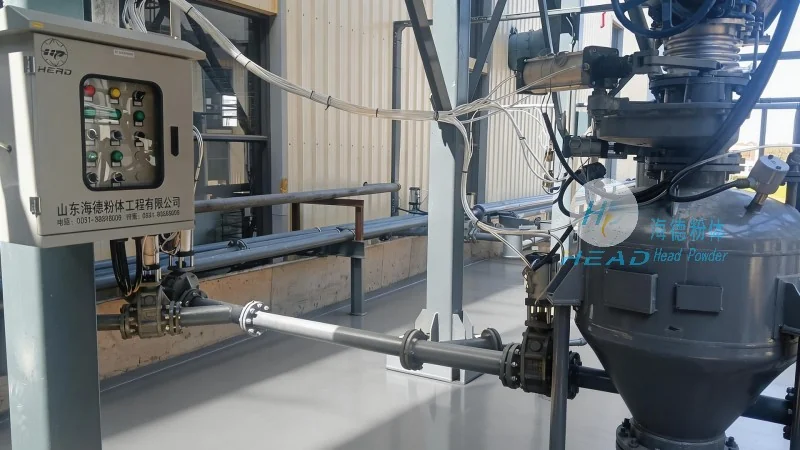
Advantages and Applications
Small bag weighing and quantitative powder conveying equipment offers several advantages that make it a preferred choice in various industries. One of the main advantages is its high accuracy in weighing, which minimizes material waste and reduces production costs. The equipment is also designed for high efficiency, with the ability to handle a large number of bags per hour, improving overall production throughput. Additionally, the equipment is versatile and can handle different types of powders, making it suitable for a wide range of applications. In the pharmaceutical industry, it is used for the accurate filling of raw materials into small bags for further processing. In the food industry, it is used for the precise packaging of food powders, ensuring product consistency and quality. In the chemical industry, it is used for the handling of chemical powders, which require strict control over dosage and purity.
Conclusion
Small bag weighing and quantitative powder conveying equipment is a critical component in modern industrial operations, providing precise and efficient handling of bulk powders. The equipment's structure and working principle are designed to ensure accurate weighing and conveying of powders, minimizing waste and maximizing productivity. With its versatility and high efficiency, it is widely used in various industries, including pharmaceuticals, food processing, and chemical manufacturing. As technology continues to advance, these equipment systems are likely to become even more sophisticated, offering further improvements in accuracy and efficiency. The equipment from Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China, exemplifies the advanced design and functionality of modern small bag weighing and quantitative powder conveying equipment.




