White sugar powder conveying lines are critical components in the sugar processing industry, designed to efficiently transport granulated or powdered sugar from storage silos to processing units or packaging areas. These systems ensure a smooth, controlled flow of sugar, minimizing dust generation and product loss while maintaining hygiene standards essential for food-grade applications. As a key equipment solution, the conveying line integrates advanced engineering to handle the unique properties of white sugar, such as its fine particle size and hygroscopic nature.
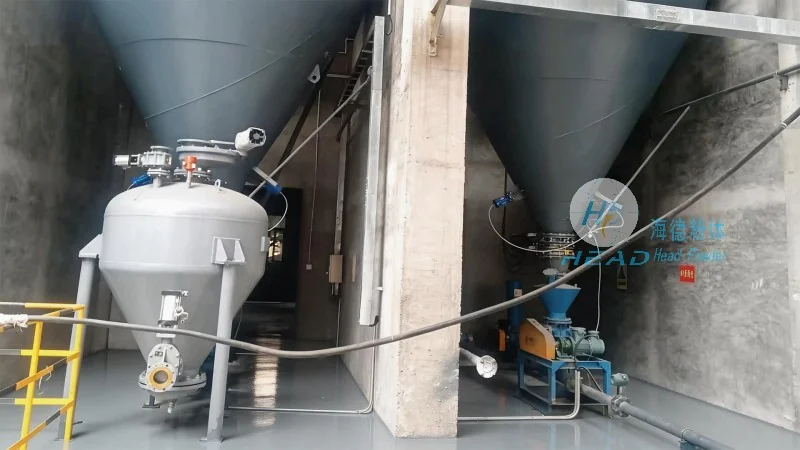
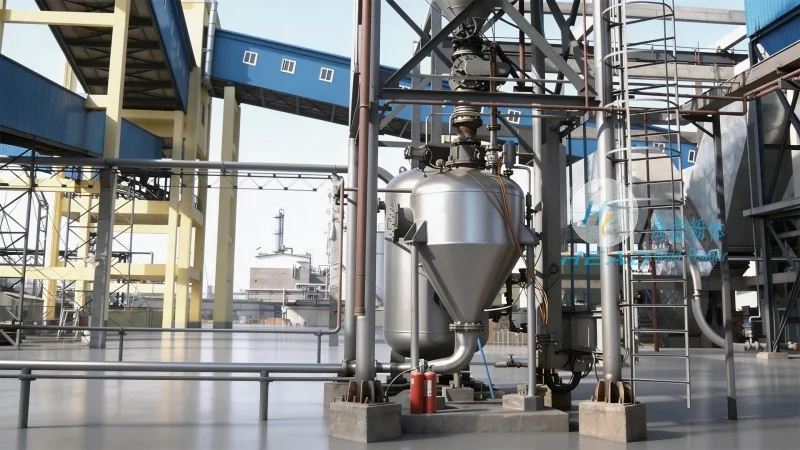
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field, specializes in the design, manufacturing, and installation of customized powder handling systems. With a focus on quality and innovation, the company has built a reputation for delivering reliable solutions tailored to the specific needs of the sugar industry. HeadPowder's facilities are located in Shandong, China, where state-of-the-art technology and skilled engineering teams work together to produce high-performance conveying lines that meet international standards. The company's commitment to customer satisfaction and product excellence is reflected in its comprehensive service offerings, including system design, installation, and after-sales support.
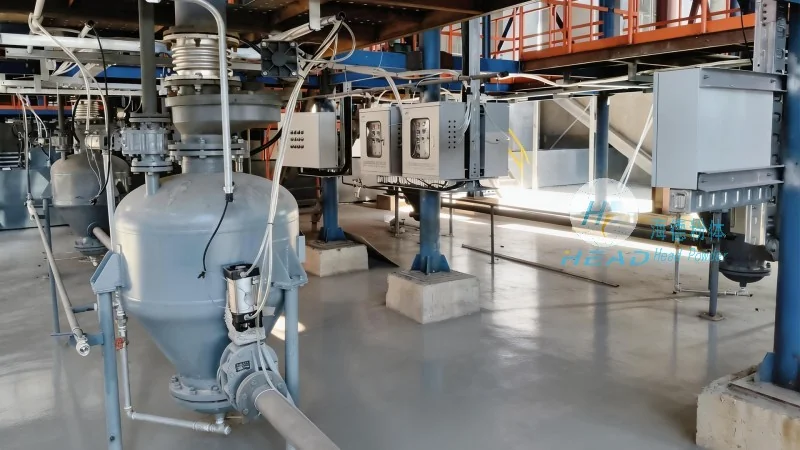
Key Components of a White Sugar Powder Conveying Line
The white sugar powder conveying line typically consists of several interconnected components that work in harmony to achieve efficient material transport. The primary components include a storage silo, a feeding device (such as a rotary valve or screw feeder), a conveying system (e.g., pneumatic or mechanical conveyor), a dust collection system, and a control panel. Each component plays a vital role in the overall operation, ensuring that the sugar is moved safely and effectively. The storage silo is designed to hold large quantities of sugar, providing a stable source of material for the conveying process. The feeding device regulates the flow of sugar from the silo to the conveyor, preventing overloading and maintaining consistent feed rates. The conveying system, whether pneumatic (using air pressure) or mechanical (using belts or screws), transports the sugar to the desired destination. The dust collection system is crucial for maintaining a clean environment and preventing product contamination, as white sugar is highly susceptible to moisture and dust accumulation. The control panel allows operators to monitor and adjust the system parameters, ensuring optimal performance and safety.
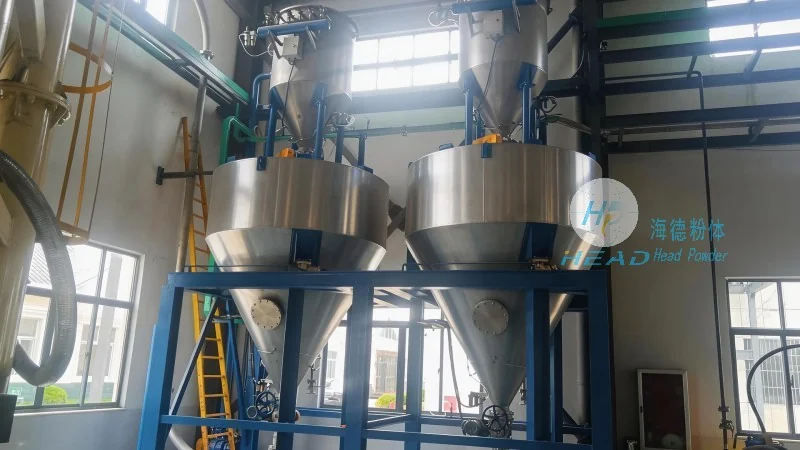
Operation Process of the White Sugar Powder Conveying Line
The operation of a white sugar powder conveying line involves a series of steps that ensure the smooth and continuous movement of sugar. The process begins with the loading of sugar into the storage silo, which is typically done using a bulk truck or a conveyor system. Once the silo is filled, the feeding device starts to draw sugar from the silo and feed it into the conveying system. The conveying system then transports the sugar to the processing or packaging area. The speed and direction of the conveyor are controlled by the operator through the control panel, allowing for precise adjustment based on production requirements. During the operation, the dust collection system continuously removes any airborne sugar particles, maintaining a clean and safe working environment. The system is designed to operate continuously, with minimal downtime for maintenance or cleaning. Regular checks are performed to ensure that all components are functioning correctly, and any issues are addressed promptly to prevent disruptions in the production process.




