Coal sand powder conveying systems are critical components in industrial processes that handle fine particulate materials like coal sand. These systems are designed to efficiently transport these materials from one location to another, ensuring smooth operation and minimal material loss. Understanding the structure and working principle of such systems is essential for optimizing performance and maintaining reliability in various industrial applications.
Overview of the Coal Sand Powder Conveying System
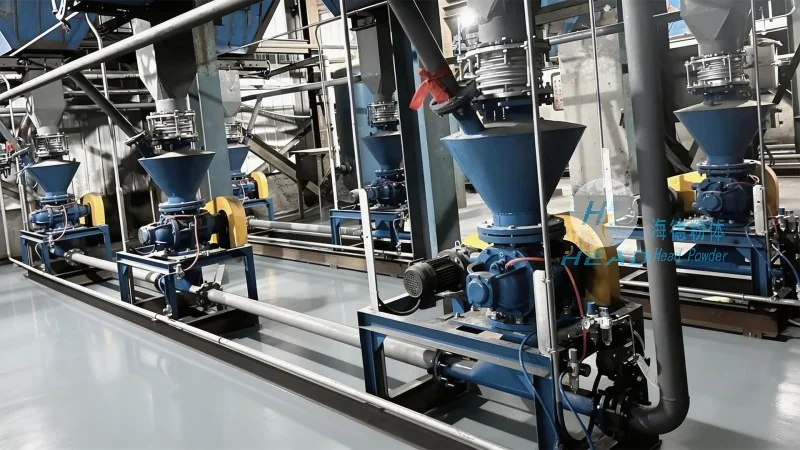
The coal sand powder conveying system, as offered by Shandong HeadPowder Engineering Co., Ltd., is engineered to handle the unique challenges associated with transporting coal sand. This system integrates advanced mechanical and pneumatic components to achieve high efficiency and durability. The design focuses on minimizing material degradation, reducing energy consumption, and ensuring consistent flow rates, which are crucial for downstream processes in coal processing and related industries.
Key Structural Components
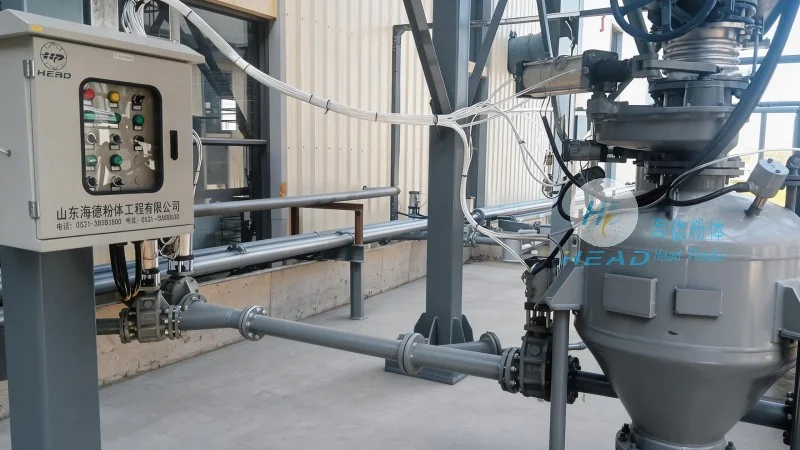
The system comprises several key components that work in tandem to facilitate the conveying process. These include the hopper, which serves as the material storage and feeding unit; the conveyor tube, which may be made of flexible or rigid materials depending on the application; the drive system, which provides the necessary force to move the material; and the control unit, which regulates the operation and monitors system performance. Each component is carefully selected and integrated to ensure optimal functionality and longevity.
Working Principle of the Conveying Process
The operation of the coal sand powder conveying system follows a systematic process. Initially, coal sand is fed into the hopper from a storage silo or processing unit. The material then flows into the conveyor tube under the influence of air pressure or mechanical force. The drive system, typically a blower or motor, generates the airflow or mechanical motion that propels the coal sand through the tube. As the material moves, it is evenly distributed and transported to the destination point, such as a storage tank or processing plant. The control unit continuously monitors parameters like pressure, flow rate, and temperature to maintain stable operation and prevent system failures.
Advantages of the System
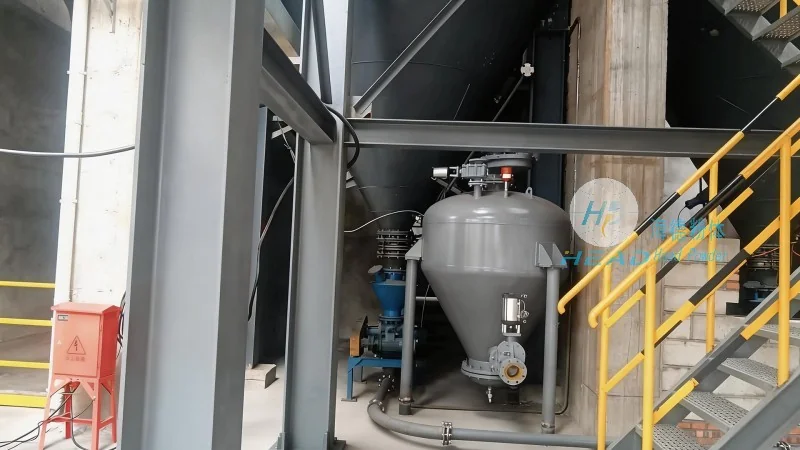
Shandong HeadPowder Engineering Co., Ltd.'s coal sand powder conveying system offers several advantages that make it a preferred choice in industrial settings. These include high conveying efficiency, which reduces downtime and increases productivity; low maintenance requirements, thanks to robust component design; and flexibility in handling different particle sizes and moisture content. The system also minimizes material contamination and degradation, which is vital for maintaining product quality in coal processing applications. Additionally, the system's compact design allows for easy integration into existing industrial setups, making it a cost-effective solution for various operational needs.
Applications and Industries
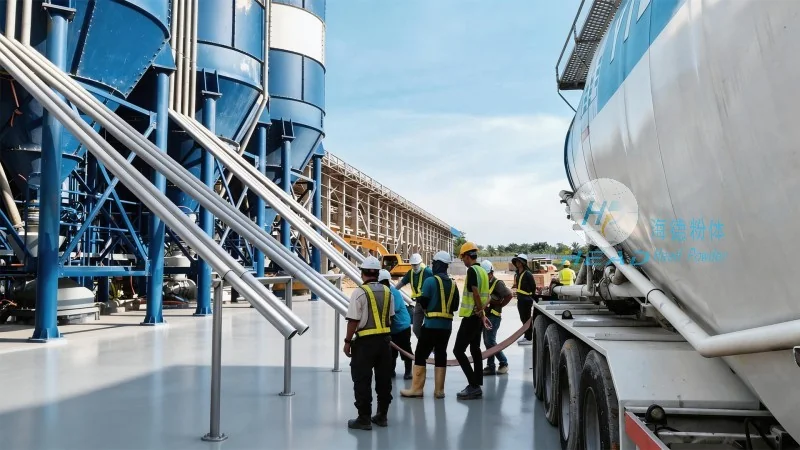
The coal sand powder conveying system is widely used in industries that rely on the handling of fine particulate materials. These include coal mining and processing, where it is used to transport coal sand from mines to processing facilities; power generation plants, which utilize coal sand for fuel; and construction material manufacturing, where it is used in the production of concrete and other building materials. The system's adaptability and reliability make it suitable for a range of applications, from small-scale operations to large industrial plants.
Conclusion
In conclusion, the coal sand powder conveying system from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated solution for the efficient and reliable transportation of coal sand. By understanding its structure and working principle, industries can optimize their operations, reduce costs, and enhance overall productivity. The system's design, components, and operational advantages make it an essential asset for any facility that handles fine particulate materials, ensuring smooth and efficient material flow throughout the production process.




