HeadPowder, a leading provider of specialized engineering solutions, specializes in the design and implementation of efficient rare earth powder conveying systems. This document provides a comprehensive overview of the system's structure and operational principles, highlighting key components and their functions to ensure optimal performance in handling rare earth powders.
Company Overview and Background
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company has established itself as a trusted partner in the rare earth industry, delivering tailored solutions that meet the stringent requirements of powder handling and material transport. With a focus on innovation and precision engineering, HeadPowder's expertise lies in creating systems that enhance productivity, ensure material integrity, and minimize operational risks.
System Overview and Core Components
The rare earth powder conveying system is a sophisticated assembly designed to transport fine powders, such as those derived from rare earth elements, with precision and reliability. The system typically comprises several critical components, each playing a vital role in the overall operation. These components include feeding mechanisms, conveying equipment, control systems, and material handling accessories. The integration of these elements ensures a seamless flow of material from the source to the destination, while maintaining the quality and purity of the rare earth powders.
Structural Design and Working Principles
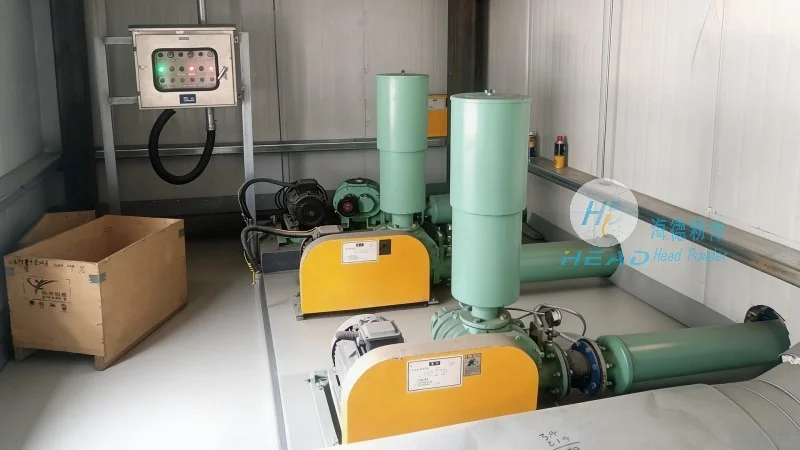
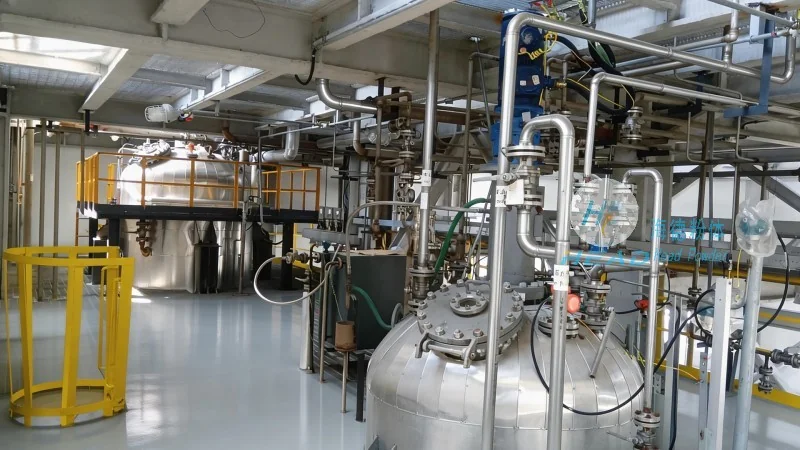
The structural design of the rare earth powder conveying system is engineered to address the unique challenges associated with handling fine, abrasive, and potentially hazardous powders. The system employs a combination of pneumatic and mechanical conveying methods, tailored to the specific characteristics of the material being transported. The feeding section, often equipped with a hopper and a rotary valve, ensures a controlled and consistent feed rate, preventing material bridging and ensuring smooth material flow. The conveying section utilizes either positive displacement blowers or vacuum pumps to create the necessary pressure or suction to move the powder through the system. The pipeline network, constructed from materials resistant to corrosion and wear, such as stainless steel or special alloys, minimizes material degradation and system downtime.
Operational Workflow and Process Flow
The operational workflow of the rare earth powder conveying system follows a systematic process that begins with material storage and ends with material delivery. Initially, the rare earth powders are stored in bulk containers or silos, from which they are transferred to the system's feeding hopper. The rotary valve then regulates the flow of material into the conveying line. The blower or vacuum pump generates the required pressure or suction, propelling the powder through the pipeline network. The system may include intermediate collection points or filters to remove any impurities or dust particles, ensuring the material remains in optimal condition. Finally, the powder is discharged into the receiving vessel or processing equipment, completing the transport cycle. The control system monitors key parameters such as pressure, flow rate, and temperature, providing real-time feedback and allowing for adjustments to maintain system efficiency and material quality.
Key Technical Features and Advantages
HeadPowder's rare earth powder conveying systems are characterized by several key technical features that contribute to their effectiveness and reliability. One of the primary advantages is the use of advanced control systems that enable precise regulation of material flow and system pressure. This ensures consistent performance and minimizes the risk of overloading or under-conveying. The system also incorporates dust collection and filtration mechanisms to maintain a clean working environment and prevent material contamination. Additionally, the modular design of the system allows for easy integration with existing production lines and facilitates maintenance and repairs. The use of high-quality materials and robust construction ensures long-term durability and reduces the need for frequent replacements or repairs.
Application and Industry Relevance
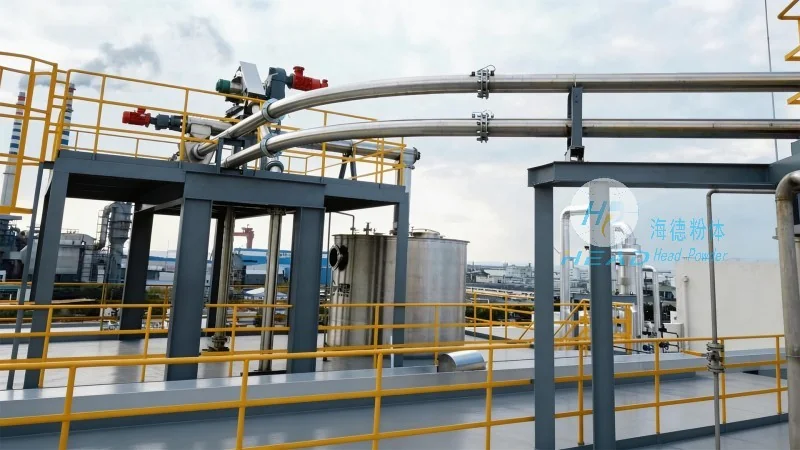
The rare earth powder conveying systems developed by HeadPowder are widely used in various applications within the rare earth processing industry. These systems are essential for transporting powders from grinding and classification stages to subsequent processing steps, such as sintering, alloying, or chemical treatment. The systems are also utilized in research and development laboratories for handling small quantities of rare earth powders with high precision. The reliability and efficiency of these systems contribute to improved productivity and cost-effectiveness in rare earth production, making them a critical component of modern rare earth processing facilities.
Conclusion and Future Developments
In conclusion, the rare earth powder conveying system offered by Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated and reliable solution for the efficient handling of rare earth powders. The system's design, incorporating advanced components and control mechanisms, ensures optimal performance while maintaining the quality and integrity of the material. As the demand for rare earth materials continues to grow, the importance of efficient powder conveying systems becomes increasingly evident. HeadPowder remains committed to innovation and excellence, continuously developing and improving its systems to meet the evolving needs of the industry. By leveraging its expertise and experience, HeadPowder provides customers with solutions that enhance operational efficiency, reduce costs, and ensure compliance with industry standards.




