Carbon black and coal powder are critical raw materials across multiple industrial sectors, including rubber manufacturing, plastic production, and energy generation. The efficient and reliable transportation of these fine powders is paramount for maintaining production efficiency, ensuring product quality, and optimizing operational costs. This article provides a comprehensive overview of the carbon black and coal powder pneumatic conveying system, detailing its structural components, operational principles, and practical applications.
Overview of the Pneumatic Conveying System
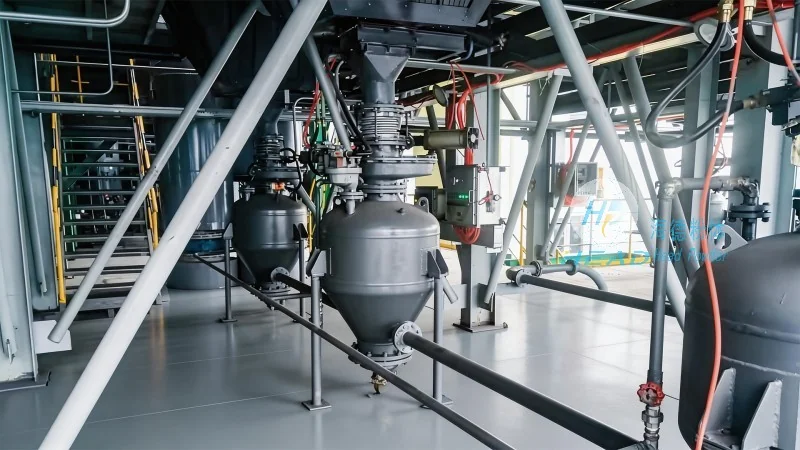
The carbon black and coal powder pneumatic conveying system is a specialized engineering solution designed to transport fine particulate materials through a pipeline using air or gas as the conveying medium. Unlike traditional mechanical conveying methods, this system offers significant advantages such as reduced material degradation, lower maintenance requirements, and enhanced safety during handling of potentially hazardous powders. It is widely adopted in industries where dust control and precise material handling are essential.
Key Structural Components and Design Considerations
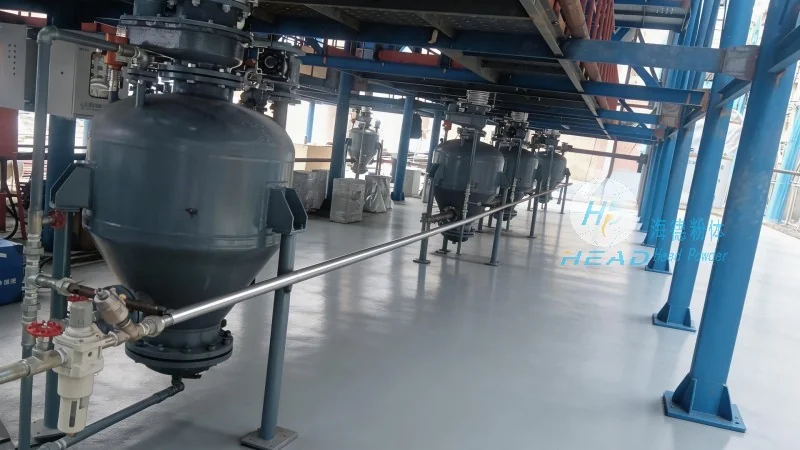
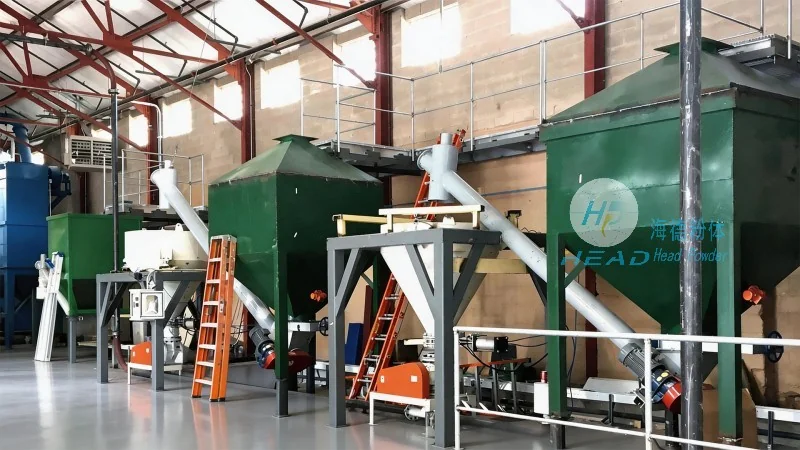
The system comprises several interdependent components, each engineered to ensure optimal performance and durability. The primary components include the material hopper, feeding mechanism, air compressor unit, conveying pipeline, and receiving hopper. The material hopper is constructed to store the carbon black or coal powder, providing a consistent feed source. The feeding device, typically a rotary valve or screw feeder, regulates the flow rate of the powder into the pipeline, preventing overloading and ensuring smooth operation. The air compressor generates the necessary pressure and airflow to suspend and transport the powder particles through the pipeline. The conveying pipeline is usually made of stainless steel or other corrosion-resistant materials to minimize material buildup and ensure long-term reliability. The receiving hopper collects the conveyed powder at the destination point, completing the material transfer process.
Operational Principle and Flow Dynamics
The core operational principle of the pneumatic conveying system is based on fluidization and suspension of powder particles within the air stream. When the air compressor provides a high-pressure airflow, it creates a flow within the pipeline that lifts and moves the powder particles. The velocity of the air must be sufficient to overcome gravitational forces and frictional resistance between particles, ensuring stable and continuous conveying. The system operates in either dense phase or dilute phase modes, depending on the system design and operating conditions. In dense phase conveying, the air velocity is lower, resulting in a higher powder concentration in the pipeline, which minimizes particle breakage and reduces pressure drop. Dilute phase conveying, on the other hand, uses higher air velocities to transport the powder in a more dispersed state, suitable for longer distances or larger volumes.
Advantages and Industrial Applications
The carbon black and coal powder pneumatic conveying system offers numerous benefits for industrial operations. It provides a clean and dust-free conveying method, reducing the risk of contamination and improving product purity. The system is highly flexible, allowing easy integration into existing production lines and modifications to accommodate different powder types or conveying distances. In the rubber industry, this system is commonly used to transport carbon black to mixing machines, ensuring uniform dispersion and enhancing the final product's mechanical properties. In the energy sector, it is employed to transport coal powder to boilers for combustion, improving combustion efficiency and reducing emissions. The system's ability to handle fine powders with high efficiency makes it a preferred choice in various industrial settings where material handling demands precision and reliability.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
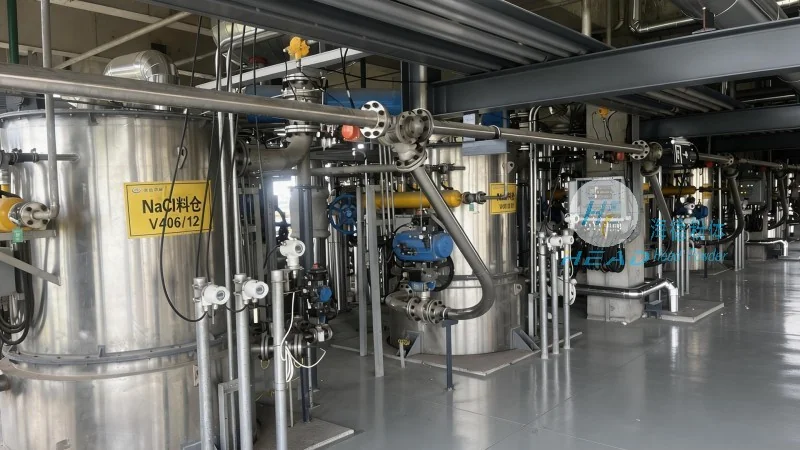
HeadPowder, a leading manufacturer specializing in carbon black and coal powder pneumatic conveying systems, is dedicated to delivering high-quality and reliable equipment for industrial applications. With years of experience in the field, HeadPowder has developed advanced technologies and innovative solutions to meet the diverse needs of clients worldwide. The company's headquarters is located in Shandong, China, where it has established a robust research and development team focused on continuous improvement and innovation. HeadPowder's products are designed to meet international standards and are widely recognized for their durability, efficiency, and user-friendly operation. By choosing HeadPowder's pneumatic conveying systems, industries can enhance their production processes, reduce operational costs, and ensure compliance with environmental regulations. HeadPowder's commitment to quality and customer satisfaction has made it a trusted partner for businesses seeking efficient material handling solutions.




