Positive pressure dense phase powder pneumatic conveying systems represent a sophisticated technology in material handling, designed to efficiently transport bulk powders through a pipeline under pressure. This system is particularly effective for applications requiring high reliability and minimal product degradation, making it a preferred choice in various industrial sectors. The core of this technology lies in its ability to maintain a dense phase flow, which enhances the conveying efficiency and reduces the risk of particle segregation or degradation during transport.
Principle of Operation
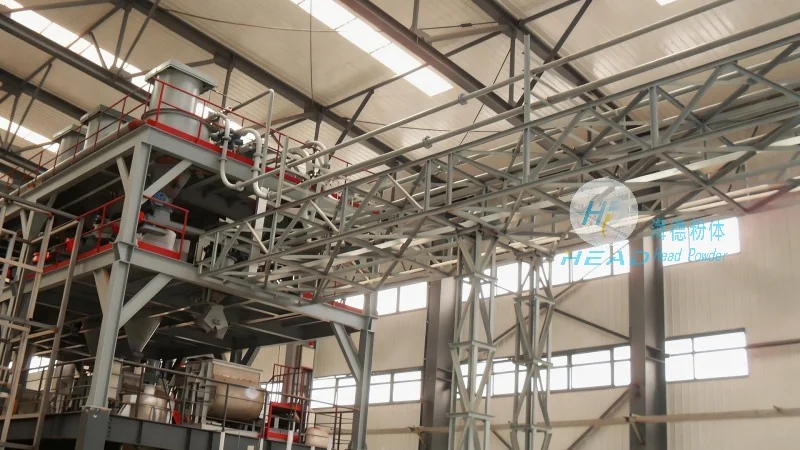
The fundamental principle of a positive pressure dense phase powder pneumatic conveying system is based on the generation of a high-pressure air stream that propels the powder particles through a pipeline. Unlike negative pressure systems, which draw material into the system, positive pressure systems force the material through the pipeline, ensuring consistent flow rates and preventing backflow. The system typically consists of a blower or compressor that supplies compressed air, a hopper or feeder to introduce the powder, and a pipeline network that delivers the material to the destination. The dense phase operation is achieved by controlling the air-to-solid ratio, ensuring that the powder particles are suspended in a dense cloud rather than a dilute suspension. This dense phase reduces the velocity of the material, minimizing particle impact and abrasion, which is crucial for delicate or abrasive powders.
Key Components and Their Functions
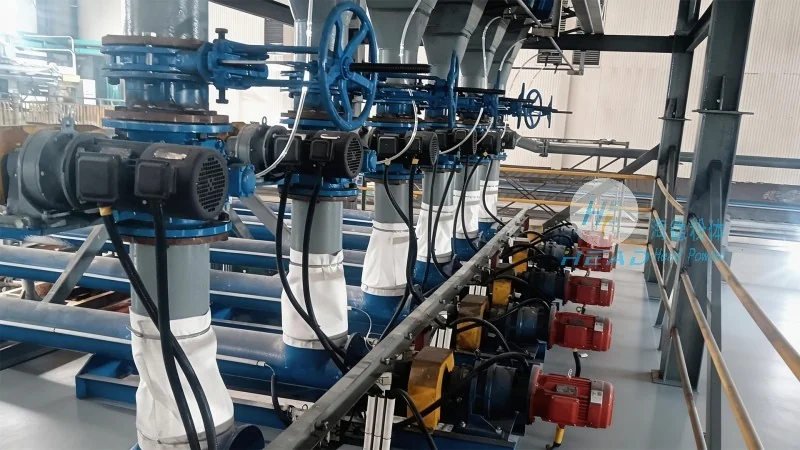
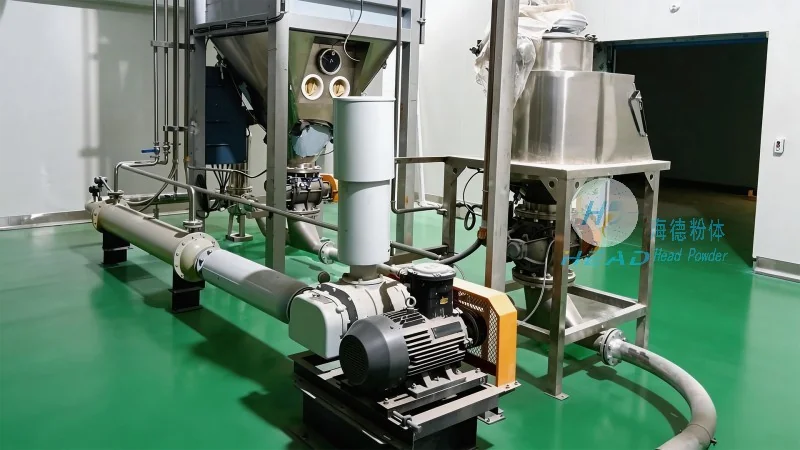
Several critical components work in tandem to ensure the efficient operation of a positive pressure dense phase powder pneumatic conveying system. The first is the air compressor or blower, which generates the necessary pressure to move the material. This component is typically selected based on the required flow rate and pressure, with options ranging from rotary lobe blowers to centrifugal compressors. The second key component is the feeder or hopper, which introduces the powder into the system. Feeding mechanisms such as rotary valves, screw feeders, or vibratory feeders are used to control the flow rate and prevent blockages. The pipeline system, often made of stainless steel or other corrosion-resistant materials, is designed to withstand the pressure and abrasion from the powder. Additionally, the system includes check valves and filters to prevent backflow and maintain air quality. The control system, which may include sensors and automation, monitors the pressure, flow rate, and other parameters to ensure optimal operation.
Working Scene Characteristics and Applications
The working scene characteristics of positive pressure dense phase powder pneumatic conveying systems are tailored to meet the demands of various industrial applications. These systems are commonly used in industries such as pharmaceuticals, food processing, chemical manufacturing, and mining, where the transport of powders requires high purity and minimal contamination. The dense phase operation ensures that the powder remains intact during transport, which is essential for products that are sensitive to moisture, temperature, or mechanical stress. For example, in pharmaceutical applications, the system can transport active pharmaceutical ingredients (APIs) without degradation, maintaining their efficacy. In food processing, the system can handle powders like flour, sugar, or spices, ensuring that the product remains fresh and free from contamination. The system's ability to handle abrasive materials, such as minerals or metal powders, makes it suitable for mining and metal processing industries, where traditional conveyor belts may wear out quickly.
Advantages and Benefits
Positive pressure dense phase powder pneumatic conveying systems offer several advantages over traditional material handling methods. One of the primary benefits is the ability to transport powders over long distances with minimal energy consumption. The dense phase operation reduces the air volume required, making the system more energy-efficient compared to dilute phase systems. Another advantage is the reduced risk of product degradation, as the low velocity and dense flow minimize particle impact and abrasion. This is particularly important for delicate or high-value products. The system also provides a closed-loop operation, which prevents dust emissions and maintains a clean working environment, enhancing safety and compliance with environmental regulations. Additionally, the system's flexibility allows for easy integration with existing production lines, and the modular design enables scalability to accommodate varying production volumes.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
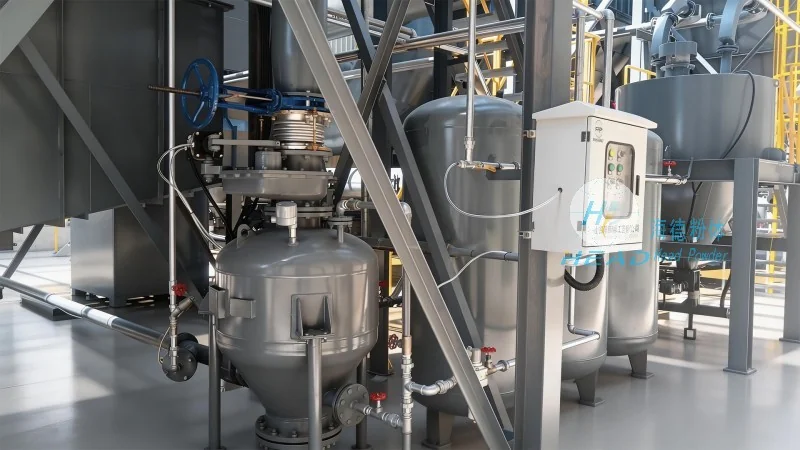
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of advanced material handling solutions, including positive pressure dense phase powder pneumatic conveying systems. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. HeadPowder's team of engineers and technicians brings extensive experience in designing and manufacturing customized conveying systems tailored to the specific needs of each client. The company's facilities, located in Shandong, China, are equipped with state-of-the-art technology and quality control measures to ensure that every product meets the highest standards. HeadPowder's commitment to research and development ensures that its systems incorporate the latest advancements in pneumatic conveying technology, providing clients with reliable and efficient solutions for their material handling challenges.




