HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of air-pneumatic conveying equipment tailored for handling quartz sand particle materials. This equipment is engineered to efficiently transport fine to medium-sized granular materials like quartz sand through an air-driven system, offering a solution that minimizes material degradation and ensures consistent flow rates. The following sections will delve into the fundamental principles of this technology and explore the specific working scene characteristics that make it an ideal choice for various industrial applications.
Principle of Air-Pneumatic Conveying for Quartz Sand
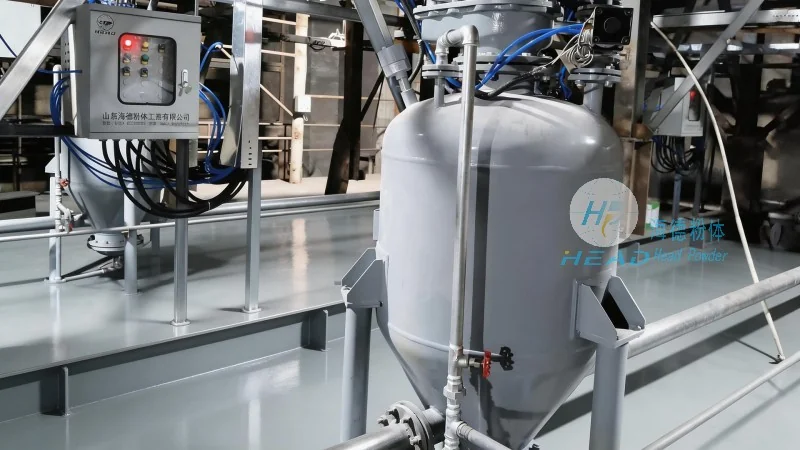
The core principle of air-pneumatic conveying for quartz sand particle materials involves the use of a pressurized or vacuum air stream to move the material through a pipeline. In a typical system, the quartz sand is fed into a hopper or feeder, where it is then introduced into the conveying line. The air, either supplied by a blower or generated by a vacuum pump, creates a flow that lifts and transports the particles. This method relies on the interaction between the air velocity and the particle size, density, and shape to achieve effective transport. The equipment is designed to maintain optimal air-to-material ratios to prevent blockages and ensure smooth operation. The use of air as the conveying medium also allows for the integration of dust collection systems, enhancing safety and compliance with environmental regulations.
Working Scene Characteristics of the Equipment
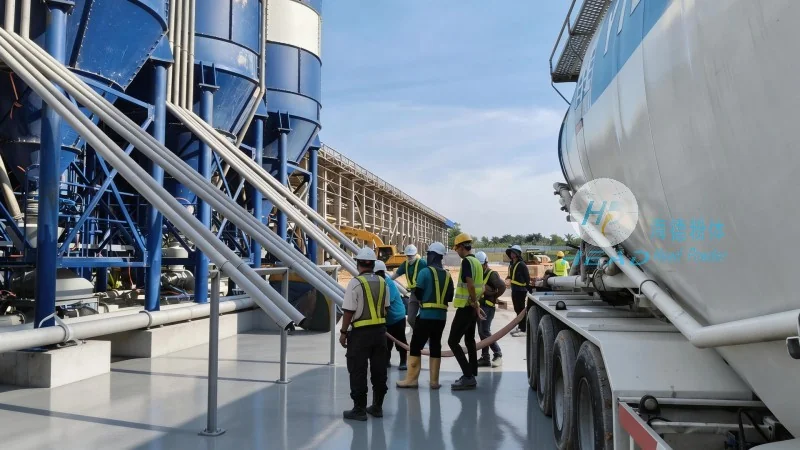
The air-pneumatic conveying equipment for quartz sand exhibits several key characteristics that make it suitable for diverse working environments. Firstly, it offers a flexible and compact design, which is advantageous in spaces where traditional bulk handling systems may not fit. The system can be configured in various layouts, including vertical, horizontal, or a combination of both, allowing for adaptation to different plant layouts. Secondly, the equipment provides a dust-free operation, which is critical in industries where air quality and worker safety are paramount. By containing the material within the pipeline and using filtration systems, the risk of dust exposure is significantly reduced. Thirdly, the system is capable of handling a wide range of particle sizes, from fine powders to coarse granules, making it versatile for different quartz sand applications. This adaptability ensures that the equipment can be used in both production and processing stages, from raw material transport to finished product handling. Additionally, the equipment operates with low maintenance requirements, as the components are designed to withstand the abrasive nature of quartz sand, reducing downtime and operational costs.
Application Scenarios and Industry Integration
The working scene characteristics of the air-pneumatic conveying equipment for quartz sand make it a valuable asset in several industrial sectors. In the mining and quarrying industry, the equipment is used to transport raw quartz sand from storage silos to processing plants, ensuring a continuous supply of material. The efficient conveying system minimizes material handling time and reduces the risk of material loss or contamination. In the glass manufacturing industry, quartz sand is a primary raw material for glass production, and the air-pneumatic system ensures a consistent and clean supply of sand to the melting furnaces. This contributes to the quality and uniformity of the final glass products. Furthermore, in the construction materials industry, the equipment is utilized in the production of concrete and other building materials, where precise control of sand particle size and quality is essential. The ability to maintain consistent flow rates and particle characteristics enhances the performance of the end products. The equipment's ability to operate in both continuous and batch modes also makes it suitable for various production schedules, adapting to the needs of different manufacturing processes.
Advantages and Practical Considerations
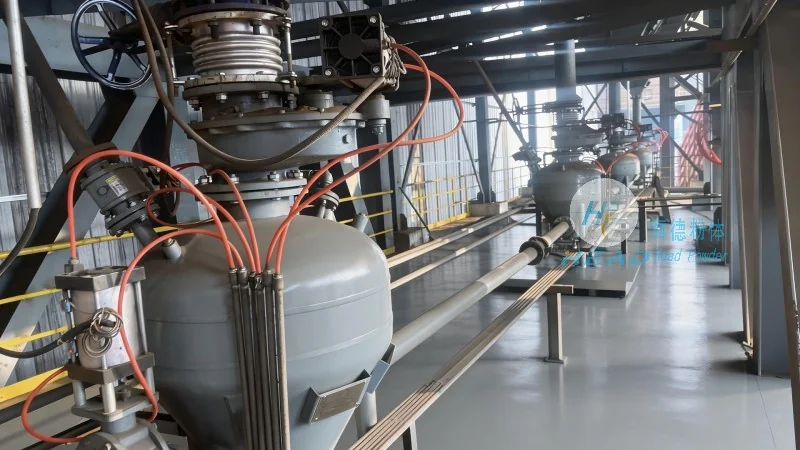
When considering the implementation of air-pneumatic conveying equipment for quartz sand, several advantages and practical considerations should be taken into account. The primary advantage is the reduction in labor costs associated with manual handling of bulk materials. The automated system minimizes the need for manual loading and unloading, improving operational efficiency. Additionally, the equipment reduces material waste by minimizing spillage and loss during transport. From a safety perspective, the enclosed system prevents dust explosions and provides a safer working environment. However, practical considerations include the initial investment cost, which may be higher than traditional conveyor systems. The system also requires regular maintenance of the air filtration and pipeline components to ensure optimal performance. The selection of the appropriate air velocity and pressure is crucial to prevent material degradation and ensure efficient transport. Proper sizing of the equipment based on the material flow rate and pipeline length is essential to avoid system inefficiencies or blockages. Overall, the air-pneumatic conveying equipment offers a reliable and efficient solution for handling quartz sand particle materials, aligning with the operational needs of modern industrial facilities.




