HeadPowder, a prominent enterprise headquartered in Shandong, China, is dedicated to providing innovative solutions for material handling. The company specializes in the design and manufacturing of industrial equipment, with a particular focus on pneumatic conveying systems. Among their offerings is the rotary lobe blower material pneumatic conveying machine, a technology that has revolutionized the way bulk materials are transported in various industries. This article delves into the core principles of this equipment and highlights the key operational environments where it excels.
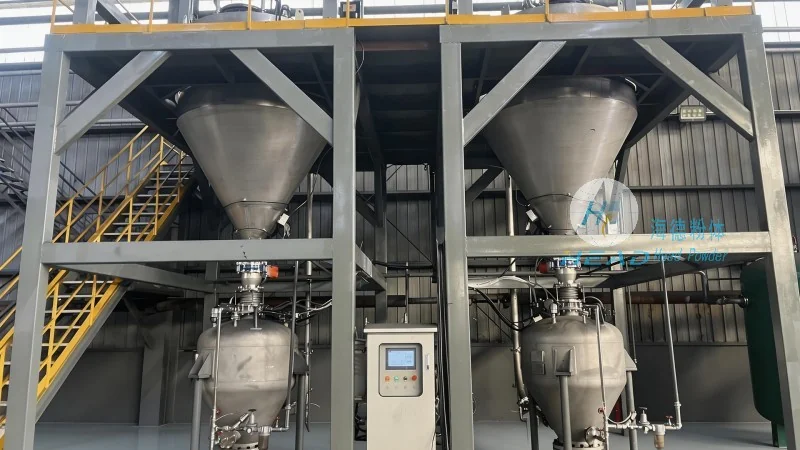
The Fundamental Principle of Rotary Lobe Blower Material Pneumatic Conveying
The rotary lobe blower material pneumatic conveying machine operates on the principle of positive displacement. Two interlocking lobed rotors rotate synchronously within a robust casing. As the rotors turn, they create a series of sealed pockets that trap air and the material to be conveyed. The continuous rotation of these pockets forces the material and air from the inlet to the outlet, ensuring a consistent flow. This mechanism is highly efficient for transporting dry bulk materials, as it maintains a stable pressure and minimizes material degradation. The sealed design also prevents air leakage, which is crucial for maintaining the system’s performance and energy efficiency.
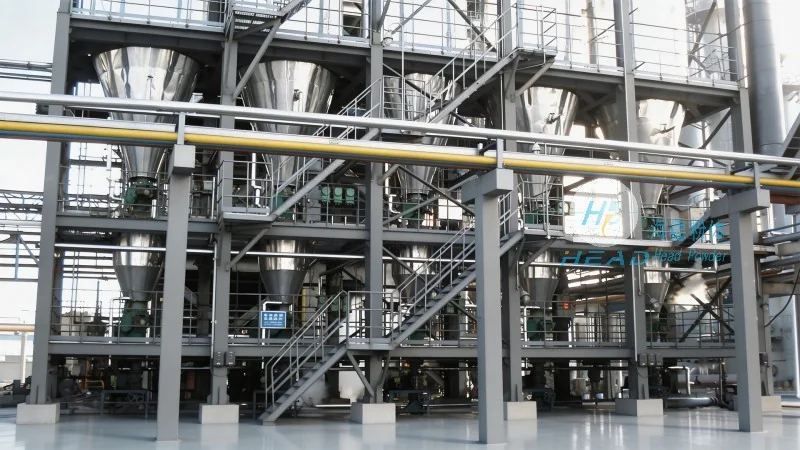
Key Working Scene Characteristics and Application Scenarios
The rotary lobe blower material pneumatic conveying machine is engineered for versatility across diverse industrial applications. Its ability to handle a wide variety of materials, including powders, granules, and fine particles, makes it suitable for sectors such as food processing, pharmaceuticals, and chemical manufacturing. The system’s compact footprint and low maintenance requirements make it an ideal choice for facilities with limited space or those seeking cost-effective solutions. Additionally, the machine’s adaptability to both positive and negative pressure modes enhances its functionality, allowing it to serve dual purposes, such as conveying materials and acting as a dust collection device in some setups. This flexibility makes it a reliable solution for industries that require efficient and reliable material transport.
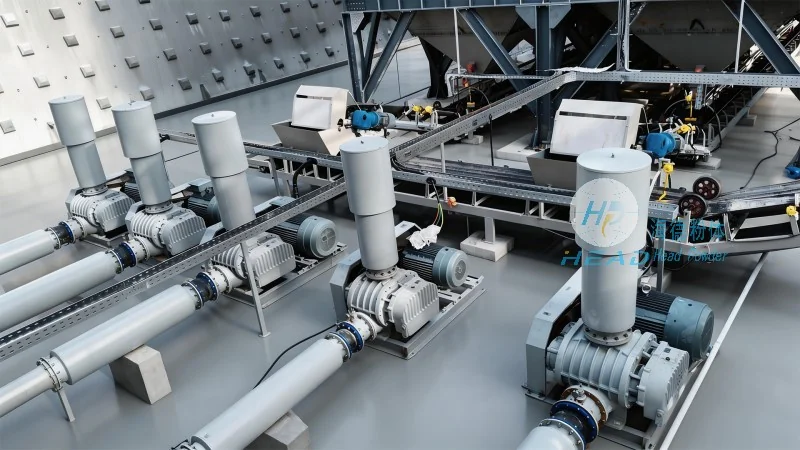
Operational Advantages in Diverse Environments
One of the standout features of the rotary lobe blower material pneumatic conveying machine is its ability to operate in various environmental conditions. The sealed design protects the material from contamination and the environment from dust, making it suitable for cleanroom applications in the pharmaceutical and food industries. The system’s low noise levels and minimal vibration also contribute to a safer working environment, reducing the risk of accidents and improving employee comfort. Furthermore, the machine’s energy efficiency, due to its positive displacement mechanism, helps reduce operational costs over time, making it a sustainable choice for long-term use.
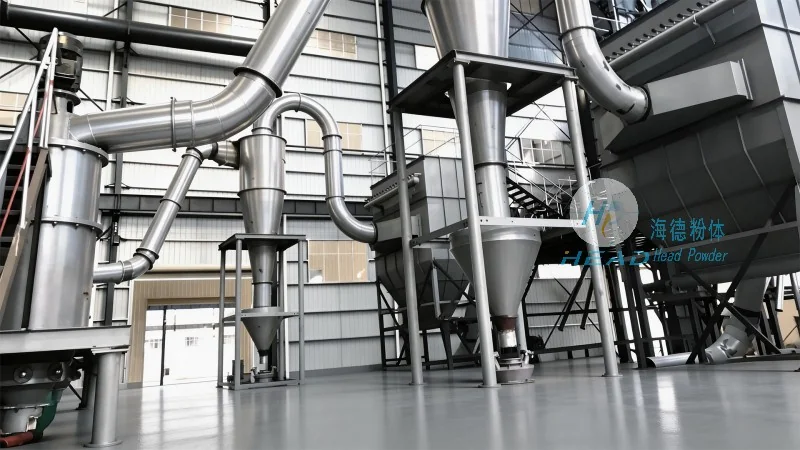
Conclusion and Company Overview
HeadPowder, with its headquarters in Shandong, China, continues to lead the industry in providing high-quality rotary lobe blower material pneumatic conveying machines. By leveraging advanced engineering and rigorous quality control, the company ensures that its products meet the demanding requirements of modern industrial applications. The principles and characteristics discussed in this article underscore the importance of this technology in enhancing material handling efficiency and reliability across various sectors. As industries evolve, the rotary lobe blower material pneumatic conveying machine remains a vital component in achieving optimal material transport solutions.




