Gray silo material conveying systems represent a critical component in modern industrial material handling, designed to efficiently transport bulk materials within storage and processing facilities. These systems are integral to optimizing workflow, enhancing operational efficiency, and ensuring consistent material flow in various industrial applications. The technology behind gray silo conveying leverages advanced engineering principles and robust mechanical designs to meet the demands of diverse material types and processing environments.
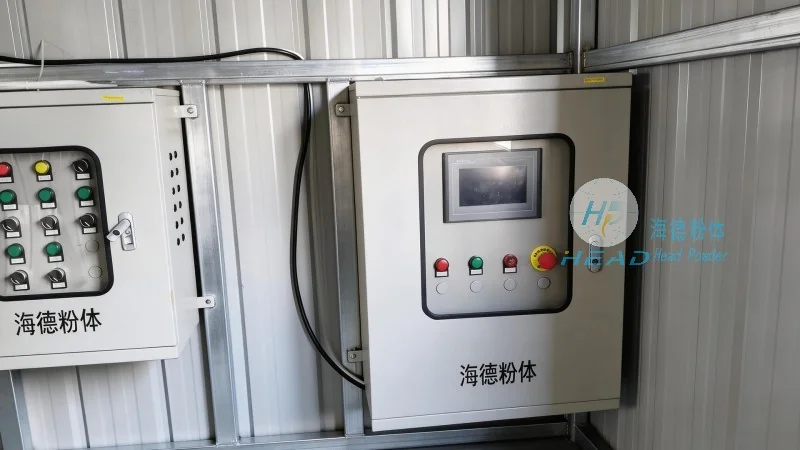
Core Principles of Gray Silo Material Conveying
The fundamental principle of gray silo material conveying revolves around the use of specialized equipment, such as screw conveyors, bucket elevators, and pneumatic systems, to move bulk materials from storage silos to processing units or other operational areas. The design of these systems prioritizes factors like material compatibility, flow rate control, and structural integrity to ensure reliable performance. For instance, screw conveyors utilize rotating helical screws to push materials forward, while bucket elevators employ buckets attached to a chain or belt to lift and transport materials vertically. Pneumatic conveying systems, on the other hand, use compressed air to transport materials through pipes, offering flexibility in horizontal and vertical transport. The choice of conveying method depends on the material's properties, such as particle size, moisture content, and bulk density, as well as the specific requirements of the application.
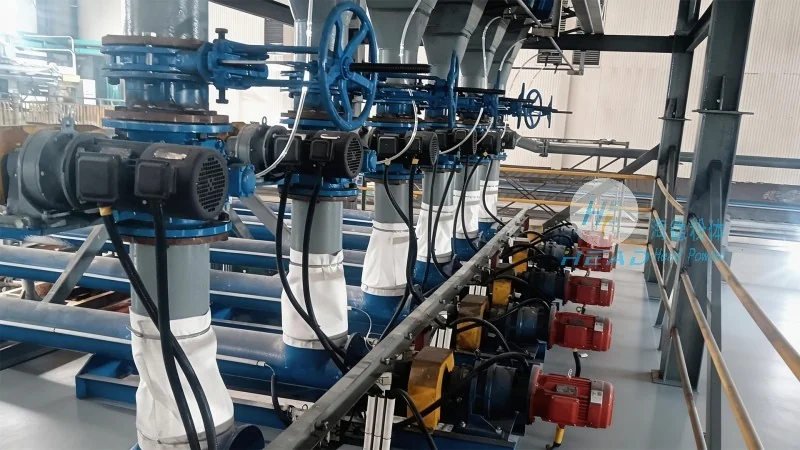
Working Scene Characteristics of Gray Silo Material Conveying
Gray silo material conveying systems are commonly employed in a wide range of industrial settings, including chemical plants, food processing facilities, pharmaceutical manufacturing sites, and mining operations. Each working scene presents unique challenges and requirements that influence the design and implementation of the conveying system. In chemical plants, for example, the systems must handle potentially hazardous materials while maintaining strict safety protocols. Food processing facilities require hygienic designs to prevent contamination and ensure compliance with food safety regulations. Pharmaceutical manufacturing sites demand high-purity conveying solutions to meet stringent quality standards. Mining operations often involve large-scale material handling, where the systems must withstand heavy loads and harsh environmental conditions. The working scene characteristics also include considerations like space constraints, integration with existing infrastructure, and the need for automated control systems to enhance operational efficiency.
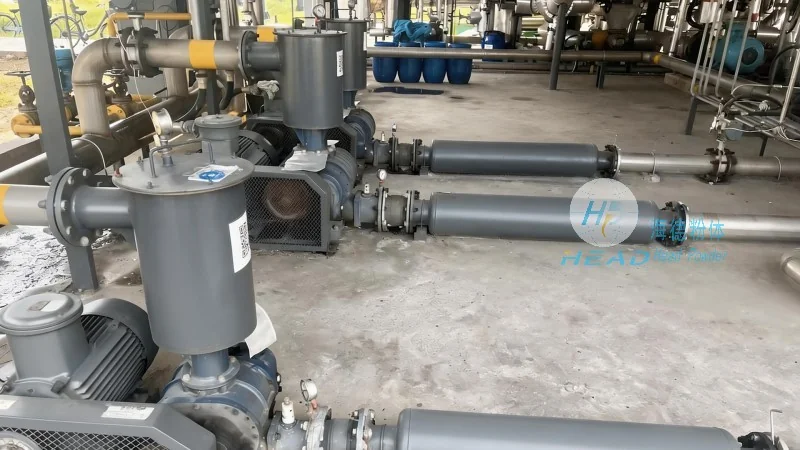
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of industrial material handling solutions, specializing in the design, manufacturing, and installation of gray silo material conveying systems. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. The company's expertise lies in tailoring conveying systems to meet the specific needs of clients, ensuring optimal performance and durability in diverse industrial environments. HeadPowder's team of experienced engineers and technicians work closely with clients to understand their operational requirements and develop customized solutions that enhance productivity and reduce downtime.
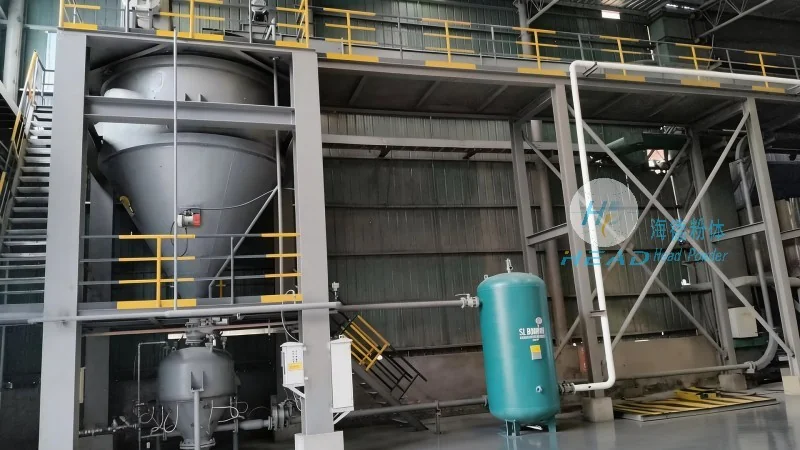
Address and Contact Information
HeadPowder is headquartered in Shandong, China, with a physical address that reflects the company's roots in the region. The company's location in Shandong provides access to a skilled workforce and robust industrial infrastructure, supporting its manufacturing and service operations. This regional presence allows HeadPowder to serve clients effectively while maintaining close ties to the local industrial community. The company's commitment to quality and customer satisfaction is evident in its operations, which are conducted in accordance with industry best practices and international standards.




