Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier specializing in material handling solutions. The company is headquartered in Shandong, China, and has established itself as a key player in the industry with a focus on innovative and efficient systems for various bulk material transport applications.
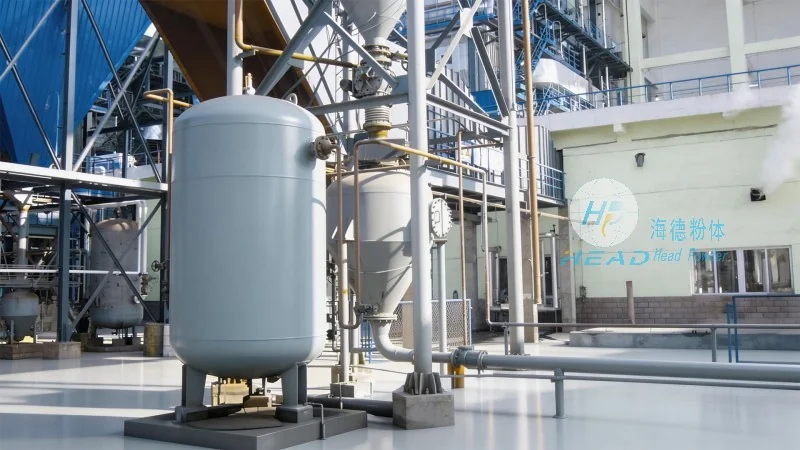
Overview of Wheat Bran Material Handling Systems
Wheat bran material handling systems are specialized equipment designed to efficiently transport and process wheat bran, a byproduct of the wheat milling process. These systems are crucial in food processing and agricultural industries, where the handling of bulk materials like wheat bran requires reliable and effective solutions. The systems are engineered to handle the unique characteristics of wheat bran, such as its light weight, irregular shape, and tendency to create dust, ensuring safe and efficient material movement.
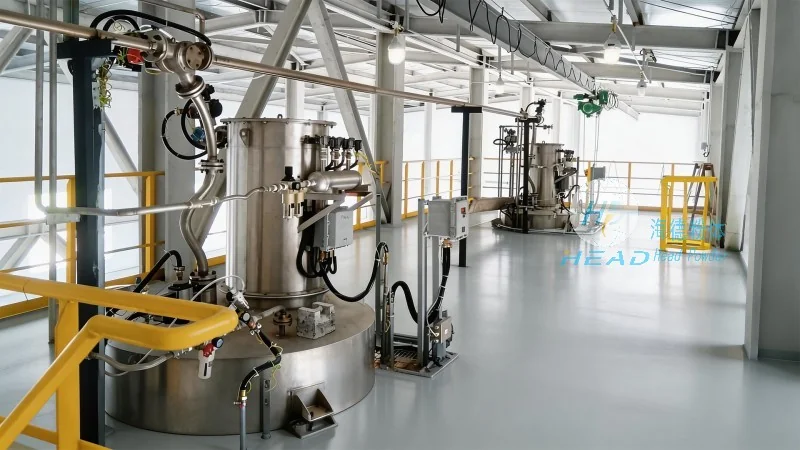
Detailed Working Principle of the System
The working principle of a typical wheat bran material handling system involves several key components and processes. The system typically starts with a feeding mechanism, which may include a hopper or a conveyor to collect the wheat bran from the source. The material is then transferred to a primary conveyor, often a belt conveyor or a screw conveyor, which moves the bran along the designated path. To ensure smooth operation, the system may incorporate a series of intermediate conveyors or transfer points, allowing for changes in direction or elevation. The final stage involves the discharge of the wheat bran into a storage bin or processing unit. The entire process is controlled by a centralized system, which monitors the flow rate, pressure, and other parameters to maintain optimal performance. The system's design ensures minimal material loss and maximum efficiency, making it suitable for high-volume operations.
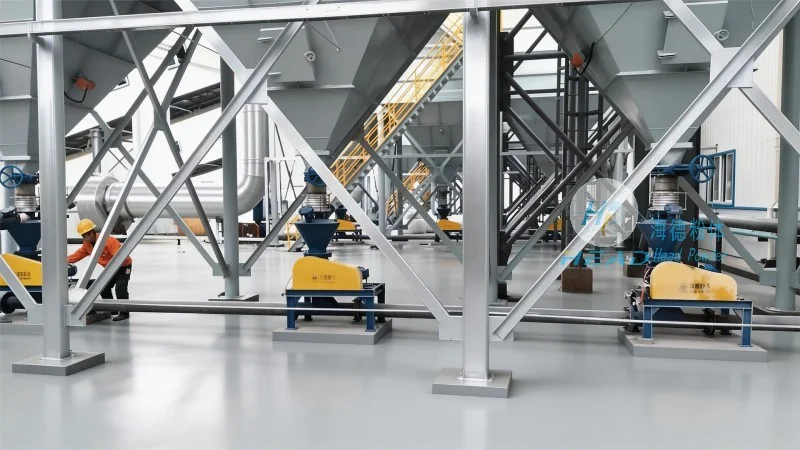
Key Features and Characteristics
Wheat bran material handling systems from HeadPowder are characterized by several notable features that enhance their performance and reliability. One of the primary features is the use of high-quality materials in the construction of the components, such as stainless steel for the conveyor belts and housing, which provides durability and resistance to corrosion. The systems are also equipped with advanced control systems, including sensors and automation controls, that allow for precise monitoring and adjustment of the material flow. Another important feature is the integration of dust control measures, such as dust collection systems and sealed enclosures, which help to maintain a clean and safe working environment. Additionally, the systems are designed for easy maintenance and cleaning, with accessible components and simple operation procedures. These features collectively contribute to the overall efficiency and longevity of the system.
Technical Advantages and Performance
The technical advantages of the wheat bran material handling systems from HeadPowder are evident in their ability to handle the specific challenges associated with wheat bran. The systems are engineered to minimize the risk of material blockages and ensure consistent flow rates, even with varying material conditions. The use of variable speed drives allows for adjustments to the conveyor speed based on the load, optimizing energy consumption and reducing wear on the components. The systems also feature robust safety features, including emergency stop buttons and overload protection, which ensure the safety of the operators and the integrity of the material. Furthermore, the systems are designed to be scalable, allowing for easy expansion or modification to accommodate changing production needs. These technical advantages make the systems a reliable choice for businesses in the food processing and agricultural sectors.
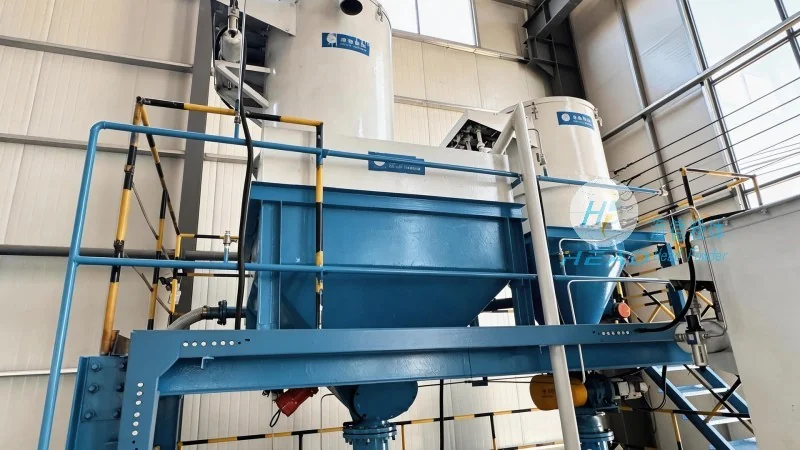
Application Scenarios and Industry Use
Wheat bran material handling systems are widely used in various industries, particularly in the food processing and agricultural sectors. In the food industry, these systems are commonly used in flour mills and grain processing plants to transport wheat bran to storage facilities or processing units. The systems are also used in animal feed production, where wheat bran is a key ingredient in feed formulations. In the agricultural sector, the systems are utilized in grain handling facilities to move wheat bran from storage silos to processing equipment. The systems are also suitable for other bulk material handling applications, such as in the chemical and pharmaceutical industries, where similar material characteristics are present. The versatility of the systems makes them a valuable asset for businesses looking to improve their material handling processes and increase operational efficiency.




