For industrial applications that require efficient material handling and air filtration, the pulse jet dust collector pneumatic conveying machine has emerged as a critical solution. This equipment combines advanced dust collection technology with pneumatic conveying capabilities, offering a comprehensive approach to managing particulate matter and transporting bulk materials. Understanding its working principle and key features is essential for industries such as mining, chemical processing, and food processing, where maintaining air quality and optimizing material transport are paramount.
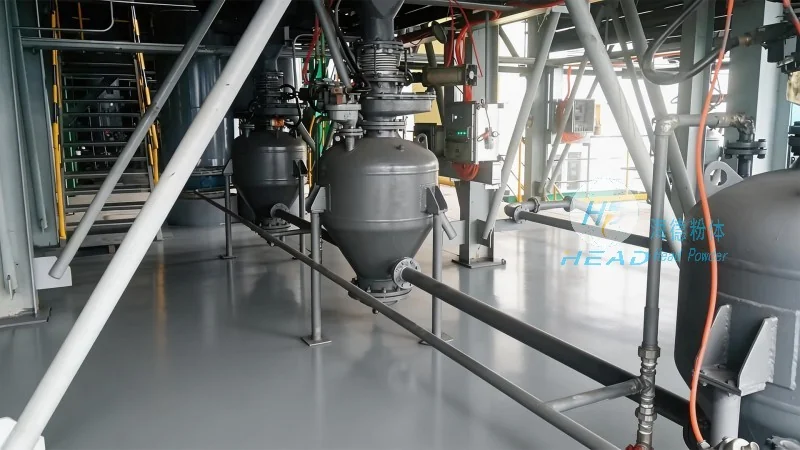
Working Principle of the Pulse Jet Dust Collector Pneumatic Conveying Machine
The pulse jet dust collector pneumatic conveying machine operates by integrating two core functions: dust filtration and material transport. The dust collector component uses a pulse jet system to clean filter bags, ensuring consistent air filtration efficiency. Simultaneously, the pneumatic conveying system utilizes compressed air to move bulk materials from a source to a destination. The machine's design allows for the simultaneous execution of these functions, making it a versatile solution for applications where both filtration and transport are required.
At the heart of the dust collector is the pulse jet mechanism. Compressed air is periodically released into the filter bags, creating a high-velocity pulse that dislodges accumulated dust particles. This process, known as reverse air cleaning, prevents filter clogging and maintains low pressure drop across the system. The compressed air is typically supplied by an external air compressor, and the timing and duration of the pulses are controlled by a programmable logic controller (PLC) to optimize cleaning efficiency.
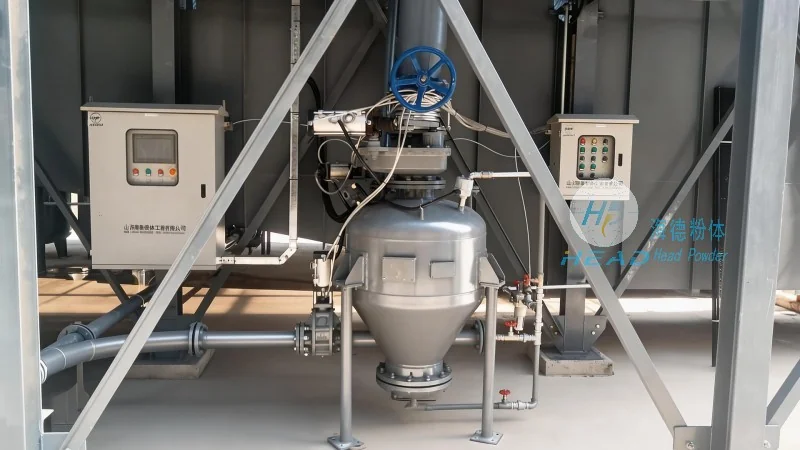
The pneumatic conveying section of the machine uses a positive pressure system, where compressed air is introduced at the material feed point to create a flow that transports the material through a pipeline. The conveying line is equipped with appropriate fittings, such as bends, valves, and in-line mixers, to ensure smooth material transport. The machine's control system monitors the pressure and flow rates, adjusting the air supply to maintain consistent conveying performance. This integrated approach ensures that the dust is collected while the material is efficiently transported, reducing the need for separate filtration and conveying equipment.
Key Features and Advantages of the Pulse Jet Dust Collector Pneumatic Conveying Machine
Several key features distinguish the pulse jet dust collector pneumatic conveying machine from traditional systems, making it an attractive choice for industrial applications. One of the primary advantages is its high filtration efficiency, which can reach up to 99.9% for particulate matter, ensuring compliance with stringent air quality regulations. The pulse jet cleaning mechanism minimizes downtime for filter maintenance, as the cleaning cycles are automated and can be scheduled based on pressure drop or time intervals.
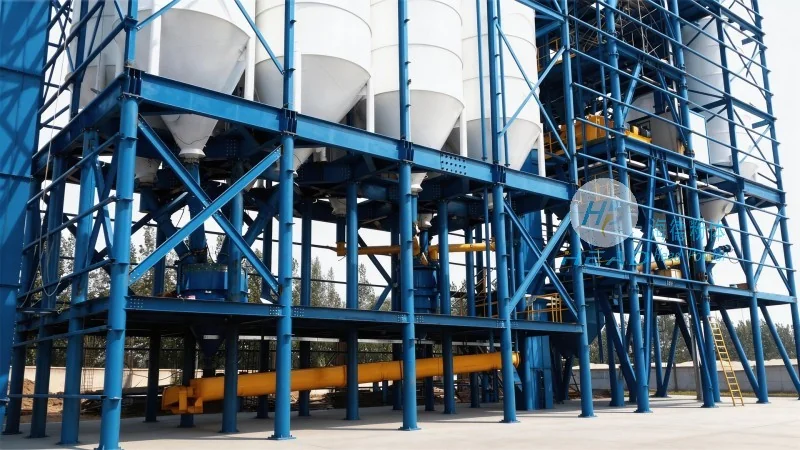
Another notable feature is the energy efficiency of the system. By using compressed air only when necessary and optimizing the pulse timing, the machine reduces energy consumption compared to continuous air cleaning systems. This not only lowers operational costs but also contributes to a more sustainable operation. The machine's compact design allows for easy installation in existing facilities, with minimal space requirements, making it suitable for retrofitting into older plants.
The pneumatic conveying capability of the machine offers flexibility in material transport. It can handle a wide range of materials, including powders, granules, and bulk solids, with varying moisture content and particle sizes. The conveying system can be configured to operate in both positive and negative pressure modes, depending on the application requirements. This adaptability makes the machine suitable for diverse industrial processes, from chemical processing to food production.
Additionally, the machine is designed for durability and reliability. High-quality materials are used in the construction of the dust collector and conveying components, ensuring long service life and minimal maintenance. The control system is user-friendly, with intuitive interfaces that allow operators to monitor and adjust the machine's performance. This ease of operation reduces the training requirements for personnel and enhances overall productivity.
About Shandong HeadPowder Engineering Co., Ltd.
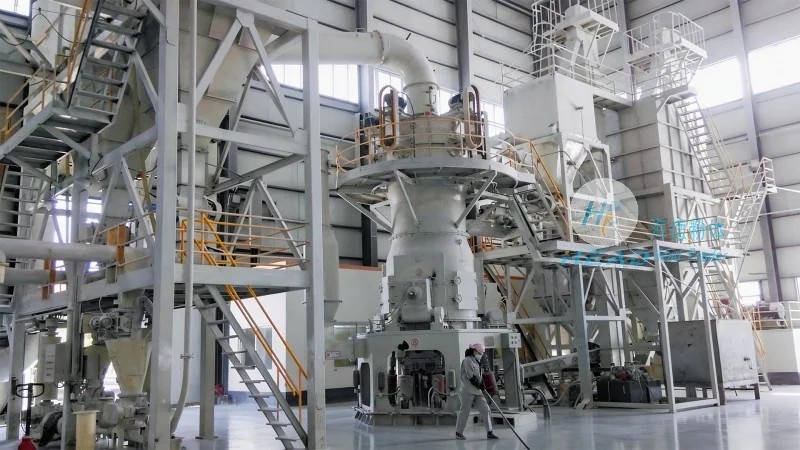
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of industrial equipment, specializes in the design, manufacturing, and supply of pulse jet dust collector pneumatic conveying machines. The company is headquartered in Shandong, China, and has a strong commitment to providing high-quality, reliable equipment that meets the needs of various industrial sectors. With years of experience in the industry, HeadPowder has developed a reputation for innovation and customer satisfaction, offering tailored solutions to meet specific application requirements.
The company's products are engineered to deliver optimal performance and durability, ensuring that customers receive a reliable solution for their material handling and air filtration needs. By combining advanced technology with rigorous quality control, HeadPowder has established itself as a trusted partner for industries seeking efficient and sustainable solutions. The company's team of experts provides technical support and after-sales service to ensure that customers can maximize the benefits of their equipment.




