For industrial applications involving the transport of sintered ash powder, understanding the working principle and key features of pneumatic conveying systems is crucial. This article provides an in-depth look at how such systems operate and the advantages they offer, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field.
Introduction to Sintered Ash Powder Pneumatic Conveying
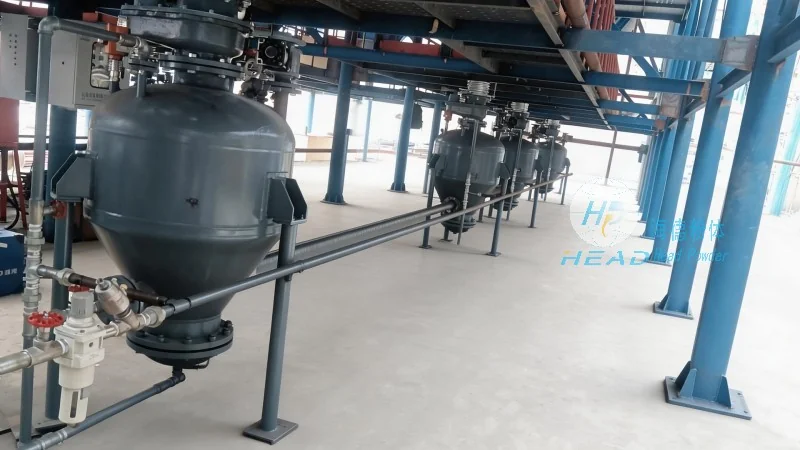
Sintered ash powder, often generated as a byproduct in industrial processes like power generation or metallurgy, requires efficient and reliable transport methods to move it from one location to another. Pneumatic conveying systems have emerged as a preferred solution due to their ability to handle fine powders without the need for mechanical components that might cause contamination or wear. The systems utilize air pressure to move the material through pipelines, offering a clean and flexible method of material handling.
Working Principle of Pneumatic Conveying Systems
The core of a sintered ash powder pneumatic conveying system lies in its ability to generate and control airflow to transport the powder. The process typically involves several key components and steps. First, the sintered ash powder is fed into a hopper or feeder, where it is then introduced into a pipeline. Simultaneously, a fan or blower creates a high-pressure air stream within the system. This air stream carries the powder particles through the pipeline, ensuring they are transported to the destination point, such as a storage silo or processing unit.
There are two main types of pneumatic conveying systems: positive pressure and negative pressure. Positive pressure systems, also known as pressure conveying, operate by blowing air into the pipeline, pushing the powder forward. Negative pressure systems, or vacuum conveying, create a vacuum in the pipeline, drawing the powder into the system. For sintered ash powder, positive pressure systems are often preferred as they can handle larger quantities and longer distances more effectively, though the choice depends on the specific application requirements.
Key Features and Advantages
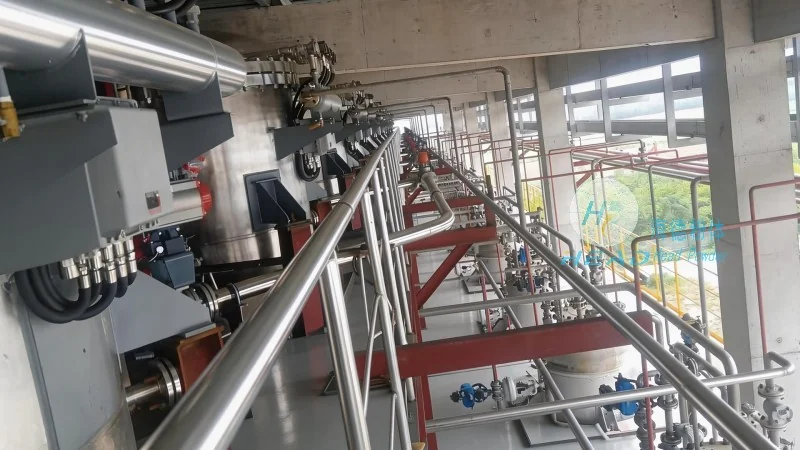
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the unique needs of sintered ash powder handling. The systems offered by the company are characterized by several key features that enhance performance and reliability. One of the primary advantages is the ability to maintain a clean and dust-free environment, as the material is contained within the pipeline and not exposed to the external air. This reduces the risk of contamination and improves safety in industrial settings.
Another significant feature is the flexibility in system design. The systems can be configured to handle varying flow rates and distances, making them suitable for a wide range of industrial applications. The use of high-quality materials, such as stainless steel for the pipelines and components, ensures durability and resistance to corrosion, which is essential when dealing with sintered ash powder that may contain acidic or abrasive components.
The systems also offer energy efficiency and reduced maintenance costs. By eliminating the need for mechanical components like belts or chains, the risk of wear and tear is minimized, leading to lower operational costs over time. Additionally, the compact design of the systems allows for easy integration into existing industrial facilities, without requiring extensive modifications or space.
Application Examples and Industry Impact
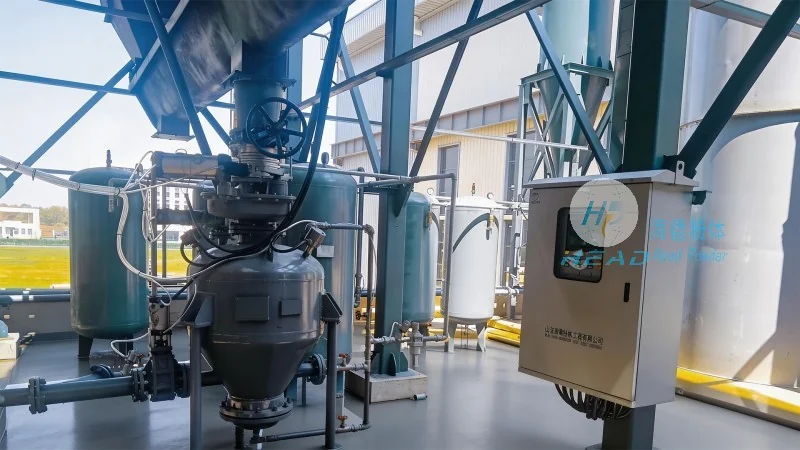
The effectiveness of sintered ash powder pneumatic conveying systems is demonstrated in various industrial applications. For instance, in power plants, these systems are used to transport fly ash from the boiler to storage or disposal areas, ensuring efficient material handling and compliance with environmental regulations. In metallurgical plants, the systems help in moving sintered ash from processing units to recycling or disposal sites, contributing to overall operational efficiency.
By leveraging the expertise of Shandong HeadPowder Engineering Co., Ltd., industries can benefit from optimized material handling solutions that enhance productivity, reduce costs, and improve safety. The company’s commitment to quality and customization ensures that each system is tailored to meet the specific requirements of the client, providing a reliable and efficient solution for sintered ash powder transport.
Conclusion
In summary, sintered ash powder pneumatic conveying systems operate on the principle of using air pressure to transport fine powders through pipelines, offering a clean, flexible, and efficient method of material handling. The key features, including environmental cleanliness, durability, energy efficiency, and customization, make these systems ideal for various industrial applications. With the support of companies like Shandong HeadPowder Engineering Co., Ltd., industries can achieve optimal performance and reliability in their material transport processes, contributing to overall operational success.




