For industries dealing with glucose, selecting the right material handling system is crucial. The need for efficiency, hygiene, and reliability cannot be overstated. Among the various options available, pneumatic conveying technology stands out as a superior choice for transporting glucose with minimal contamination and maximum operational efficiency. This article delves into the benefits and applications of pneumatic conveying in glucose handling, highlighting why it is considered the cleanest and most effective method for this purpose.
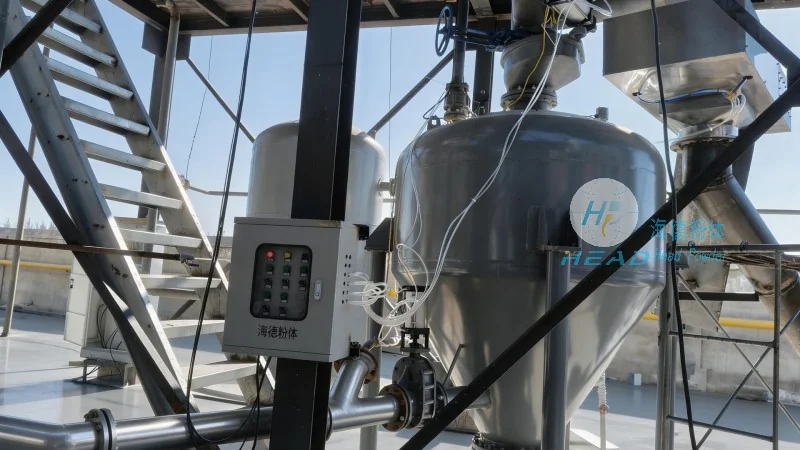
Pneumatic Conveying: How It Works and Its Advantages
Pneumatic conveying systems use air or other gases to transport bulk materials like glucose through a pipeline. Unlike traditional mechanical systems that involve moving parts and potential points of contamination, pneumatic conveying operates with a closed system, ensuring that the material remains in a controlled environment. This design significantly reduces the risk of cross-contamination, making it ideal for pharmaceutical and food industries where product purity is paramount. The technology offers several key advantages:
- High Efficiency and Speed: Pneumatic conveyors can transport glucose at high velocities, reducing overall processing time. This is particularly beneficial in large-scale production where quick and consistent material movement is required.
- Clean and Hygienic Operation: The enclosed pipeline system prevents dust and airborne particles from entering the product stream. This is critical for maintaining the quality and safety of glucose, which is often used in sensitive applications such as pharmaceuticals or food products.
- Reduced Downtime and Maintenance: With fewer moving parts compared to mechanical conveyors, pneumatic systems experience less wear and tear, leading to lower maintenance costs and longer operational life.
- Flexibility in Layout: Pneumatic conveying allows for flexible pipeline configurations, enabling the system to be adapted to different plant layouts without major structural changes.
Application of Pneumatic Conveying in Glucose Handling
Glucose, a common sweetener and raw material in various industries, requires a transport method that preserves its quality and purity. Pneumatic conveying excels in this regard by providing a seamless, continuous flow of material. Whether it's moving raw glucose from storage to processing units or transporting finished products to packaging lines, pneumatic systems ensure that the material remains in a controlled state throughout the process.
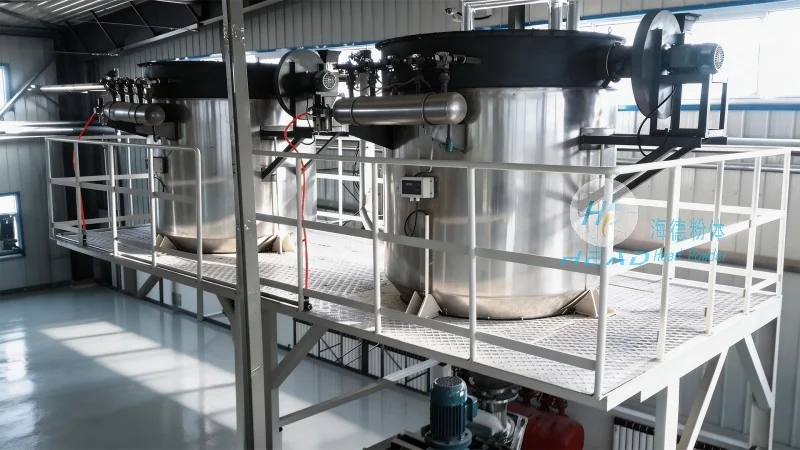
For example, in a pharmaceutical facility, the use of pneumatic conveying for glucose can prevent contamination from external sources, ensuring that the final product meets stringent regulatory standards. Similarly, in food processing plants, the hygienic design of pneumatic systems helps maintain the quality of glucose used in beverages, baked goods, and other food products.
HeadPowder Engineering: Leading the Way in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a prominent player in the material handling industry, specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the needs of glucose and other bulk materials. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for businesses seeking efficient and clean transport solutions.
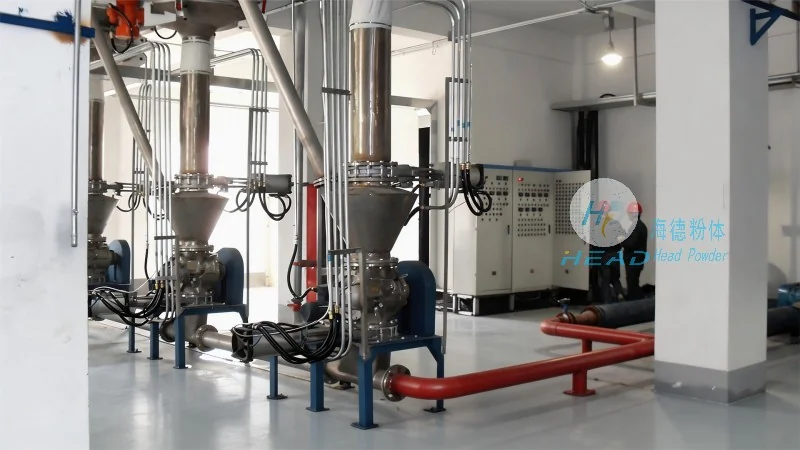
HeadPowder's expertise lies in customizing pneumatic conveying systems to meet specific operational requirements. The company's team of engineers works closely with clients to understand their production processes, material characteristics, and quality standards, ensuring that the final solution is optimized for performance and reliability. By leveraging cutting-edge technology and rigorous quality control measures, HeadPowder delivers systems that enhance productivity while maintaining the highest levels of hygiene.
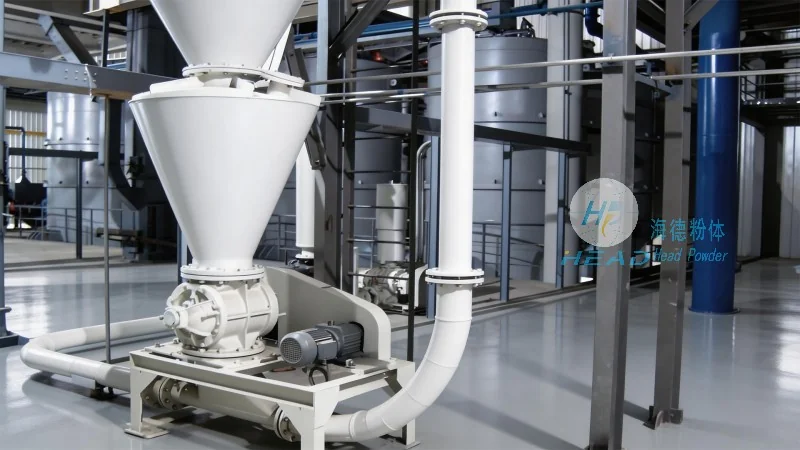
Key Features of HeadPowder's Pneumatic Conveying Systems
HeadPowder's pneumatic conveying systems are equipped with several features that make them ideal for glucose transport:
- High-Purity Materials: Components such as pipelines, valves, and fittings are made from materials that are resistant to corrosion and compatible with glucose, ensuring that the product remains uncontaminated.
- Advanced Control Systems: The systems are integrated with sophisticated control panels that allow for real-time monitoring and adjustment of conveying parameters, ensuring optimal performance.
- Energy Efficiency: By optimizing air flow and pressure, HeadPowder's systems minimize energy consumption, reducing operational costs for the client.
- Easy Cleaning and Maintenance: The design of the systems facilitates regular cleaning and maintenance, ensuring that the equipment remains in top condition and operational for extended periods.
Conclusion: The Future of Glucose Transport with Pneumatic Conveying
As the demand for efficient and clean material handling solutions continues to grow, pneumatic conveying technology remains at the forefront of innovation. For glucose transport, this technology offers a superior alternative to traditional methods, providing unmatched efficiency, hygiene, and reliability. With companies like Shandong HeadPowder Engineering Co., Ltd. leading the way in developing advanced pneumatic systems, the future of glucose handling looks promising. By investing in pneumatic conveying, businesses can enhance their operational efficiency, maintain product quality, and stay ahead in a competitive market.




