Efficient and reliable material handling is crucial in the cocoa processing industry, particularly when dealing with delicate and high-value products like cocoa powder. The proper handling of cocoa powder not only ensures product quality and safety but also enhances operational efficiency. This article explores the working principles and key features of modern cocoa powder material handling systems, highlighting how advanced technologies are applied to meet the demands of the industry.
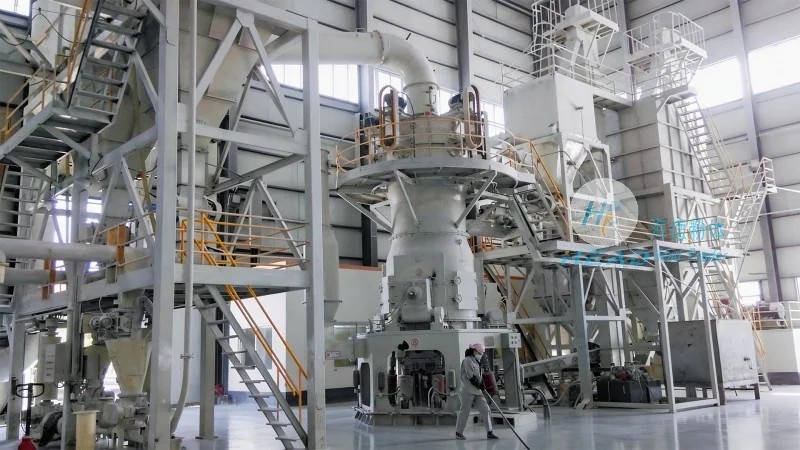
Understanding the Working Principle of Cocoa Powder Material Handling
The working principle of cocoa powder material handling typically involves the use of specialized equipment designed to transport, store, and distribute cocoa powder with minimal risk of contamination or degradation. Common methods include mechanical conveying systems, such as screw conveyors and belt conveyors, as well as pneumatic systems that utilize air pressure to move the powder through pipelines. These systems are engineered to maintain the integrity of the cocoa powder, preserving its flavor, aroma, and nutritional properties throughout the handling process.
For instance, a screw conveyor operates by rotating a helical screw within a trough, which moves the cocoa powder forward through the system. This method is particularly effective for handling free-flowing powders like cocoa powder, as it provides gentle and continuous movement without causing excessive friction or breakage. The design of the screw conveyor, including the pitch and diameter of the screw, is optimized to control the speed and pressure of the material flow, ensuring smooth and efficient transport. In contrast, pneumatic conveying systems use compressed air to create a flow of air and powder mixture, which is then directed through a network of pipes to the desired destination. This method is ideal for long-distance or high-rise applications, as it can transport cocoa powder over significant distances without the need for multiple transfer points.
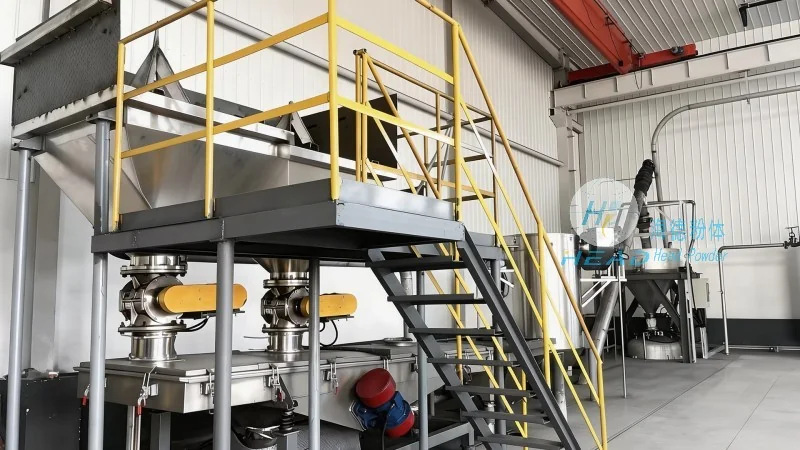
Key Features of Cocoa Powder Material Handling Systems
Modern cocoa powder material handling systems are characterized by several key features that enhance their performance and suitability for the industry. One of the most important features is the emphasis on hygiene and sanitation. Since cocoa powder is a food product, all handling equipment must comply with strict regulatory standards, such as those set by the FDA or EU food safety guidelines. This includes the use of stainless steel construction, smooth surfaces, and easy-to-clean components to prevent the accumulation of powder residues and microbial growth. Additionally, many systems incorporate dust control measures, such as sealed enclosures and filtration systems, to minimize the release of airborne particles and maintain a clean working environment.
Another critical feature is the ability to handle varying particle sizes and moisture content. Cocoa powder can have a wide range of particle sizes, from fine to coarse, and may contain moisture that affects its flow properties. Advanced material handling systems are equipped with adjustable components, such as variable-speed drives and adjustable screw pitch, to accommodate these variations. This ensures consistent and reliable operation, even when dealing with different batches of cocoa powder. Furthermore, the systems often include monitoring and control features, such as level sensors and flow meters, which allow operators to track the amount of material in storage and the rate of transport in real time. This data is essential for optimizing production processes and preventing overfilling or underfilling of storage tanks.
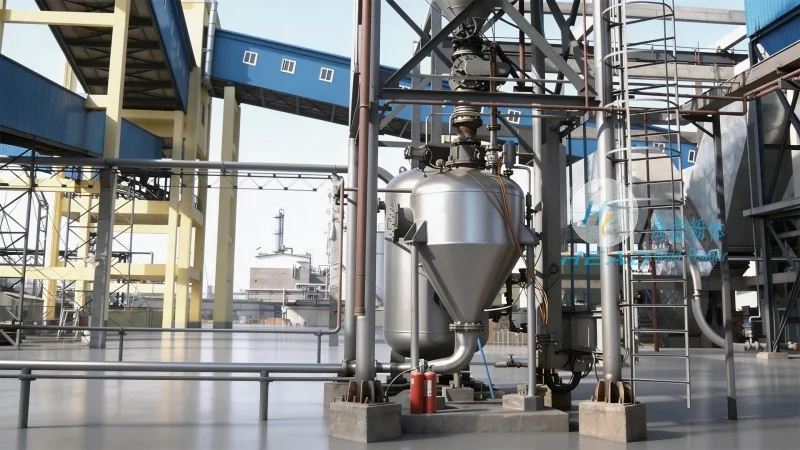
Efficiency and Cost-Effectiveness in Cocoa Powder Handling
Efficiency and cost-effectiveness are paramount in the cocoa powder handling process. The use of modern material handling systems can significantly reduce labor costs and improve overall productivity. For example, automated conveying systems can operate continuously without the need for manual intervention, reducing the risk of human error and increasing the throughput of the production line. Additionally, the reduction in material loss and waste due to improved handling techniques can lead to substantial cost savings over time. Companies like Shandong HeadPowder Engineering Co., Ltd. specialize in designing and manufacturing customized material handling solutions tailored to the specific needs of cocoa processing facilities. With years of experience in the industry, HeadPowder provides comprehensive services, including system design, installation, and maintenance, to ensure that clients achieve optimal performance and reliability.
Conclusion
In conclusion, the working principle and features of cocoa powder material handling systems play a vital role in maintaining product quality and operational efficiency in the cocoa industry. By leveraging advanced technologies and adhering to strict hygiene standards, modern systems can effectively transport and store cocoa powder while preserving its valuable properties. Companies like Shandong HeadPowder Engineering Co., Ltd. continue to innovate and provide tailored solutions to meet the evolving demands of the cocoa processing sector, ensuring that businesses can operate at their best with reliable and efficient material handling equipment.




