Efficient and reliable sintered ash material conveying systems are crucial in industrial processes, particularly in the iron and steel industry where the handling of sintered ash is a common requirement. Understanding the working principle and key characteristics of such systems is essential for optimizing material transport and ensuring operational efficiency. This article provides an in-depth exploration of the mechanisms behind sintered ash material conveying, highlighting the technical aspects and functional features that define modern solutions.
Working Principle of Sintered Ash Material Conveying
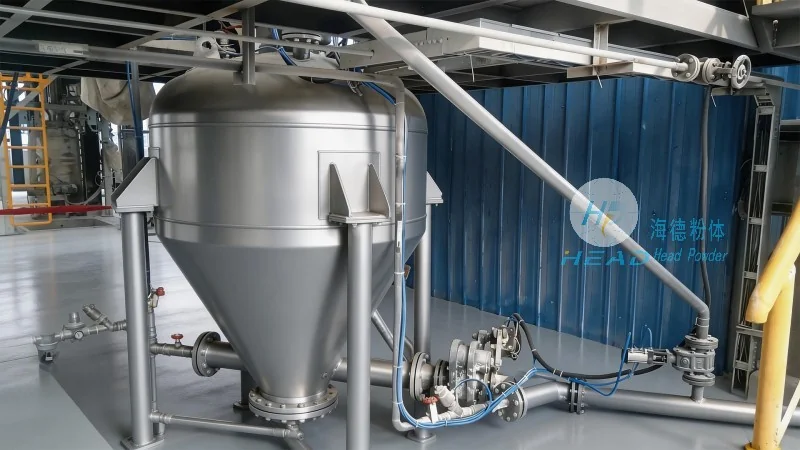
The working principle of sintered ash material conveying typically involves a combination of mechanical components designed to transport bulk materials over varying distances. A common approach is the use of belt conveyors, which are widely adopted due to their adaptability and efficiency in handling sintered ash. The process begins with the loading of sintered ash onto the conveyor belt at the feed point. The belt, driven by a motor and pulley system, moves the material forward. The sintered ash, which may have varying particle sizes and moisture content, is transported through the system with minimal spillage and loss. The conveyor system may include idlers to support the belt and maintain proper tension, ensuring smooth operation. Additionally, some systems incorporate control mechanisms to regulate the speed and direction of the conveyor, allowing for precise material handling. The discharge point is where the sintered ash is released, often into a storage bin or processing unit. The entire process is powered by electric motors, which provide the necessary force to move the material through the conveying system. The design of the conveyor, including the belt type, pulley configuration, and support structure, is tailored to the specific characteristics of the sintered ash, such as its density, abrasiveness, and flowability.
Key Characteristics of Sintered Ash Material Conveying Systems
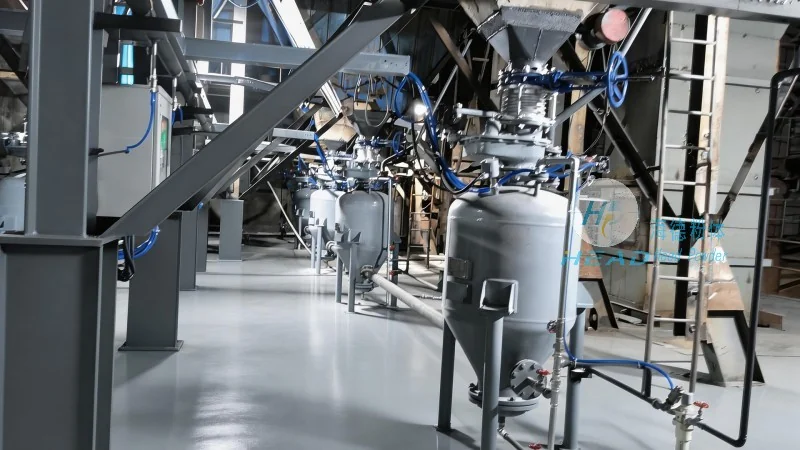
Several key characteristics define the performance and effectiveness of sintered ash material conveying systems. First, the system's ability to handle abrasive materials is critical, as sintered ash can be hard and rough, potentially causing wear on conveyor components. High-quality materials, such as rubber or special steel, are used for the conveyor belt and pulleys to withstand the abrasive nature of the ash. Second, the system must maintain a consistent flow rate to prevent blockages or overloading. This is achieved through proper design of the feed hopper and control of the conveyor speed. Third, the system's durability and reliability are essential for continuous operation in industrial settings. Regular maintenance and robust construction are necessary to ensure long-term performance. Fourth, the system's energy efficiency is a significant consideration, as reducing energy consumption can lower operational costs. Modern conveyor systems often incorporate energy-saving features, such as variable speed drives, to optimize power usage. Fifth, the system's adaptability to different material conditions is important. Sintered ash may vary in moisture content and particle size, requiring the conveyor to be flexible enough to handle these variations without compromising performance. Finally, the system's safety features, including guards and emergency stop mechanisms, are vital to protect operators and prevent accidents during operation.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design and production of material handling equipment, including sintered ash conveying systems. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted provider in the industry. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. HeadPowder's team of engineers and technicians brings extensive experience in material handling systems, ensuring that each product meets the highest standards of performance and reliability. The company adheres to strict quality control processes, from raw material selection to final assembly, to deliver durable and efficient conveying solutions. HeadPowder's commitment to customer satisfaction is reflected in its comprehensive after-sales service, which includes maintenance, repair, and technical support. By leveraging its expertise and advanced manufacturing capabilities, HeadPowder continues to provide reliable sintered ash material conveying systems that meet the diverse needs of industrial clients.
Conclusion
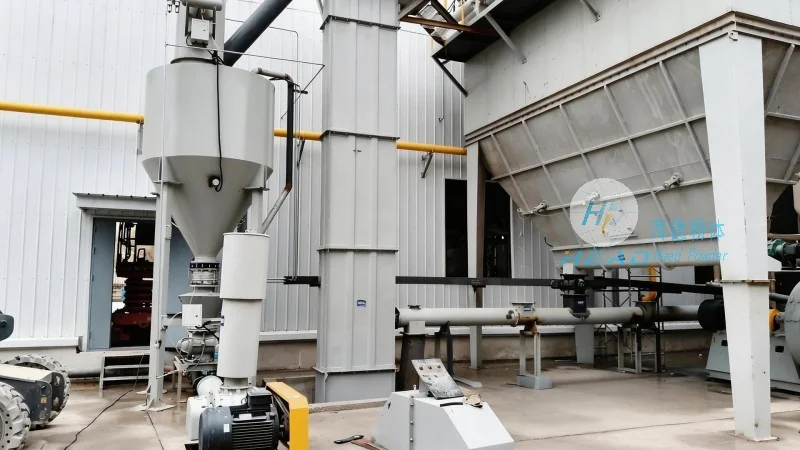
In summary, sintered ash material conveying systems operate on a well-defined working principle that combines mechanical components to efficiently transport bulk materials. The key characteristics of these systems, including durability, adaptability, and energy efficiency, are crucial for their performance in industrial applications. Shandong HeadPowder Engineering Co., Ltd. plays a significant role in the industry by providing high-quality conveying solutions tailored to the specific requirements of sintered ash handling. By understanding the working principle and characteristics of such systems, industrial operators can make informed decisions to enhance their material handling processes and improve overall operational efficiency.




